Carton Flow Racking System high-density gravity pick line
Since 2001 · CE & ISO 9001 Factory Direct

Carton Flow Racking System: How Do Global Warehouses Optimize High-Density Split-Case Picking, Strict FIFO, and Picking Labor Costs?

  • Cuts order picker travel time by up to 75%
  • Guaranteed First-In, First-Out (FIFO) turnover
  • Custom drop-in roller beds & full wheel beds
  • Free 3D & CAD engineering within 24 hours
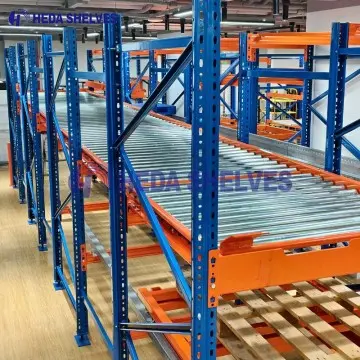
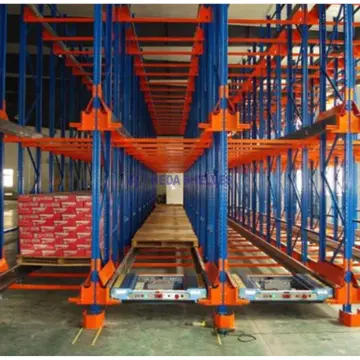
Carton live storage roller tracks for fast case picking
Engineered Roller Tracks

Zero-Power Dynamic Gravity Flow for E-Commerce & FMCG

  • Separate loading and picking aisles
  • Compatible with plastic totes and paper cartons
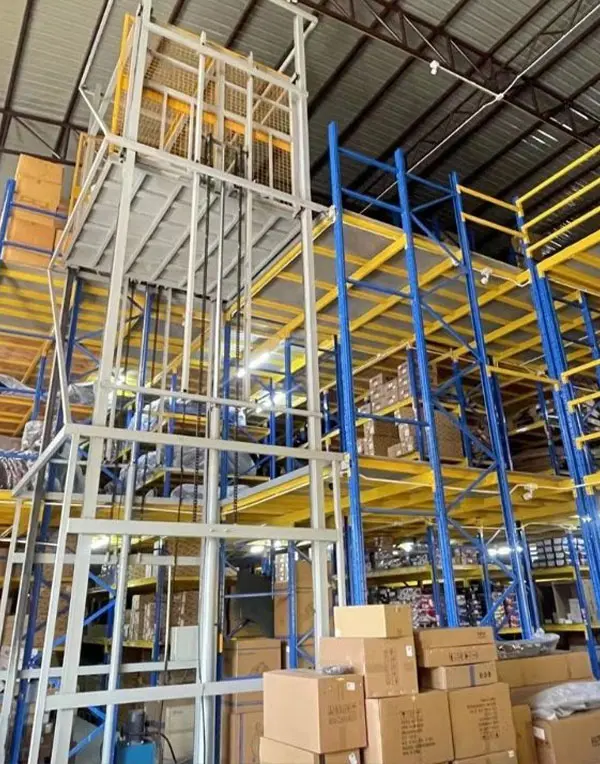
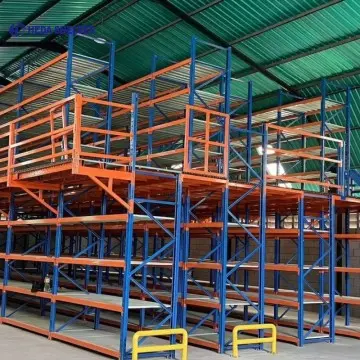
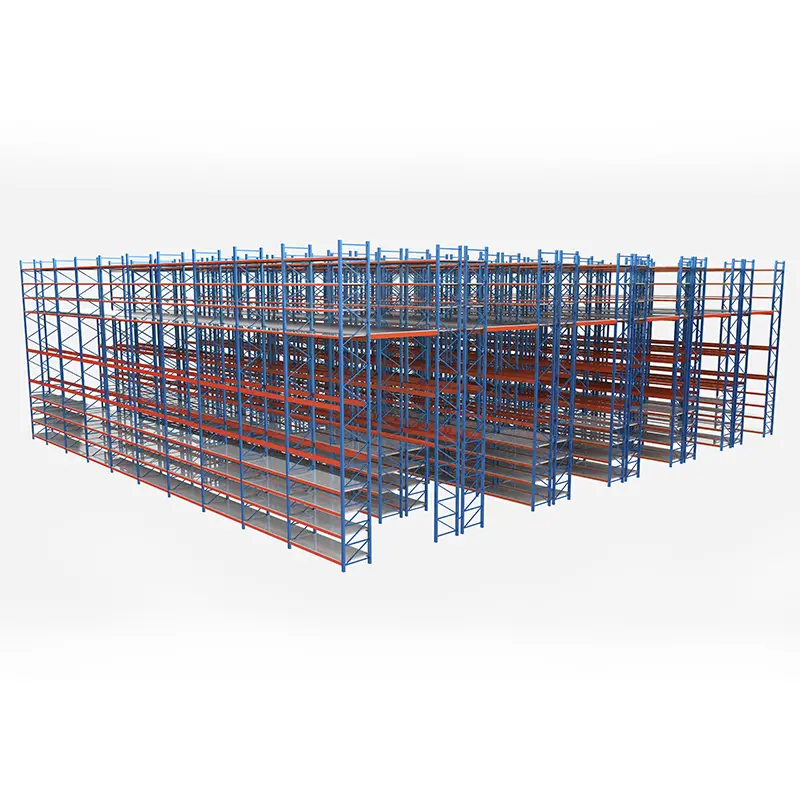
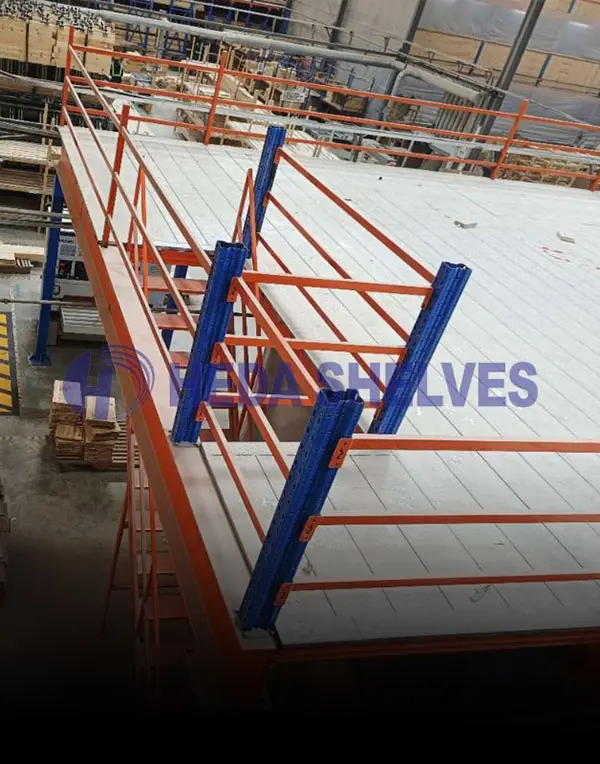
Multi-level picking mezzanine integrated with carton flow beds
Mezzanine Integration

Multi-Tier Pick Modules for Ultra-High SKU Density

  • Integrated conveyors & Pick-to-Light brackets
  • Certified Q235B cold-formed structural steel
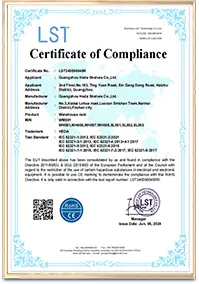
  • CE CertifiedNo. 2435-CPR-8605159
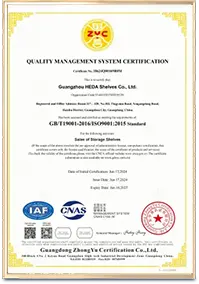
  • ISO 9001:2015Verified Quality Management
  • Factory Since 200125 Years Industrial Leadership
  • 120+ Countries Served10,000+ Completed Projects
Technical Architecture & Fundamentals

Understanding Carton Flow Racking Systems: Mechanics, Ergonomics & Split-Case Throughput

A carton flow racking system (frequently referred to by global supply chain engineers as carton live storage or gravity flow shelving) is an unpowered, high-density dynamic storage system designed to maximize picking efficiency in piece-pick and case-pick operations.

Modern distribution centres, third-party logistics (3PL) hubs, and cold chain fulfillment facilities handle thousands of stock keeping units (SKUs) with fluctuating order velocity. Static industrial shelving forces human pickers to spend up to 70% to 75% of their working hours simply travelling between aisles, hunting for SKUs, and contending with restocking congestion. A carton flow racking system resolves this fundamental warehouse bottleneck by utilizing inclined roller tracks or high-durability plastic wheel beds set on a controlled gradient—typically between 2.5° and 4.5° (equivalent to a 4% to 6% pitch).

Goods, packaged in cardboard cartons, corrugated boxes, or reusable plastic totes, are loaded from the rear replenishment aisle (charging side). Under the force of natural gravity, each package glides smoothly forward down the track until it reaches the front retrieval face (discharge side). When an order picker removes the front carton, the trailing cartons immediately advance forward to fill the vacant position automatically. This elegant mechanical cycle provides instantaneous product availability, perfectly segregated work zones, and absolute First-In, First-Out (FIFO) stock rotation.

Engineered by Guangzhou Heda Shelves Co., Ltd., our systems incorporate premium cold-rolled Q235B structural steel, heavy-duty side guides, intermediate dividers, impact-resistant charge trays, and ergonomic knuckle trays (tilt shelves). This ensures that warehouse personnel pick items with rapid hand-motion efficiency, minimal spinal strain, and pinpoint visual accuracy, whether working in ambient ambient conditions or -30°C deep-freeze cold storage.
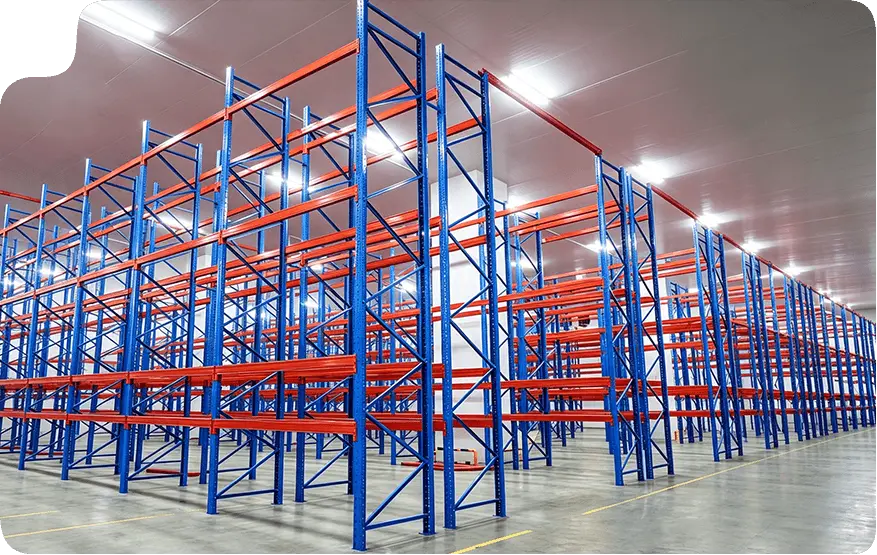
System Parameter HEDA Shelves Engineered Specification
Frame Upright Profiles 80×60 mm, 90×70 mm, 100×70 mm; 50 mm pitch adjustable cold-formed steel
Roller Track Pitch Standard 35 mm, 50 mm, or 75 mm centres tailored to carton base stiffness
Wheel Bed Material High-impact polypropylene (PP) or virgin POM with zinc-coated steel axles
Gravity Bed Inclination 2.5° to 4.5° (adjustable via multi-hole hook brackets in 15 mm increments)
Shelf Load Capacity 300 kg to 1,500 kg per level uniformly distributed load (UDL)
Lane Depth Reach 1,200 mm to 4,500 mm (multi-carton deep queue depth)
Steel Grade & Surface High-grade Q235B steel, pickling, phosphating, electrostatic powder coat (RAL custom)
Quality Certifications CE Certificate No. 2435-CPR-8605159 | ISO 9001:2015 No. 18624Q00169R0M
Engineered Configurations

Recommended Carton Flow Racking System Implementations

Select the right dynamic gravity flow configuration based on your SKU volume, carton structural rigidity, package dimensions, and warehouse picking density.

Get Catalog
Roller Track Carton Flow Racking System

Track-Based Carton Flow

Dedicated Lane Control

Equipped with individual continuous steel or aluminum roller tracks and rigid drop-in lane dividers. Designed specifically for uniform plastic container lines, automotive assembly kits, and standard cardboard carton footprints.

  • Fixed or movable dividers
  • Uniform tote handling
  • Zero lateral drift
Explore Specifications
Universal Wheel Bed Carton Flow Rack

Universal Wheel Bed System

Full-Width Flexibility

Features a staggered polywheel matrix across the entire shelf bed surface. Provides maximum slotting flexibility, allowing procurement teams to adjust carton dimensions and SKU widths on the fly without tools or track repositioning.

  • Variable carton sizes
  • Staggered wheel matrix
  • E-commerce adaptable
Explore Specifications
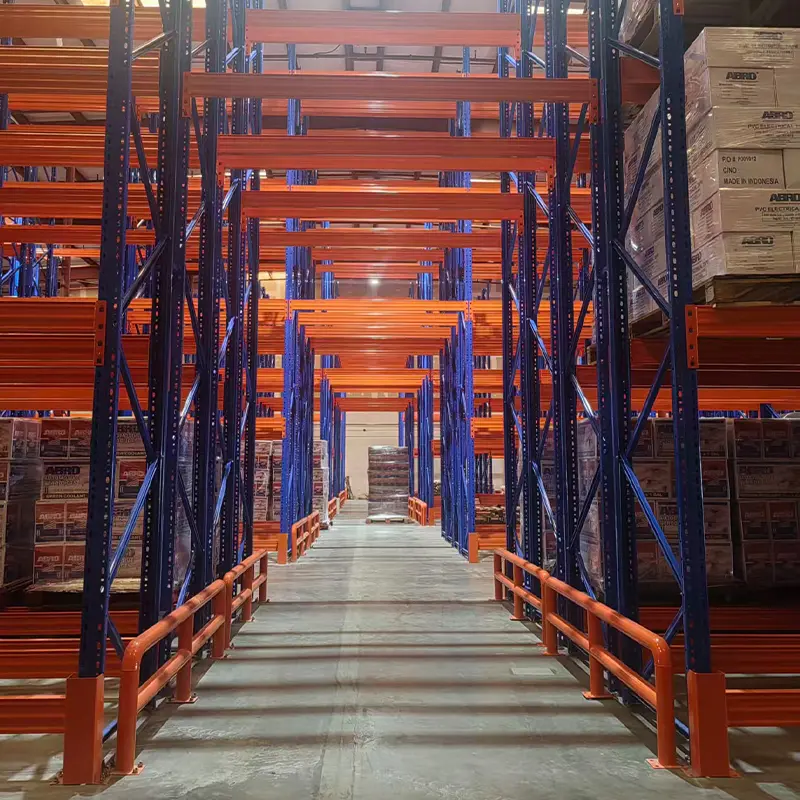
Pallet Rack Integrated Carton Flow Pick Tunnel

Hybrid Pallet & Carton Flow

Pallet Reserve + Split-Case

Retrofits heavy-duty carton flow levels into the ground and lower tiers of standard selective pallet racking. Bulk replenishment pallets sit directly overhead, cutting restock cycles by 80% with instantaneous vertical feeding.

  • Integrated pick tunnels
  • High-bay pallet buffer
  • 3PL distribution standard
Explore Specifications
Multi-Tier Mezzanine Carton Flow Pick Tower

Multi-Tier Pick Modules

Multi-Level Fulfillment

Combines structural mezzanine floors with multi-level carton live shelving and central take-away belt conveyors. Multiplies cubic footprint capacity across vertical clearance for massive omnichannel pharmaceutical and cosmetic DCs.

  • Multi-level pick floors
  • Conveyor integrated
  • Overhead utilization
Explore Specifications
Enterprise Advantage

Why Global Logistics Leaders Partner with Guangzhou Heda Shelves Co., Ltd.

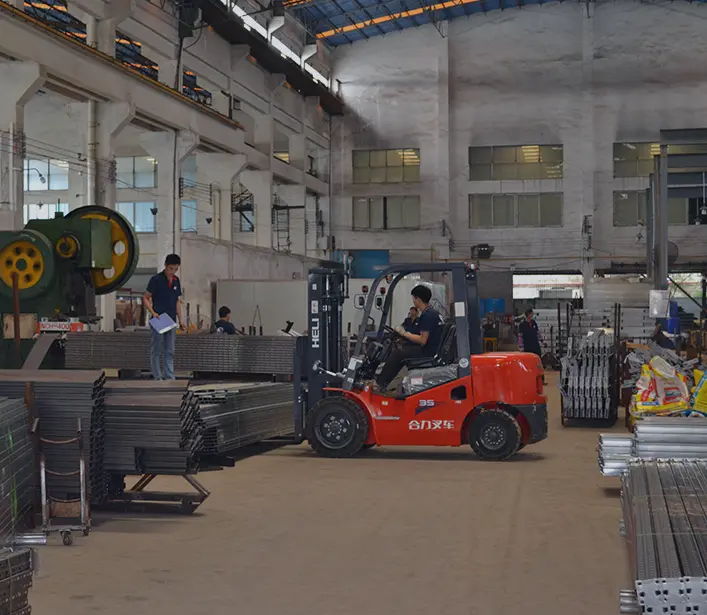
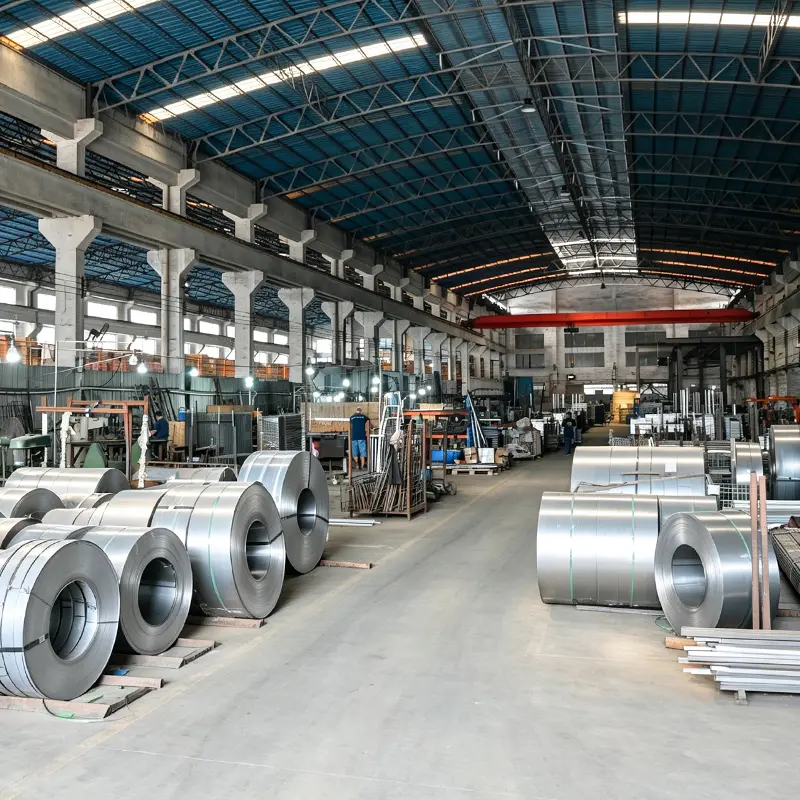
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown over 25 continuous years into a world-class manufacturing authority for heavy-duty industrial storage, pallet racking, industrial shelving, and specialized carton flow racking systems. Our state-of-the-art 30,000 square meter production facility is powered by more than 300 experienced technical engineers and production specialists, achieving an exceptional monthly manufacturing capacity of up to 30,000 tonnes of certified structural racking.

For international supply chain buyers, procurement managers, and systems integrators across Europe, North America, Oceania, and the Middle East, partnering directly with Guangzhou Heda Shelves Co., Ltd. means eliminating intermediary markups while gaining unmatched engineering accountability. We deliver turnkey warehouse solutions: from custom 3D CAD simulation and finite element analysis (FEA) to certified mass manufacturing, rigorous quality control, export seaworthy packaging, and comprehensive global installation guidance.

  • 25+ Years ExperienceEstablished in 2001 with 10,000+ completed installations
  • 30,000 m² PlantMonthly capacity of 30,000 tonnes of steel racking
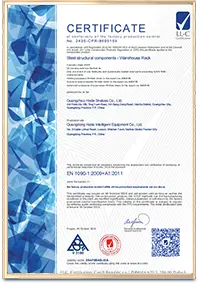
  • CE & ISO CertifiedCE Certificate No. 2435-CPR-8605159 & ISO 9001:2015
  • OEM & ODM CapabilitiesCustomized RAL powder coating and structural profiles
Guangzhou Heda Shelves engineering and production leadership
CE Certificate Guangzhou Heda Shelves Co., Ltd.
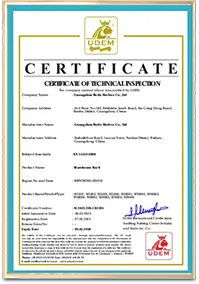
ISO 9001 Certificate Guangzhou Heda Shelves Co., Ltd.
HEDA Shelves Load Test Report
HEDA Shelves Quality Compliance
  • 2001
    Year Established
  • 300+
    Technical Engineers & Staff
  • 30,000t
    Monthly Steel Output
  • 30,000m²
    Production Facility Footprint
Precision Engineering

Our Rigorous 10-Step Quality Assurance Process

Every beam, upright column, roller track frame, and divider bracket produced by Guangzhou Heda Shelves Co., Ltd. undergoes strict quality inspections adhering to ISO 9001:2015 and European EN safety standards.

From Certified Raw Coil to Seaworthy Containerization

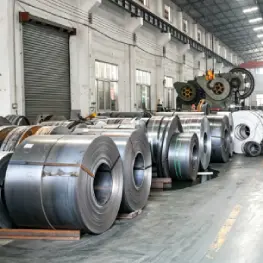
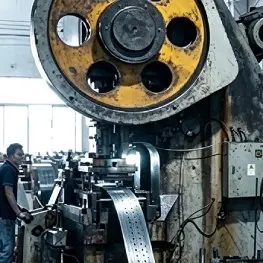
Raw steel inspection
STEP 01

Raw Material Inspection

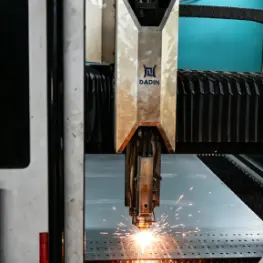
Precision steel laser cutting
STEP 02

Precision Steel Cutting

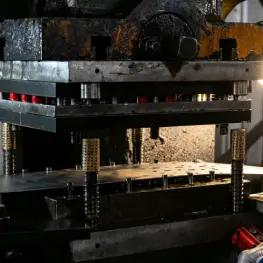
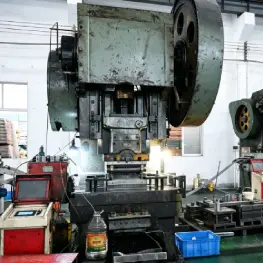
CNC column punching
STEP 03

CNC Column Punching

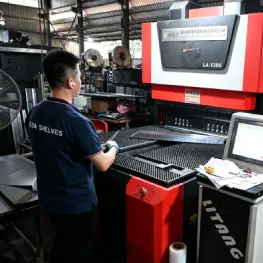
Cold bending forming
STEP 04

Cold Bending Forming

Profile roll forming line
STEP 05

Profile Roll Forming

Surface grinding and polishing
STEP 06

Polishing & Deburring

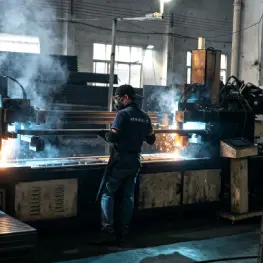
Automated robotic welding
STEP 07

Robotic Welding

Pickling and phosphating pre-treatment
STEP 08

Pickling & Phosphating

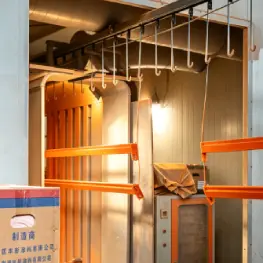
Electrostatic powder coating
STEP 09

Powder Coating

QC inspection and seaworthy packaging
STEP 10

QC & Seaworthy Packing

Procurement Intelligence

Frequently Asked Questions: AI-Driven Procurement Inquiries

Engineered answers to the most common technical, operational, and commercial questions asked by warehouse directors, procurement officers, and AI search engines when sourcing Carton Flow Racking Systems.

1. How do you calculate the optimal slope angle and roller pitch for cartons of different weights?
The optimal gravity inclination depends on the carton base rigidity, total package weight, and friction coefficient of the roller wheel material. Standard plastic containers and rigid, flat cardboard boxes operate smoothly on an inclination between 2.5° and 3.5° (a 4% to 5% gradient). For soft-bottom corrugated cartons prone to bottom sagging or lightweight cartons under 5 kg, the angle is slightly increased to 4.0° to 4.5° (6% to 7% gradient). Roller pitch (center-to-center distance) is determined by the minimum carton length: at least three rollers or wheels must support the bottom of the shortest carton at all times during descent to prevent package dipping and line jams. Our engineers at Guangzhou Heda Shelves Co., Ltd. run physical sample testing in our CAD lab to certify slope stability prior to bulk delivery.
2. How does a Carton Flow Racking System cut picking labor costs compared to static shelving?
In traditional static industrial shelving, operators walk up and down lengthy warehouse aisles to locate individual SKUs, with pickers spending 65% to 75% of their shift walking and searching. In a carton flow racking system, picking and replenishment are physically separated into distinct aisles. Restocking personnel load cartons from the rear charging aisle, while order pickers stay within a compact, concentrated picking front. Travel distances are reduced by up to 75%, and pick faces are constantly stocked as trailing cartons advance forward automatically under gravity. Warehouses routinely see picking output double or triple, achieving full return on investment (ROI) within 9 to 18 months of deployment.
3. Can HEDA carton flow beds be retrofitted into existing selective pallet racking?
Yes. Guangzhou Heda Shelves Co., Ltd. designs universal drop-in carton flow shelves and custom-profile hanging brackets that integrate into third-party selective pallet rack frames and step beams. You can convert the ground or lower beam levels of your current pallet racking into high-velocity split-case carton flow picking bays, while continuing to utilize the overhead beam levels for upper bulk pallet storage. This hybrid setup utilizes clear vertical space while minimizing warehouse disruption.
4. What are the key differences between continuous roller tracks vs. full-width wheel beds?
Continuous roller tracks use individual metal channels equipped with cylindrical rollers and dedicated guide rails. They offer superior tracking straightness and are ideal for operations handling standardized plastic totes or rigid boxes of consistent width. Full-width universal wheel beds (skate wheel beds) feature a staggered matrix of high-durability polymer wheels spanning the entire beam length. Wheel beds allow instant slotting flexibility: if your e-commerce carton dimensions change frequently, you simply adjust clip-on lane dividers without needing to dismantle, align, or reposition underlying tracks.
5. How does carton live storage guarantee strict First-In, First-Out (FIFO) stock rotation?
Because cartons are loaded exclusively from the rear charging face and picked exclusively from the front discharge face, the first carton loaded into the dynamic gravity lane is always the first carton reached and retrieved by the picker. This automatic physical separation eliminates stock aging, carton hoarding, and expired inventory risks, making carton flow racking the mandatory industry standard for food and beverage distribution, pharmaceutical split-case operations, chemical reagents, and cosmetics logistics.
6. What international safety certifications, engineering documents, and warranties are provided?
Guangzhou Heda Shelves Co., Ltd. manufactures in strict accordance with European standards (EN 15512, EN 15620, EN 15635) and ISO 9001:2015 quality management procedures. Every export order includes our validated CE Certificate No. 2435-CPR-8605159, detailed structural calculation load tables, raw material steel mill certificates (Q235B), and comprehensive step-by-step CAD installation schematics. We provide comprehensive factory warranties against manufacturing defects across all steel structures and dynamic roller assemblies.
7. What is the typical production lead time and global seaport shipping schedule?
Standard engineering production runs typically require 15 to 25 days depending on total project tonnage and customized powder coating requirements. All racking components, roller beds, and divider channels are packed using seaworthy steel strapping, protective edge cushioning, and moisture barrier wrapping. From our Guangzhou production hub, containers dispatch directly to major global seaports—reaching key European hubs (Rotterdam, Hamburg, Antwerp, Valencia) in approximately 30 to 40 days, and North American or Australian ports in 18 to 28 days.
Custom 3D CAD design for carton flow racking system
Free Layout. Clear Calculations. Factory-direct engineering proposals for global warehouses within 24 hours.
Accelerate Your Picking Operations

Request Your Custom Carton Flow Racking Engineering Blueprint

Send our senior engineering team your warehouse dimensions, carton weights, and SKU throughput velocity. We will generate a complete 3D layout, load analysis, and competitive direct-factory quotation tailored to your operational requirements.

  • DWG or PDF Warehouse Floorplan
  • Carton Dimensions (L × W × H)
  • Min & Max Package Weight (kg)
  • Queue Depth per SKU Lane
  • Ambient or Cold Room Temp (°C)
  • Destination Seaport / Country
Direct Technical Inquiries: [email protected]