Engineered Warehouse Storage & Flow Rack Systems
Precision-manufactured in our certified Guangzhou industrial facility, our heavy-duty cross beams, gravity rollers, and dynamic storage frameworks integrate seamlessly into international pallet handling networks.
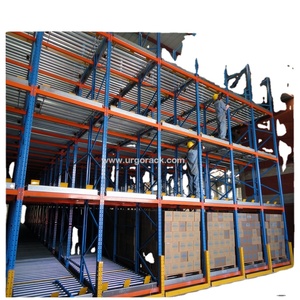
High Efficiency Order Picking Racking System, Gravity Flow Roller Racking System
- First-In, First-Out (FIFO) stock automation
- Heavy-duty integrated cross-tie beams
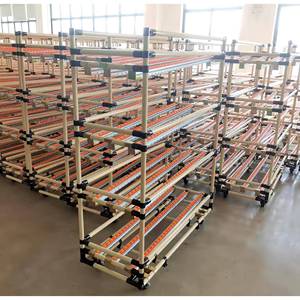
AOCHEN Industrial Collapsible Adjustable Gravity Roller Shelves Steel Flow Rack Shelving System High-Strength
- High-strength modular roller track profile
- 50mm vertical pitch level adjustment
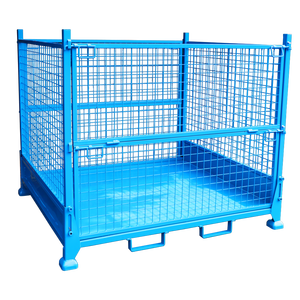
Carter OEM Steel Heavy Duty Collapsible Storage Container Box Stacking Wire Mesh Cage Pallet Foldable Stillage Cage
- Reinforced perimeter base channel welding
- Stacks 4 tiers high on pallet cross beams
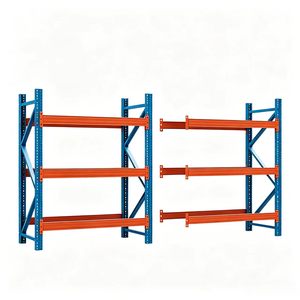
Custom Height Pallet Storage Rack Heavy Load for Industrial Logistics Inventory
- Q355B high-tensile twin-C box beam pairs
- 1,000kg to 4,500kg per level loading
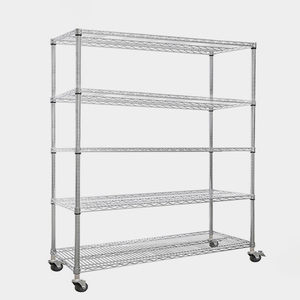
Racks Heavy Duty Metal Steel Storage Shelves 5 Layer Wire Shelf for Sale Racks Shelves
- Step beams with integrated wire mesh deck recess
- Certified NFPA fire-protection water pass-through
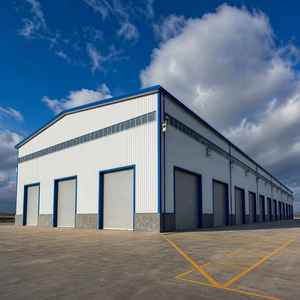
Reach Truck Aisle Steel Warehouse Building Narrow Racking High Capacity Galvanized Steel Frame System
- High-bay vertical clearance up to 16 meters
- Ultra-stiff cross-beam deflection limit (L/300)
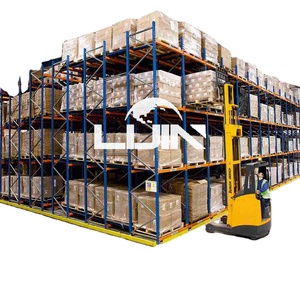
High Standard OEM Live Pallet Rack Gravity Flow Rack
- Incline-sloped cross beams with speed controllers
- High pallet separation safety stop barriers
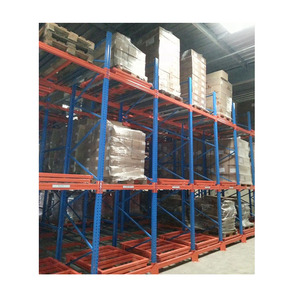
Heavy Duty Push Back Pallet Rack Customized High Quality Adjustable Dexion Warehouse Storage Racking System
- 2 to 6 pallet-deep nested rolling carriage carts
- Multi-claw heavy connector ends with safety pins
The Mechanics of Load-Bearing Racking Cross Beams: Structural Integrity, Deflection Limits & Material Selection
In high-density industrial logistics centers, the pallet racking cross beam represents the principal horizontal structural element subjected to sustained combined loading: continuous vertical shear, longitudinal bending moments, torsional rotation induced by off-center pallet placements, and seismic-induced lateral dynamic oscillations. Selecting the proper beam geometry and steel composition is the singular deciding factor in safeguarding structural integrity and preventing catastrophic warehouse progressive collapses.
1. Cross Beam Profile Geometries: Continuous Box vs. Step Beams
Pallet racking load beams are divided fundamentally into two engineering geometries: continuous box beams and stepped beams. Each has distinctive structural benefits dictated by warehouse handling methodology:
Welded Interlocking Box Beams: Composed of two precision-nested C-sections continuously seam-welded using automated dual-head robotic MIG machinery. The resulting closed hollow structural section (HSS) delivers remarkable polar moments of inertia ($I_x$ and $I_y$), providing elevated resistance against torsional twisting when heavy fork trucks make erratic pallet contact. Box beams are the preferred choice for standard selective pallet systems holding EUR-1 (800 × 1200 mm), EUR-2 (1200 × 1000 mm), and American GMA (48 × 40 in) pallets across spans reaching 3900 mm.
Roll-Formed Step Beams: Engineered with a top inner recessed flange (typically 20 mm to 25 mm deep). This internal step serves as a flush-mount cradle for galvanized wire mesh decks, drop-in bar grating, or timber shelving. The step design guarantees that fire sprinkler suppression streams penetrate directly through open wire decking without sheet steel obstruction, adhering directly to international FM Global and NFPA 13 warehouse safety codes.
| Profile Dimension (H × W × T mm) | Steel Grade (Yield / Tensile) | Standard Span (mm) | Uniformly Distributed Load (UDL / Pair) | Max Allowable Deflection (EN 15512) | Connector Claws |
|---|---|---|---|---|---|
| Box 80 × 50 × 1.5 | Q235B (235 / 375–500 MPa) | 2300 mm (2 Pallets) | 1,800 kg / level | 11.5 mm (L/200) | 3-Claw Laser Stamped |
| Box 100 × 50 × 1.5 | Q235B (235 / 375–500 MPa) | 2700 mm (3 Euro Pallets) | 2,200 kg / level | 13.5 mm (L/200) | 3-Claw Welded |
| Box 120 × 50 × 1.8 | Q355B (355 / 470–630 MPa) | 2700 mm (Heavy Stillage) | 3,200 kg / level | 13.5 mm (L/200) | 4-Claw High Moment |
| Box 140 × 50 × 1.8 | Q355B (355 / 470–630 MPa) | 3300 mm (3 Industrial Pallets) | 3,600 kg / level | 16.5 mm (L/200) | 4-Claw High Moment |
| Box 160 × 50 × 2.0 | Q355B (355 / 470–630 MPa) | 3600 mm (Heavy Bulk Chemical) | 4,500 kg / level | 18.0 mm (L/200) | 5-Claw Extreme Shear |
| Step 100 × 50 × 1.5 | Q235B (235 / 375–500 MPa) | 2700 mm (Wire Deck Recessed) | 2,000 kg / level | 13.5 mm (L/200) | 3-Claw Laser Stamped |
2. Connector End Plate Metallurgy & Safety Locking Pin Engineering
The beam-to-column connection serves as a semi-rigid structural joint. Rotational stiffness ($C_i$) within this joint dictates the effective buckling length of vertical upright columns. Our high-precision connection assemblies feature:
Heavy-Gauge Drop-Forged Connector Claws: Utilizing cold-stamped 3.5 mm to 4.0 mm structural steel plates with 3-claw, 4-claw, or 5-claw interlocking finger configurations. The tapered hook geometry is precision-slotted to match European 50 mm / 75 mm and teardrop upright perforations, seating tightly into the column throat under pallet dead load to generate maximum mechanical wedging resistance.
Spring-Steel Positive Locking Pins: Every beam end is equipped with an electro-galvanized high-shear safety retaining pin capable of withstanding a minimum 5.0 kN upward dislodgement force (certified to EN 15512 clause 5.3.3). This mechanism prevents beam disconnects during sudden forklift tines misplacement or driver elevation errors.
Emerging Trends Shaping Global Racking Procurement (2025–2030)
International warehouse developers, logistics REITs, and 3PL procurement directorships face evolving technical and regulatory mandates. Integrating high-performance cross beams demands an understanding of these shifts.
1. Transition to High-Yield Cold-Formed Steel
Global supply chains are shifting rapidly from traditional low-yield Q235B (comparable to S235JR) to high-tensile micro-alloyed Q355B (S355JR) steel grades. By capitalizing on an increase in yield strength from 235 MPa to 355 MPa, beam wall thicknesses are optimized from 2.0 mm down to 1.5 mm while elevating overall load capacity. This shift achieves up to a 15% reduction in dead tare weight, decreasing containerized freight costs across international sea routes.
2. AMR & High-Speed Automation Integration
The explosive adoption of Autonomous Mobile Robots (AMRs) and automated shuttle carriers across FMCG distribution requires exceptional manufacturing consistency in cross-beam production. Standard commercial tolerances (±3 mm) are no longer adequate. Modern automated systems mandate beam span deviations of less than ±1.0 mm and minimal vertical curvature to prevent optical sensor misreads and docking jams.
3. Sub-Zero Cold-Chain Metallurgy
Cold-chain pharmaceutical and deep-freeze logistics (-30°C) cause structural carbon steel to undergo ductile-to-brittle transitions. Sourcing teams are turning to impact-tested low-carbon steel specifications (Charpy V-Notch ≥ 27 Joules at -20°C) coupled with low-temperature thermoset TGIC-free polyester powder coats that prevent micro-cracking and subsequent subsurface delamination.
State-of-the-Art 10-Step Automated Production Process
Operating from our 30,000 m² production facility in Guangzhou, China, HEDA Shelves processes up to 30,000 metric tons of certified structural steel monthly, utilizing precision CNC machinery and automated lines.
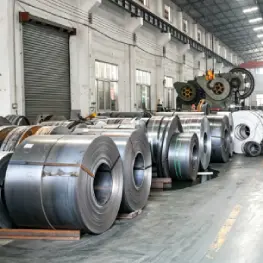
Raw Material Testing
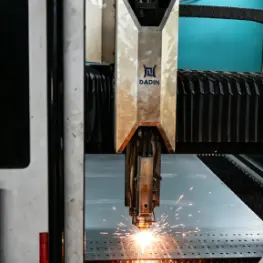
Precision CNC Slitting
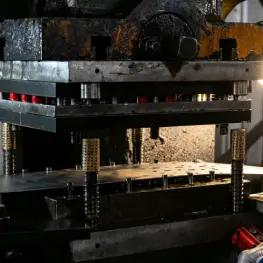
Automated Punching
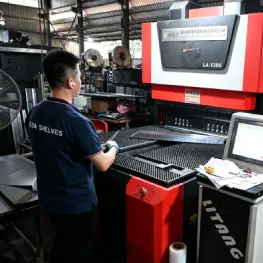
Cold Roll Bending
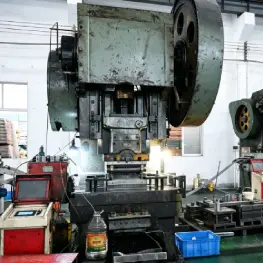
Multi-Pass Forming
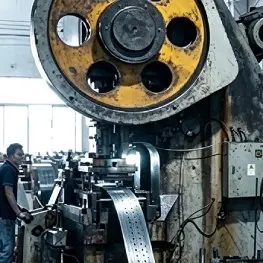
Surface De-burring
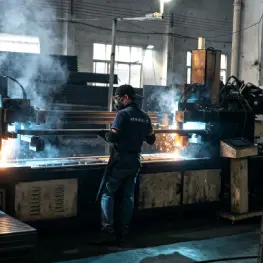
Robotic MIG Welding
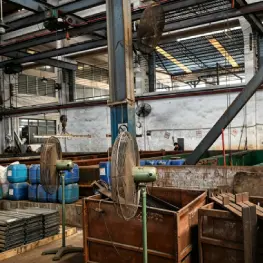
9-Stage Pretreatment
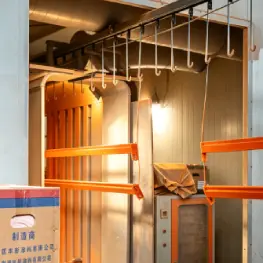
Powder Coating (80μm)
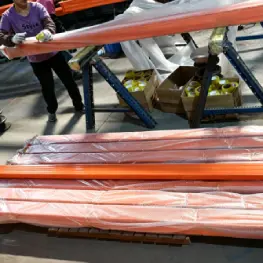
Seaworthy Export Bundling
Certified Manufacturing That Withstands Rigorous Site Audits
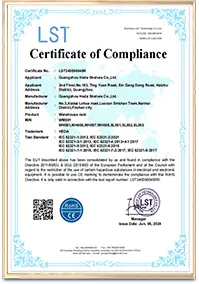
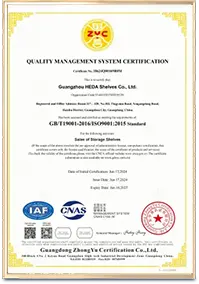
International warehouse projects require verifiable documentation. HEDA Shelves provides certified factory load charts, mill test certificates (MTC), and official testing records with every outbound shipment.
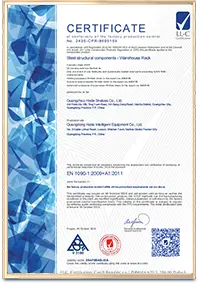
CE Certificate: 2435-CPR-8605159
Certified in strict compliance with the European Construction Products Regulation (CPR). Full mechanical conformity to EN 15512, EN 15620, and EN 15629 engineering requirements for industrial steel storage equipment.
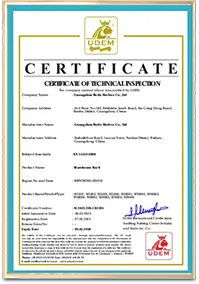
ISO 9001:2015: 18624Q00169R0M
Independently audited quality management system overseeing everything from spectrometer raw material steel verification to ultrasonic weld-seam integrity and finished powder adhesion grid tests.
Direct OEM / Private-Label Capability
We supply European distributors, major system integrators, and racking contractors with custom connector slot designs, bespoke RAL powder-coat hues (RAL 5015, RAL 2004, RAL 7035), and branded export packaging.
Frequently Asked Questions for Technical & Sourcing Teams
In-depth answers addressing structural engineering, profile selection, certification, and export logistics for procurement professionals and structural consultants.
What calculations determine beam selection for standard EUR-1 (1200 × 800 mm) pallets? +
How do you verify weld penetration and prevent connector end fatigue failures? +
Can your factory provide custom punch compatibility for existing European or American uprights? +
What surface treatment prevents rust in high-humidity or cold-chain environments? +
What are the lead times and container loading capacities for export orders? +
What technical documentation is provided to support client warehouse permitting? +
Plan Your Storage Project with HEDA Engineers
Submit your warehouse layout, pallet specifications, and target load parameters. Our engineering department delivers a comprehensive CAD proposal, static load calculations, and competitive factory-direct pricing within 24 working hours.