Heavy-Duty Tall Pallet Racking Systems
Precision roll-formed uprights manufactured from high-tensile Q235B and Q355B structural steel, specifically designed for high-density vertical warehouses, automated logistics hubs, and cold-storage operations worldwide.
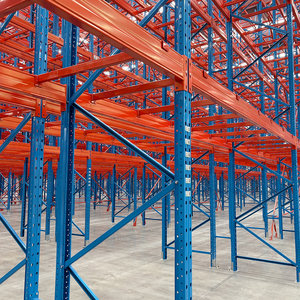
Heavy Duty Modular Cold Room Pallet Racking System
- Operating Temp: Down to -35°C Sub-Zero
- Bay Capacities: 1,000 – 4,500 kg/tier
- Anti-Embrittlement Cold-Formed Steel
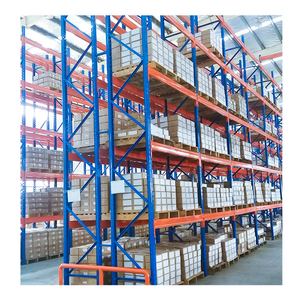
Heavy Duty Selective Steel Pallet Racking System
- 100% Direct Immediate Pallet Selectivity
- Upright Profiles: Up to 15m Single Piece
- Pitch Adjustment: 50mm / 75mm Precision
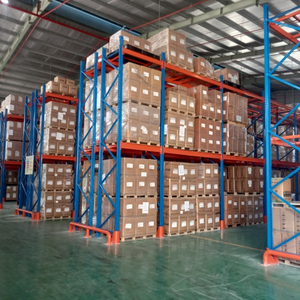
Engineered Selective Racking for Cold Storage Logistics
- Epoxy Polyester Thermosetting Finish
- Euro & Industrial Pallet Adaptable
- EN 15512 Safety Load Certification
Tall Industrial Logistics Pallet Racking (Custom Height)
- Upright Heights Engineered Beyond 20m
- Reinforced Box Beams & Heavy Baseplates
- FEA Simulated Seismic Dynamic Bracing
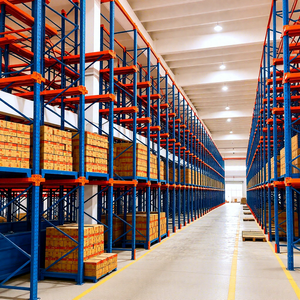
Tall Drive-In Pallet Racking for Maximum Volume
- Eliminates Picking Aisles (Up to 85% Vol. Use)
- Continuous Support Rails with Lead-In Arms
- Strict LIFO or FIFO Drive-Through Formats
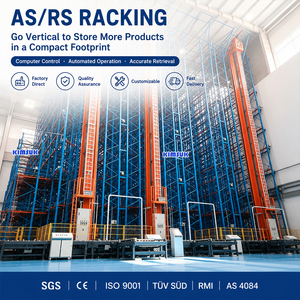
Seismic AS/RS Automated High-Bay Racking Structure
- Automated Stacker Crane Tolerances (EN 15620)
- Vertical Clearance Limits Exceeding 35m
- Structural Clad-Rack Self-Supporting Option
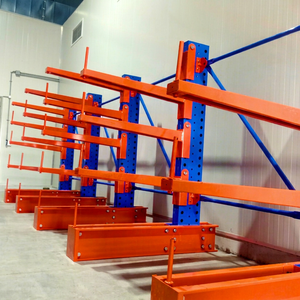
Heavy Duty Tall Cantilever Pallet Racking System
- Open Front for Pipes, Extrusions & Timber
- Column Loading Up to 18,000 kg per Side
- Hot-Dip Galvanized / Powder Coated
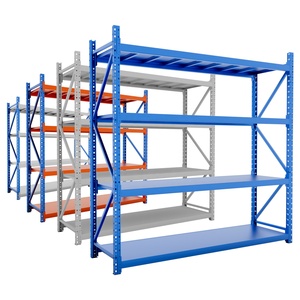
High-Bay Longspan Integrated Pallet Storage Rack
- Hybrid Bulk Pallet Base + Upper Tier Shelves
- Decking: Steel Panels, Wire Mesh, or Plywood
- Rapid Knockdown Bolt-Free Connectors
Structural Design Principles of Tall Pallet Racking (12m – 40m+)
In modern high-density distribution centers, escalating land costs have accelerated the structural migration toward the vertical plane. Engineering tall pallet racking—defined structurally as rack configurations exceeding 12 meters clear height up to 40 meters in automated clad-rack silos—introduces rigorous structural physics that deviate entirely from standard low-bay shelving. As China's premier manufacturer and exporter of tall industrial storage, Guangzhou Heda Shelves Co., Ltd. applies advanced finite element analysis (FEA) to counteract structural sway, torsional buckling, and seismic shockwaves.
The manufacturing integrity of high-bay upright columns demands ultra-tight dimensional tolerances. When vertical uprights are stacked or roll-formed continuously to heights exceeding 18 meters, any micro-deviation in column straightness (camber or sweep) is multiplied along the structural height vector. According to European standard EN 15620 (Class 100 to 300 tolerances for VNA and AS/RS installations), out-of-plumbness tolerances must not exceed 1:750 of overall height. Our continuous roll-forming lines operate computerized servo punches that maintain hole-pitch center accuracy within ±0.15mm across a 12-meter section, guaranteeing flawless crane tracking and narrow-aisle forklift stability.
Critical Material Science: High-Yield Steels & Cold-Chamber Resilience
Heda strictly selects primary-mill Q235B and Q355B structural steel coils from Baosteel and Shougang. For ultra-tall automated racking installations and seismic active regions (Zone 3 and 4), high-yield Q355B (equivalent to European S355JR) provides elevated minimum tensile yield strength (≥ 355 MPa), ensuring upright frames resist dynamic deceleration loads inflicted by fast-accelerating automated storage and retrieval machines (SRMs). In sub-zero cold room environments (-25°C to -35°C), cold-embrittlement constitutes a fatal operational hazard; we employ micro-alloyed killed steels with validated Charpy V-notch impact toughness test ratings exceeding 27 Joules at -40°C.
Structural Comparison: Low-Bay vs. Standard High-Bay vs. Automated Tall Silo Racking
A comprehensive side-by-side comparative metric for structural design engineers, logistics directors, and general procurement teams:
| Engineering Metric | Standard Selective (Low-Bay) | Tall VNA Racking (12m - 18m) | Automated High-Bay Silo (18m - 40m+) |
|---|---|---|---|
| Height Range | 3.0m – 8.5m | 12.0m – 18.5m | 18.0m – 42.0m (Clad-Rack) |
| Governing Standard | EN 15512 / RMI MH16.1 | EN 15620 / FEM 10.2.02 | FEM 9.831 / EN 16681 (Seismic) |
| Column Straightness | 1 / 500 max deflection | 1 / 750 (Strict VNA tolerance) | 1 / 1000 (Laser aligned AS/RS) |
| Handling Equipment | Counterbalance / Reach Truck | Man-Up / Man-Down VNA Turret | Automated Stacker Crane (SRM) |
| Aisle Width Requirement | 3,200mm – 3,800mm | 1,650mm – 1,900mm | 1,350mm – 1,550mm |
| Volumetric Efficiency | 40% - 50% | 70% - 80% | 88% - 95% |
| Floor Anchorage Anchor | Standard Expansion Bolts M12 | Chemical Resin Anchors M16-M20 | Heavy Pre-Cast Embedment Anchor Studs |
Why Tier-1 Global EPCs Partner with Guangzhou Heda Shelves
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized metal stamping workshop into one of Asia's most recognized export fabrication bases for high-bay intralogistics racking. With over 300 experienced technicians, robotic welding automation, and dedicated structural testing rigs, our 30,000 square meter facility delivers turnkey supply contracts with zero-defect quality standards.
Massive Scale & Fast Dispatch
Our monthly output of 30,000 metric tons guarantees that large multi-thousand-pallet projects ship on schedule via major coastal ports in Guangzhou, Shenzhen, and Hong Kong.
Free CAD & 3D Structural Simulation
Our structural engineering office generates complete DWG layout blueprints, dynamic load charts, and 3D warehouse simulations before purchase orders are signed.
Internationally Audited Quality
Certified under CE No. 2435-CPR-8605159 and ISO 9001:2015 No. 18624Q00169R0M. All raw metals and surface coatings undergo rigorous RoHS and salt-spray durability testing.
Precision CNC Automated Fabrication
12 automated multi-station cold roll-forming lines, Panasonic robotic laser welding stations, and continuous electrostatic powder coating tunnels guarantee micron-level consistency.
Future Procurement Trends in Tall Warehouse Pallet Storage
Global supply chain directors and industrial real estate investors are confronting seismic shifts in warehousing economics. The procurement of tall pallet racking is no longer a simple structural commodity buy—it has transformed into a strategic capital investment.
Automation-Ready Standardization
Buyers are mandating that all static high-bay racks feature pre-punched mounting holes and deflection thresholds that accommodate future retrofit of AMR shuttles or AGVs without structural modifications.
EPD Carbon Footprint Mandates
Global ESG benchmarks require Environmental Product Declarations (EPD). Modern factories using electric-arc-furnace recycled steel and low-VOC powder coats will capture preference in multi-national tenders.
Pre-Engineered Clad-Rack Buildings
Rising civil construction costs have sparked massive demand for rack-supported clad-rack buildings where the tall pallet uprights serve directly as the primary load-bearing structural columns of the warehouse roof and walls.
Modular Nearshoring Spares Supply
Global procurement teams favor tier-1 Chinese manufacturers maintaining standardized beam connector pin geometries that allow rapid interchangeability and lower maintenance carrying costs across worldwide sites.
Digital Twin Sensor Integration
Integration of wireless strain gauges and load sensors inside upright baseplates to provide live telemetry on rack fatigue, over-capacity alerts, and seismic displacement logging directly to warehouse WMS/ERP systems.
Procurement Strategy Analysis: The Total Cost of Ownership (TCO) Shift
In legacy procurement models, purchasing managers evaluated tall racking purely on initial steel tonnage costs ($/ton). However, empirical post-installation data from tier-1 distribution hubs demonstrates that initial steel expense accounts for merely 42% of a tall racking facility's 15-year lifecycle cost. The remaining 58% comprises civil floor levelling remediation, installation crane rental, annual structural integrity recertification under EN 15635, damage repairs, and operational downtime caused by beam deflection.
By partnering directly with a certified Chinese manufacturer like Heda Shelves, buyers capture up to a 35% reduction in initial fabrication expenditures while securing certified high-grade steels (Q355B), dual-sided powder coating with 80-120 micron dry film thickness (DFT), and pre-tested bolted splices. This directly mitigates long-term deflection, prevents corrosion in chilled environments, and minimizes lifetime maintenance cycles.
Technological Evolution of High-Bay Racking Systems
How advanced metallurgy, digital twin finite element simulation, and automated intralogistics robotics are revolutionizing the next generation of tall pallet storage structures.
Frequently Asked Questions on Tall Pallet Racking Procurement
Comprehensive, engineering-backed answers to the technical, logistical, and commercial inquiries most frequently raised by international buyers, consultants, and contractors.
We fabricate single-piece continuous upright columns up to 18 meters on our computerized roll-forming production lines. For installations between 18 meters and 42 meters (such as AS/RS clad-rack high-bay warehouses), we engineer structural spliced frames with reinforced precision CNC-machined internal splice channels and grade 10.9 high-tensile bolts, maintaining complete structural alignment and full load transfer without structural flexing.
For free-standing outdoor racks and clad-rack warehouse buildings, our engineering department performs full 3D Finite Element Analysis (FEA) compliant with EN 16681 (Seismic Racking Design), EN 1991-1-4 (Wind Actions), and ASCE 7 / RMI standards. We configure vertical cross-bracing towers, top portal ties, and heavy anchored baseplates based on local spectral ground acceleration values (Ss, S1) and basic design wind speeds provided for your specific site.
We utilize certified prime structural steels: Q235B (yield strength ≥ 235 MPa) for standard ambient beams and bracing, and Q355B (yield strength ≥ 355 MPa, equivalent to European S355JR / ASTM A572 Gr 50) for heavy-load tall uprights and critical seismic upright frames. Every production batch is accompanied by EN 10204 3.1 Mill Test Certificates verifying carbon equivalence, chemical composition, tensile yield, elongation, and Charpy impact properties.
Components undergo an automated 9-stage pre-treatment process: alkaline degreasing, water rinsing, acid pickling, zinc phosphating, and deionized neutralization before entering the electrostatic powder coating line. Powder coatings are baked at 180°C - 200°C to achieve 80–120 microns DFT. For ocean container shipping, upright frames and beams are strapped with high-density corrugated board, wrapped in moisture-barrier PE shrink film, and bundled with desiccants to completely prevent sea-air oxidation.
Yes. We regularly supply European distributors and intralogistics system integrators with OEM and ODM manufacturing. Our modular tooling allows us to roll-form uprights and box beams matching major European pitch configurations (such as 50mm, 75mm, and 76.2mm pitches), customized teardrop punches, and custom RAL corporate colors (RAL 5015 blue, RAL 2004 orange, RAL 7035 grey, etc.) with client private branding.
Tall pallet racking installations—especially VNA and AS/RS systems—place concentrated point loads (often 80 to 250 kN per baseplate) on the concrete slab. Floors must comply with DIN 18202 (Table 3, Line 4) or TR34 (Category Free Movement FM2 or Defined Movement DM1 / DM2). Minimum concrete compressive strength should be C28/35 or C30/37, with adequate slab thickness (typically 200mm – 300mm reinforced) to prevent punch-through and ensure anchor pull-out ratings are preserved.
Each shipment includes a complete structural verification dossier: 1) Approved CAD general arrangement drawings and assembly elevations; 2) Structural static calculation reports signed by structural engineers; 3) CE Declaration of Performance (DoP) under EN 1090 / CPR; 4) ISO 9001:2015 quality inspection and mill test certificates; 5) Detailed step-by-step installation manuals and safety load notice plaques for rack end frames.
All structural members feature laser-etched or color-coded part numbers matching our 3D assembly shop drawings. For major international projects across Europe, the Middle East, Southeast Asia, and the Americas, Heda provides two installation support tiers: complete remote video technical engineering guidance for local installation crews, or the direct dispatch of bilingual senior installation site supervisors to oversee alignment, plumb checks, and torque audits on site.
Accelerate Your High-Bay Warehouse Project With Factory-Direct Engineering
Bypass intermediary markups and communication delays. Consult directly with Guangzhou Heda Shelves' senior structural design department to configure optimized tall pallet racking, VNA installations, or automated AS/RS storage systems engineered specifically for your building dimensions and budget.
- Free 24-Hour CAD Layout & 3D Renderings
- EN 15512 & RMI Structural Load Calculations
- Full European Pallet (EUR/EPAL) Customization
- FOB, CIF, or Turnkey DDP Delivery to Any Port
Request Technical Proposal
Connect immediately with our structural racking team. Provide your building clearance height, pallet dimensions, and forklift type to receive an engineered layout and factory quotation.