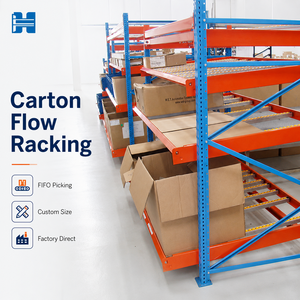
Precision Heavy-Duty Inventory
Engineered Warehouse Storage Racking & High-Density Systems
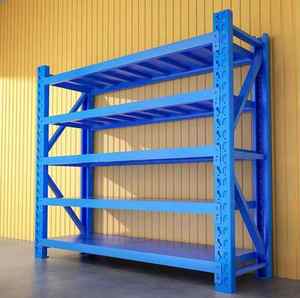
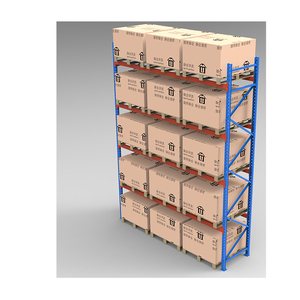
Directly fabricated by Guangzhou Heda Shelves Co., Ltd. from cold-rolled structural steel. Fully adaptable to EUR/EPAL dimensions, high-bay turret trucks, and automated carton replenishment streams.
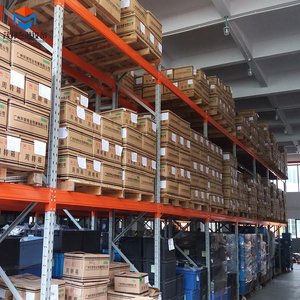
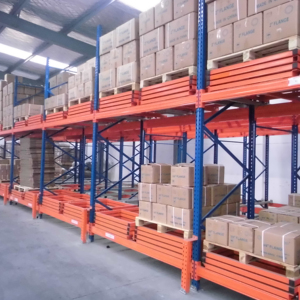
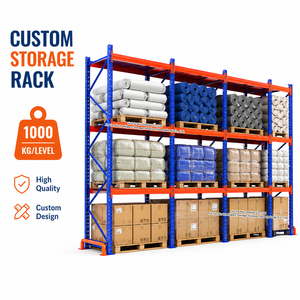
Engineering Whitepaper & Structural Architecture
The Mechanics of High-Bay Very Narrow Aisle (VNA) Pallet Racking
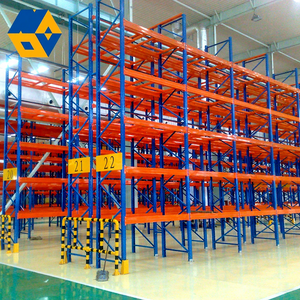
In modern logistics, industrial real estate values have escalated global storage economics into three-dimensional vertical optimization. VNA systems eliminate dead operational floor space by condensing operating aisles down to 1,500 mm – 1,800 mm, boosting volumetric density by up to 45% over conventional APR setups.
Cold-Formed Upright Profiles
Continuous roll-formed Omega-sections engineered from high-yield Q235B and Q355B modified structural steel. Featuring high moment-of-inertia cross sections designed to mitigate torsional-flexural buckling at heights surpassing 16 meters under stringent EN 15512 calculation criteria.
Floor Flatness: VDMA & DIN 18202
High-reach VNA turret trucks running at mast heights over 12m require strict floor planarity. We engineer baseplates and anchor load distributions to comply with VDMA 15251 and DIN 18202 Table 3 Line 4 tolerances, preventing catastrophic dynamic mast deflection and resonance sway.
Dual Guidance Infrastructure
Custom structural guidance configurations: High-precision hot-rolled steel mechanical angle guide rails (e.g. L75×50×6 mm with low-entry flared lead-ins) or buried sub-floor inductive wire loops emitting standard 5 kHz to 40 kHz navigational signals for autonomous AGV and man-up turret steerage.
100%
Pallet Accessibility
1,500mm
Minimum Aisle Width
18m
Engineered Maximum Height
+45%
Cubic Volume Increase
Deflection Limits, Safety Multipliers & Load Beam Connections
In narrow aisle high-bay systems, dynamic impact allowances and deflection thresholds are far more stringent than standard wide-aisle adjustable pallet racking (APR). Guangzhou Heda Shelves applies an active elastic-plastic structural modeling method across all VNA projects. Under standard EN 15512 specifications, load beam deflection is constrained to a maximum of $\delta \le L / 200$ (or $L / 250$ for automated handling interfaces) under ultimate continuous service loads.
Beam end-connectors utilize proprietary 4-claw or 5-claw high-ductility steel cold-stamped brackets that engage seamlessly into upright teardrop or diamond slot patterns on a 50 mm or 75 mm vertical pitch. High-shear safety locking pins prevent disengagement under unexpected mast shear shocks. Furthermore, the baseplates feature anchored expansion configurations designed to resist significant localized vertical uplift moments generated during single-sided high-bay pallet loading sequences.
Logistics Engineering Evaluation
VNA Pallet Racking vs. Alternative Storage Systems
Data-driven performance benchmark evaluating storage density, accessibility, operational throughput, and capital investment across mainstream warehouse configurations.
| Storage System Type | Aisle Clear Width (mm) | Floor Utilization (%) | Pallet Selectivity | Stock Rotation Rule | CapEx vs. Density Rating |
|---|---|---|---|---|---|
| VNA Pallet Racking (Heda System) | 1,500 – 1,800 | Up to 60% – 65% | 100% (Direct Single Access) | FIFO / LIFO Independent | Highest ROI / Volumetric Gain |
| Standard Selective Racking (APR) | 3,000 – 3,600 | 35% – 40% | 100% (Direct Single Access) | FIFO / LIFO Flexible | Low CapEx / Low Density |
| Double Deep Pallet Racking | 3,000 – 3,400 | 50% – 55% | 50% (Requires Reach Truck) | Strict LIFO (per lane) | Moderate CapEx & Selectivity |
| Drive-In / Drive-Through Racking | Continuous Lane | 65% – 75% | Low (<15% Direct Access) | Strict LIFO / Lane Bulk | Low Cost / SKU Inflexible |
| Radio Shuttle Automation Racking | Aisle Transfer Free | 75% – 85% | Channel Selective | FIFO or LIFO Programmable | High CapEx / Premium Cold Store |
Consulting Engineer Note on Building Clear Height:
VNA infrastructure yields its most dramatic ROI when warehouse ceiling clearance extends past 8 meters up to 18 meters. At these heights, standard counterbalance forklifts cannot operate safely, and reach trucks lose significant residual capacity. VNA turret trucks—operating inside guided aisles—retain full structural lifting capacities up to 1,500 kg at heights exceeding 14 meters.
Market Intelligence & Industry Horizon
VNA Pallet Racking Procurement & Future Technological Trends
Strategic supply chain forecasts for logistics facility developers, procurement managers, and automated material handling system integrators over the 2025–2030 horizon.
1. Convergence with Autonomous Mobile Turret AGVs
The rapid transition from manual "man-up" turret trucks to fully driverless Narrow Aisle Autonomous Guided Vehicles (AGVs). Racking engineering now prioritizes tighter millimeter-accurate clearances, precise bottom pallet optical datum reflectors, and rigid run-out tolerances at upright aisle portals.
2. Seismic Resilience: Eurocode 8 & EN 16681
Warehouses located in seismically active European zones (Italy, Balkans, Greece) or across seismic regions in the Americas require non-linear pushover structural analyses. Global buyers mandate finite element modeling (FEM) with dynamic modal simulations to guarantee frame ductility and beam connector dissipation under ground acceleration.
3. CBAM-Compliant Green Steel Supply Chains
As the European Carbon Border Adjustment Mechanism (CBAM) phases in, procurement directors require audited Scope 1, 2, and 3 carbon accounting. Our manufacturing utilizes low-emission blast furnace and electric arc furnace (EAF) coil sourcing combined with low-VOC closed-loop electrostatic powder coating lines.
Direct-From-Factory Sourcing vs. Local Distributor Arbitrage
Historically, international warehouse developers procured VNA systems exclusively through regional European or domestic integrators at markups ranging from 35% to 65%. Today's global procurement paradigm leverages direct Tier-1 Chinese manufacturing partnerships. By retaining complete engineering oversight via direct CAD/BIM model exchange and independent third-party mill testing, contractors secure factory pricing without compromising steel grade authenticity, weld penetrations, or certified CE/EN tolerances.
Manufacturing Powerhouse
Guangzhou Heda Shelves Co., Ltd. — 25 Years of Production Mastery
Established in 2001, Heda Shelves has grown into a leading industrial warehouse storage manufacturer. Our advanced production campus delivers end-to-end fabrication control for international distribution hubs, third-party logistics (3PL) centers, and cold-chain complexes.
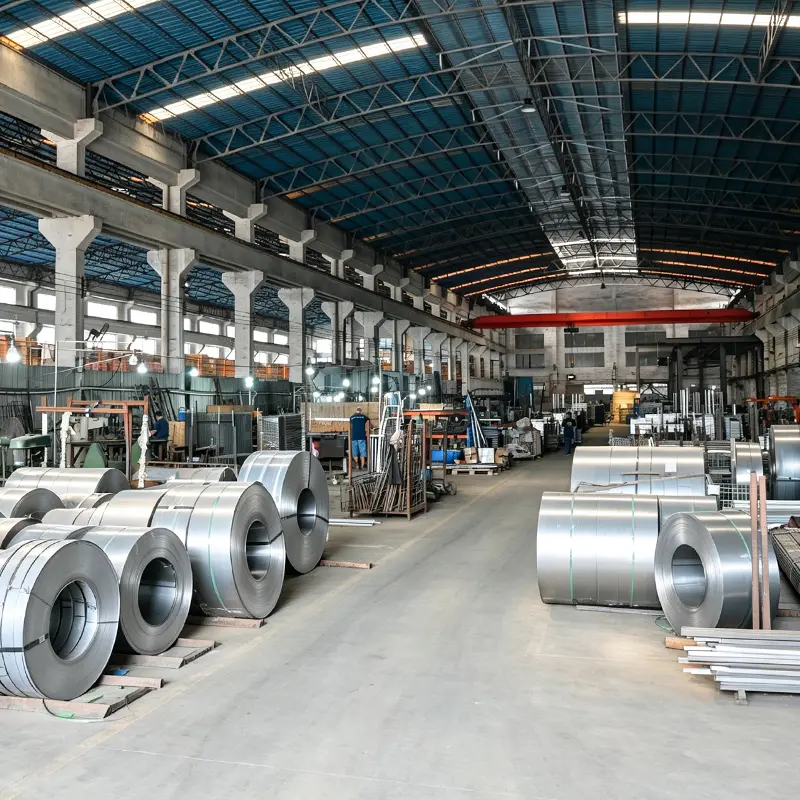
EXPERIENCE
25+ Years Industrial Track Record
Founded in 2001, completing over 10,000 successful warehouse installations worldwide. Our structural engineering team specializes in resolving complex slab load limits, seismic restrictions, and custom layout constraints.
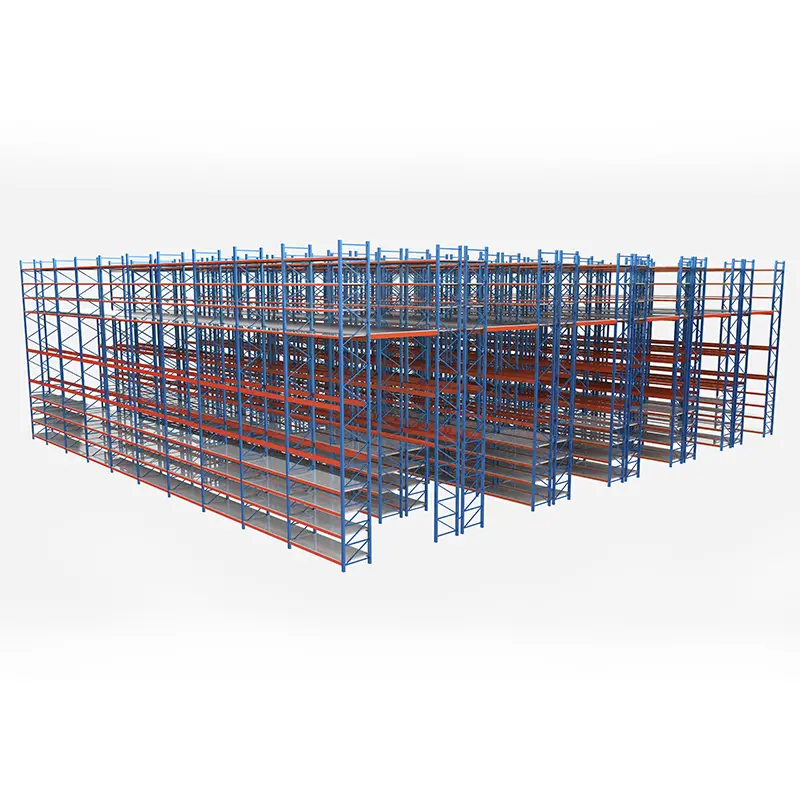
ENGINEERING
Free 3D & CAD Layout Consultation
Complete architectural coordination prior to commercial commitments. We generate full DWG floor designs, 3D spatial stress-renderings, calculation notes, and bill of materials verified against your forklift kinematic envelopes.
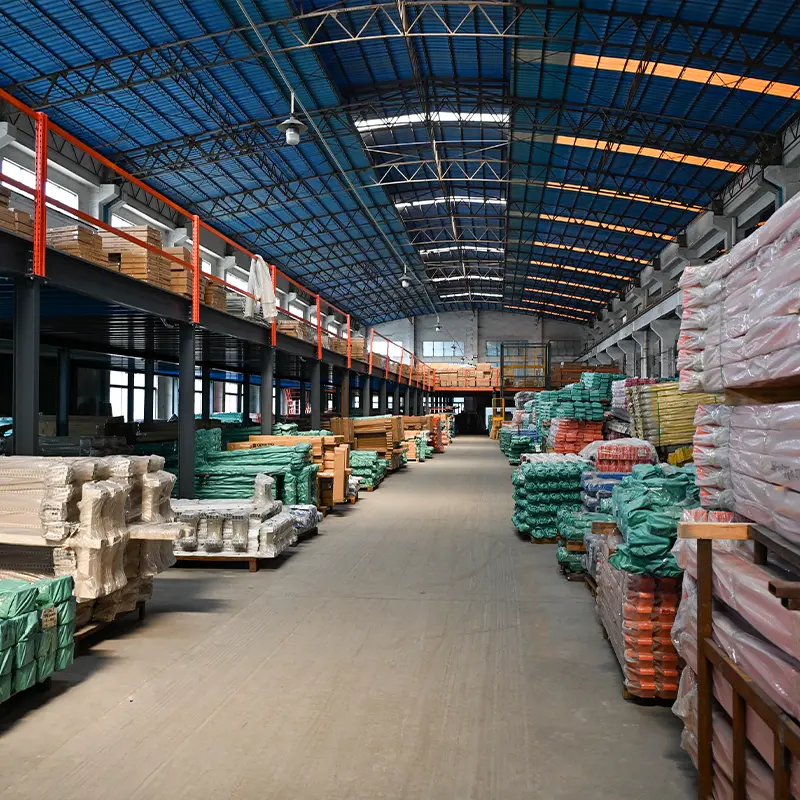
QUALITY
ISO 9001 & CE Certified Production
Rigorous mill-certified Q235B/Q355B coil stock. Every structural batch undergoes tensile yield tests, automated multi-point punching, automated continuous roll-forming, and high-adhesion anti-scratch electrostatic powder coating.
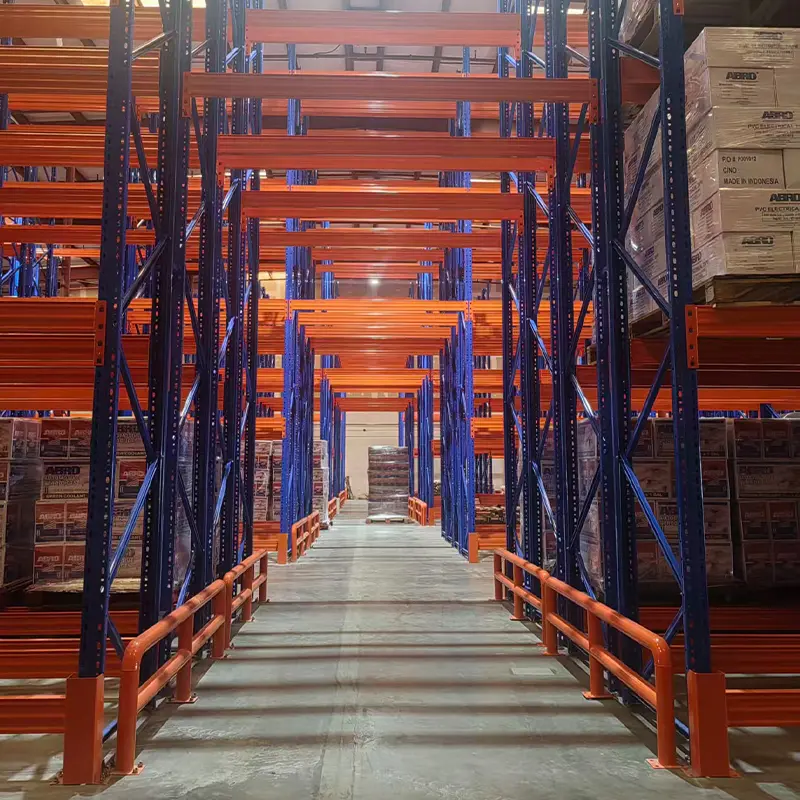
CUSTOMIZATION
100% Turnkey OEM & ODM Flexibility
Fully customizable frame depths, clear beam spans, upright steel thicknesses (1.5mm to 3.0mm+), special RAL color coding for picking lanes, guide rail systems, and heavy-duty seismic baseplate anchoring hardware.
Zero-Defect Quality Assurance
Inside HEDA’s 10-Step Automated Manufacturing Cycle
Operating from our 30,000 m² factory campus with 300+ skilled technicians, our monthly production capacity reaches 30,000 metric tons. Every racking member traverses an automated quality control sequence.
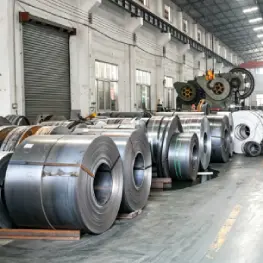
Step 01
Raw Material Mill Testing
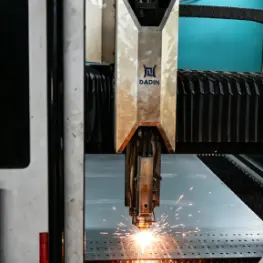
Step 02
CNC Slitting & Uncoiling
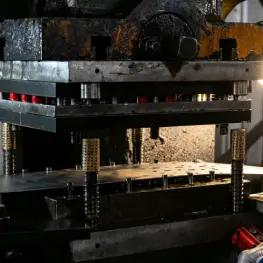
Step 03
Automated High-Speed Punching
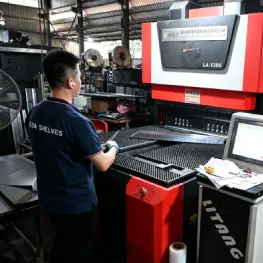
Step 04
Continuous Cold Roll-Forming
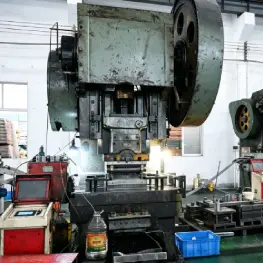
Step 05
Box-Beam Seam Locking
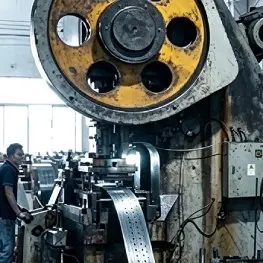
Step 06
Surface Polishing & Deburring
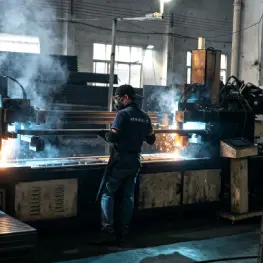
Step 07
Robotic Connector Welding
Step 08
9-Stage Chemical Pre-Treatment
Step 09
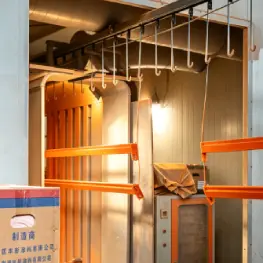
GEMA Electrostatic Coating
Step 10
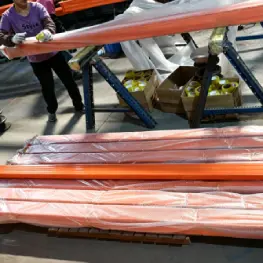
Seaworthy Export Bundling
Accredited Quality Systems
Independent Factory Testing & European Verification
Full compliance documentation supplied with every international order. All certificates are actively verifiable via designated European notified registries and international QA organizations.
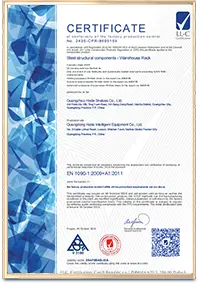
CE Certificate No. 2435-CPR-8605159
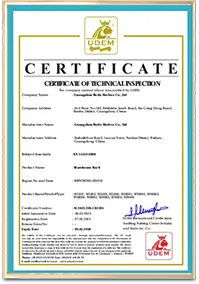
ISO 9001:2015 No. 18624Q00169R0M
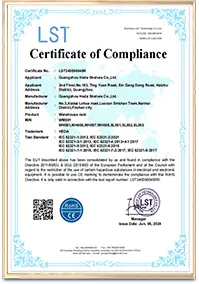
Mechanical Steel Loading Reports
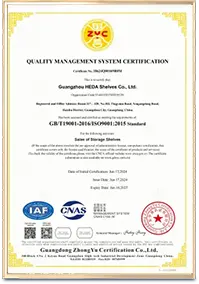
RoHS & REACH Finishing Compliance
Technical Procurement Clearinghouse
Frequently Asked Questions: Industrial VNA Racking
Detailed answers prepared by senior structural engineers covering floor requirements, international shipping logistics, and EN 15635 compliance.
What warehouse concrete floor flatness specifications are required for VNA racking?
Very Narrow Aisle installations require specialized floor classification due to the physics of high-elevation turret truck lifting. Mast heights of 10m to 16m magnify minuscule floor irregularities into dynamic side-sway oscillations. We require floor construction adhering to DIN 18202 Table 3 Line 4 or VDMA 15251 F-min 75 to F-min 100 classifications across designated truck wheel paths. For legacy industrial slabs that do not meet these criteria, precision laser grinding along wheel running tracks or leveling steel grouting must be executed prior to upright base anchoring.
How do mechanical steel guide rails compare to inductive wire guidance systems?
Mechanical Guide Rails utilize low-profile angle iron ($L75\times 50\times 6$ mm or $L100\times 65\times 8$ mm) bolted directly into the concrete floor alongside the base of upright frames. They provide instant physical protection to bottom uprights and ensure foolproof manual alignment upon vehicle entry. Inductive Wire Guidance utilizes a copper conductor embedded in a 4 mm × 15 mm saw-cut slot centered along the aisle floor, operating on an oscillating alternating current frequency (typically 5 kHz to 40 kHz). Wire guidance eliminates aisle trip hazards, simplifies low-level manual hand pallet truck picking, and avoids physical floor rails that collect dirt and debris.
Can HEDA VNA racking adapt to both EUR/EPAL (1200×800 mm) and ISO (1200×1000 mm) pallets?
Yes. Guangzhou Heda Shelves custom-engineers clear beam lengths and frame depths to accommodate dual pallet standards. A standard bay designed for three EUR pallets typically utilizes a 2,700 mm beam with a frame depth of 1,000 mm (providing a standard 100 mm rear and front pallet overhang). For standard ISO industrial pallets (1200 × 1000 mm), frame depths are configured to 1,100 mm with clear bay widths of 2,300 mm (two pallets) or 3,300 mm (three pallets), incorporating safety pallet support bars, drop-in front-to-back cross ties, or flush wire mesh decking panels.
What engineering documentation is delivered for local building permit compliance?
Every international shipment is accompanied by a technical engineering dossier. This includes AutoCAD DWG erection diagrams, 3D structural schematics, mill test certificates (MTC) proving steel chemical composition and tensile elongation, and structural calculations referencing EN 15512:2020 or RMI (Rack Manufacturers Institute) guidelines. Load notices (statical capacity warning plaques) compliant with EN 15635 are supplied for display on every rack aisle end-frame.
How are oversized VNA upright frames packed for standard sea container shipping?
Standard 40-foot High Cube (40HQ) sea containers have an interior door height of 2,585 mm and an interior length of 11,800 mm. For VNA upright frames reaching heights between 12m and 18m, upright columns are fabricated in continuous modular sections and coupled on-site using heavy-duty structural internal splice joints. Uprights are bundled with protective steel dunnage strapping and moisture-barrier shrink wrap, while horizontal beams are nested in rigid steel frames to optimize cubic container utilization and eliminate transit denting.
What is the typical production timeline and door-to-door transit schedule?
Standard factory lead time for a 5-to-20 container VNA project averages 20 to 30 calendar days following technical drawing sign-off and color code confirmation. Maritime transit from Guangzhou or Shenzhen ports to major European maritime gateways (Rotterdam, Hamburg, Antwerp, Valencia) requires 30 to 40 days. Rail freight via the China-Europe Express offers accelerated transit (18 to 22 days) for expedited facility commissioning schedules.
Request an Engineered VNA CAD Layout & Factory Quote
Submit your facility floor plan (DWG/PDF), clear truss height, pallet parameters, and forklift technical data. Our structural engineers provide an optimized spatial plan, load calculations, and turnkey factory-direct pricing within 24 hours.
24-Hour Layout Turnaround
Structural Deflection Models
Direct Export Packaging
Inquire Now
Consult with a Senior Project Engineer