Engineered Pallet Racking & Industrial Shelving Systems
Explore our heavy-duty cold-formed steel racking systems fabricated in accordance with global structural standards. Each system delivers customizable beam levels, variable column gauges, and modular storage configurations for fast deployment.
Heavy Duty Storage Rack Pallet Rack System Shelf For Industrial Storage Rack
- Payload Capacity: 1,000–4,500 kg/level
- Steel Specification: Q235B / Q355B Grade
- Upright Pitch: 50 mm / 75 mm Adjustable
- Surface Coating: Electrostatic Powder Curing
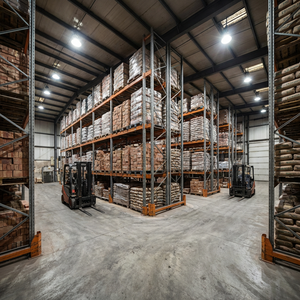
Heavy Duty Adjustable Pallet Rack Warehouse Storage Shelving System Steel Rack Manufacturer
- Payload Capacity: 800–3,500 kg/level
- Frame Heights: Up to 12,000 mm
- Safety Standard: CE No. 2435-CPR-8605159
- Configuration: Selective Single/Double Deep
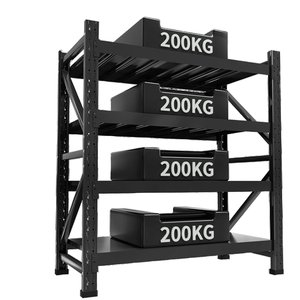
250KG Iron Adjustable Boltless Pallet Racking Long Span 5-Layer Light Duty Storage Shelving Units Garage Metal Stacking Steel
- Shelf Loading: 250 kg UDL/shelf
- Structure Type: Interlocking Boltless Keyhole
- Decking Medium: Cold-Rolled Steel / MDF
- Assembly Time: Under 10 mins / unit
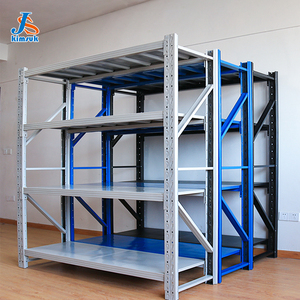
Racking Adjustable Metal Boltless Shelf and Racks Warehouse Storage Medium Duty Metal Rack Shelf
- Payload Capacity: 300–800 kg/tier
- Upright Profile: 55×47×1.5 mm Omega Section
- Connector Type: 3-Claw Safety Interlock
- Finish System: Zirconium Nano-Pretreated
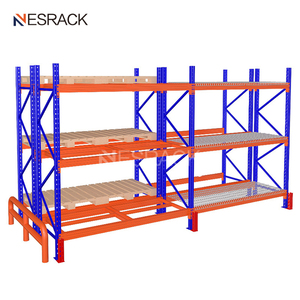
Adjustable Boltless Durable 4-Layers Steel Heavy Duty Pallet Rack 500-3000kg Warehouse Storage Rack
- Rated Load Capacity: 500–3,000 kg/level
- Standard Bay Length: 2,300 / 2,700 / 3,300 mm
- Safety Mechanism: Drop-In Locking Spring Pins
- Compliance: ISO 9001:2015 Audited
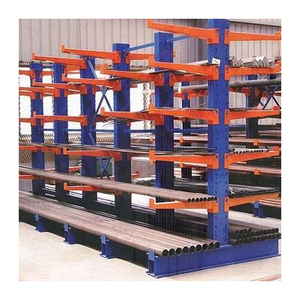
H-Beam Heavy Duty Cantilever Racks Steel Structural Shelf Industrial Warehouse Racking for Storaging Wooden Boards, Pipes
- Arm Capacity: 500–1,800 kg per arm
- Core Profile: Hot-Rolled Heavy H-Section
- Optimal Cargo: Pipes, Timber, Barrels, Steel
- Orientation: Single or Double Sided Tower
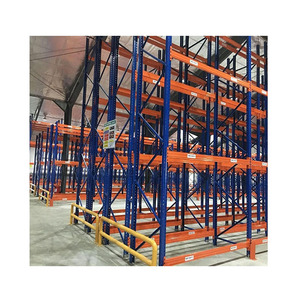
industrial galvanized steel rack heavy duty pallet racking system VNA/double deep high density warehouse storage racks
- Anti-Corrosion Spec: Hot-Dip Galvanized / Pre-Galv
- Aisle Footprint: 1,600–1,900 mm (VNA Turret)
- Operating Environment: Chilled / Deep Freeze (-30°C)
- Floor Utilization: Up to 85% Volumetric Density
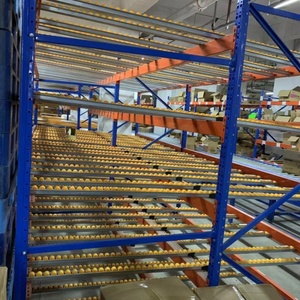
Industrial 5 Layer Heavy Duty Flow Rack Gravity-Fed Storage Solution for Warehouses Picking Efficiency for Boxes and Cartons
- Fulfillment Logic: Strict FIFO Inventory Rotation
- Roller Tracks: High-Impact Polyethylene/Steel
- Slope Angle: 3°–5° Gravity Gradient
- Application: E-Commerce & Split-Case Order Pick
Structural Steel Grade, Deflection & Seismic Design Matrix
Industrial racking procurement mandates empirical load validation under EN 15512:2020 and ANSI MH16.1 (RMI). Our engineering team calculates beam deflection limits at L/200 down to L/300 to eliminate seismic failure risks, torsional buckling, and connector sheared joints.
| Racking Architecture | Structural Profile | Yield Strength (Fy) | Max Load per Bay | Deflection Limit | Intralogistics Compatibility |
|---|---|---|---|---|---|
| Selective Pallet Racking | Upright 90×70×2.0 mm / Box Beam 120×50×1.5 | Q235B (235 MPa) | Up to 15,000 kg | ≤ L/200 | Counterbalance, Reach Trucks, Articulated VNA |
| High-Bay VNA System | Upright 120×95×2.5 mm / Step Beam 140×50×1.8 | Q355B (355 MPa) | Up to 24,000 kg | ≤ L/300 | Man-Up / Man-Down Wire-Guided Turret Cranes |
| Drive-In / Drive-Through | Upright 100×70×2.0 mm / Top Beam + Cantilever Brackets | Q235B (235 MPa) | Up to 18,000 kg | ≤ L/250 | Deep lane drive-in forklifts, cold room fleet |
| Radio Shuttle Automation | Custom Omega Rail System / HD Upright 120×95 | Q355B (355 MPa) | Up to 30,000 kg | ≤ L/300 | Automated battery carrier shuttles, WMS integration |
| Structural Cantilever Tower | Hot-Rolled Heavy H-Beam 200×100 to 300×150 | Q355B / SS400 | 5,000 kg per column side | ≤ L/180 | Side loaders, 4-way multi-directional mast trucks |
| Multi-Tier Mezzanine Deck | C-Section Primary Joists / Decking 300–1000 kg/m² | Q235B / S235JR | Up to 1,200 kg/m² | ≤ L/300 | Conveyors, spiral chutes, order picking trolleys |
Emerging Trends in Global Warehouse Racking Procurement (2025–2030)
Macroeconomic shifts, automated intralogistics expansion, and carbon accounting standards are transforming the pallet rack supply chain. Global supply chain directors are moving from transactional sourcing to engineered structural partnerships.
1. High-Density Shuttle & AS/RS Hybridization
With urban industrial land costs escalating across Europe, North America, and Southeast Asia, conventional selective racking is rapidly being superseded by semi-automated pallet shuttle systems and automated storage and retrieval systems (AS/RS). Procurement teams demand racks manufactured with ultra-strict roll-forming tolerances (±0.5 mm) to prevent carrier shuttle track jam hazards and sensor false positives.
2. Decarbonization & Green Steel Traceability (CBAM)
Under the European Union's Carbon Border Adjustment Mechanism (CBAM) and corporate ESG mandates, tier-1 tier warehouse operators now audit the embedded emissions of structural steel. Chinese manufacturers leveraging electric arc furnace (EAF) processing, continuous zero-VOC electrostatic powder curing lines, and complete mill test certificates (MTC) gain a decisive edge in multinational competitive tenders.
3. Seismic Performance & Finite Element Verification
Recent updates to international building codes (IBC 2024 and Eurocode 3 / EN 15512) enforce heightened dynamic ground acceleration verification. Buyers require certified Finite Element Analysis (FEA) validating baseplate bolt shear, upright column tear-out resistance under heavy seismic spectral loading, and drop-beam accidental dislodgement prevention with minimum 5 kN shear-rated locking pins.
Advanced Cold-Forming, Continuous Punching & Surface Metallurgy
The engineering integrity of industrial pallet racks depends on the metallurgical quality of cold-rolled strip steel, computer-controlled punching accuracy, and state-of-the-art chemical pre-treatment before polymer curing.
CNC Continuous Roll-Forming
Multi-stage 22-station roll-forming lines bend cold-rolled structural steel gradually into complex omega upright profiles. This mitigates microscopic micro-cracking at bend radiuses and maintains high cross-sectional modulus.
Micro-Tolerance Punching
High-speed hydraulic continuous progressive die stations punch tear-drop, diamond, or European butterfly pitch holes at a steady ±0.1 mm spacing accuracy, ensuring true plumb alignment across multi-tier frame installations.
Nanotech Zirconium Pretreatment
Replacing legacy iron-phosphating with zirconium silane nanotechnology cleanses grease and scale down to zero residue, tripling salt-spray resistance (>500 hours ASTM B117) and securing powder adhesion to prevent peeling.
Automated Robotic Beam Welding
Robotic dual-torch MIG welding systems fuse heavy beam connectors to roll-formed box beams with continuous deep-penetration fillets, completely eradicating cold-joint weaknesses and ensuring uniform load distribution.
Guangzhou HEDA Shelves: 25 Years of Precision Storage Engineering
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized metal stamping factory into a globally recognized manufacturer of industrial pallet racking, automated shuttle systems, structural mezzanines, and high-density longspan shelving. Operating out of an expansive 30,000 square meter intelligent manufacturing facility in Guangzhou, China, our team delivers complete end-to-end intralogistics infrastructure for 3PL logistics hubs, pharmaceutical warehouses, cold chain freezers, and industrial distributors worldwide.
-
CE Certified Factory (No. 2435-CPR-8605159): Compliant with EU Construction Products Regulation (CPR) and audited against EN 15512 and EN 15620 structural verification standards.
-
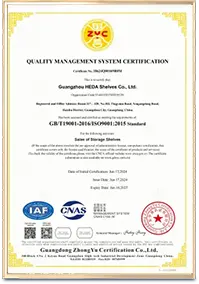
ISO 9001:2015 Quality Management (No. 18624Q00169R0M): Fully implemented across raw coil slit shearing, robotic welding, electrostatic powder baking, and seaworthy bundle packing.
-
Free 24–48h Turnkey CAD & 3D Engineering Layouts: Our structural engineers calculate bay capacities, aisle clearances, and seismic load limits tailored to your specific forklift turning radius.
-
High Production Throughput (30,000 Tonnes/Month): Direct factory-floor control guarantees rapid production turnarounds of 15–25 calendar days, even on large-scale logistics hub projects.
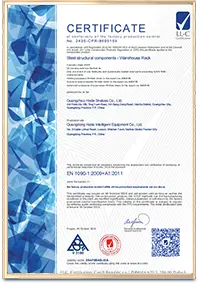 CE Certificate
 ISO 9001:2015
 Test Report
 Compliance
The 10-Step Heavy-Duty Precision Production Flow
Raw Steel Audit
Spectroscopic chemical check & tensile yield testing of prime Q235B/Q355B coils.
Precision Slitting
Automated shearing with burr-free rotary knives to exact millimeter coil widths.
CNC Column Punching
Continuous progressive die punch creating standard 50/75 mm pitch connection slots.
Cold Roll-Forming
22-station roll-forming lines shaping open uprights and closed box beam tubes.
Laser Flying Cut
High-speed synchronized cut-off units maintaining strict ±0.5 mm beam length tolerances.
Surface Polishing
Shot-blasting and mechanical de-scaling to achieve Sa 2.5 cleanliness classification.
Robotic MIG Welding
High-deposition welding of multi-claw connector tabs with deep metallurgical penetration.
9-Stage Pretreatment
Multi-tank degreasing, clean-water rinse, and zirconium silane conversion coating.
Electrostatic Powder
Thermosetting polyester resin application cured at 200°C for high impact endurance.
Seaworthy Packing
Protective bubble wrap, corrugated steel strapping, and labeled bundle sequencing.
Frequently Asked Questions by Industrial Racking Buyers
Direct answers to structural, commercial, and operational questions encountered by logistics developers, engineering consultants, and corporate procurement directors.
How do Chinese racking profiles comply with European EN 15512 and US RMI MH16.1 standards?
Compliance is achieved through rigorous engineering validation rather than nominal steel thickness alone. Under EN 15512:2020 and RMI MH16.1, upright frame columns, beam end connectors, and floor baseplates undergo physical stub-column compression tests, beam connector shear tests, and looseness rotational stiffness testing. HEDA Shelves utilizes certified Q235B and Q355B structural steel, maintaining full traceability through Mill Test Certificates (EN 10204 Type 3.1) and structural calculations stamped for review by your regional building certifier or local rack inspector.
What are the key technical differences between Q235B and Q355B cold-rolled steel?
Q235B exhibits a guaranteed minimum yield strength (Fy) of 235 MPa and ultimate tensile strength of 370–500 MPa, functioning as the standard workhorse for low-to-medium-height pallet racks (up to 7 meters) with standard pallet loads (500–1,500 kg). Q355B provides a minimum yield of 355 MPa (equivalent to European S355JR or American ASTM A572 Grade 50). Q355B is selected for high-bay VNA systems exceeding 9 meters, seismic design categories D/E/F, automated radio shuttle tracks, and heavy-duty structural cantilever columns where higher buckling limits are required.
How does factory-direct procurement from China optimize Total Cost of Ownership (TCO)?
Purchasing directly from Guangzhou Heda Shelves eliminates intermediary distributor margins, which typically add 25% to 45% to project costs. Furthermore, because our in-house engineering team customizes upright steel gauges and beam profiles to your precise load specifications rather than forcing oversized catalogue modules, overall steel tonnage is optimized without compromising safety factors. Our experienced shipping department loads 40-foot high-cube containers (40HQ) with custom nesting cradles, packing 24 to 28 metric tonnes per container to maximize ocean freight density.
What project data is required to generate a complete CAD design and structural quotation?
To provide an engineered proposal within 24–48 hours, our structural team requires: (1) Warehouse architectural drawings (DWG or PDF) showing clear ceiling heights, column grids, fire riser mains, and egress doors; (2) Pallet specifications including width, depth, height, and maximum loaded weight; (3) Forklift fleet details indicating model, maximum lift height, mast collapse height, and right-angle stacking aisle turning radius (Ast); (4) Operating temperature (ambient vs. -25°C cold storage); and (5) Project site location for seismic spectral acceleration determination.
How are heavy-duty racks finished to resist corrosion in cold rooms and chemical environments?
For ambient warehouses, our automated electrostatic lines apply thermosetting epoxy-polyester powder coating (60–90 μm dry film thickness) cured at 200°C, offering exceptional resistance to impact, chipping, and standard humidity. For blast freezers (-30°C) where condensation and thermal cycling cause micro-blistering, or chemical fertilizer plants with high chloride concentrations, we manufacture hot-dip galvanized racking (HDG) per ASTM A123 / ISO 1461, yielding a sacrificial metallurgical zinc alloy layer exceeding 70–85 μm that provides decades of rust-free service life.
What quality control milestones, MTCs, and third-party inspections (SGS/TÜV) are provided?
Quality control is executed at three distinct stages: (1) Inbound coil inspection covering ultrasonic thickness gauging, chemical composition, and yield-point pull tests accompanied by EN 10204 3.1 Mill Test Certificates; (2) In-process geometric dimensional audits checking upright hole pitch alignment, beam weld penetration depth, and powder cure cross-hatch adhesion (ASTM D3359); and (3) Pre-shipment batch validation. We routinely host independent third-party inspection agencies such as SGS, Bureau Veritas, and TÜV Rheinland to issue independent loading and inspection reports prior to final balance dispatch.
What container packing configurations prevent maritime transit damage and warping?
Export logistics for long structural members require specialized stowage engineering. Upright frames are nested horizontally on heavy hardwood or steel dunnage skids with corrugated edge protectors and high-tensile polyester strapping. Beams are bundled in matched pairs with connector tabs shielded by protective sleeves to prevent transit bending. All hardware, baseplates, shims, and safety locking pins are packed in weather-sealed wooden cases with desiccant packs to prevent surface oxidation while traversing equatorial shipping routes.
How does HEDA Shelves support global installation, sign-off, and safety inspections?
Every export project ships with component piece-marked assembly drawings, installation torque specifications for base anchor bolts (M12/M16 wedge anchors), and step-by-step video construction guides. For major projects across Europe, the Middle East, Southeast Asia, and the Americas, HEDA Shelves dispatches senior structural installation supervisors to direct local rigging crews. Following assembly, we supply compliant permanent load safety warning plaques detailing maximum bay and shelf capacities in accordance with EN 15635 and OSHA regulations.
Submit Your Warehouse Project Brief for Turnkey Engineering Review
Connect directly with our senior intralogistics structural engineering department in Guangzhou. Receive a full CAD warehouse layout, 3D render, structural deflection analysis, and direct factory-gate quotation within 24–48 hours.