Precision-Engineered Industrial Storage Systems
Certified, high-load warehouse systems and custom heavy-duty steel shelving configurations supplied direct from our 30,000 m² Guangzhou production facility.
Slim Slide Out Storage Tower Rack Mesh Rolling Organization Serving Cart
Warehouse Storage Factory Strong Load Capacity Adjustable Heavy Duty Cold Rack
Heavy Duty Industrial Shelving Unit 4 Tier Adjustable Boltless Metal Rack
Peterack CE Certified Heavy Duty Selective Pallet Racking System
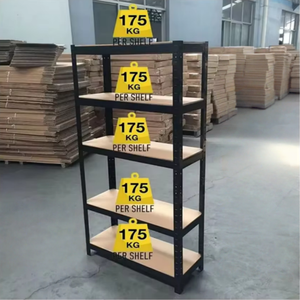
5 Tier Boltless Shelving Heavy Duty Workshop & Garage Storage Shelving
Commercial Wall Shelf with Engineered Drainage Groove & Moisture Channels
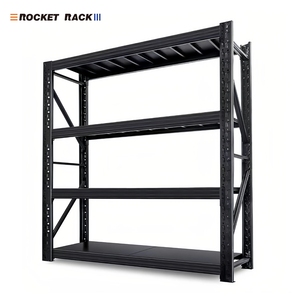
Cold Rolled Steel Medium Duty Corrosion Protection Warehouse Shelving Units
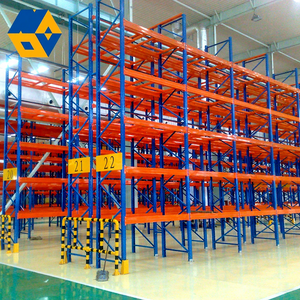
NOVA Industry Automation-Ready Heavy Duty Selective Pallet Racking
Engineering Selection Guide: Pallet Racking Topologies for Modern Fulfillment
Modern distribution centers, cold storage hubs, and third-party logistics (3PL) providers face tightening floor margins and increasing SKU velocities. Selecting an appropriate steel pallet racking topology requires evaluating pallet turnover rates, building clearance thresholds, forklift fleet profiles, and seismic risk factors. As an established China wholesale steel pallet racking manufacturer, our engineering team manufactures structural configurations optimized according to the European EN 15512 standard, the American RMI (Rack Manufacturers Institute) specification, and Australian AS 4084 guidelines.
Selective Pallet Racking
Offers 100% immediate selectivity to every pallet location. Engineered for fast-moving multi-SKU retail and distribution facilities. Compatible with standard counterbalance and reach trucks without dedicated specialized handling equipment.
Drive-In / Drive-Through Systems
Eliminates working aisles to achieve up to 75% volumetric warehouse utilization. Best suited for high-density, low-SKU bulk inventory operating on LIFO (Last-In, First-Out) or FIFO (First-In, First-Out) batch rotation sequences in cold storage.
Radio Shuttle Semi-Automated Racking
An intelligent cart navigates inside deep continuous storage tunnels via radio frequency control. Eliminates forklift transit inside lanes, cutting mast collision damage by over 80% while dramatically shortening pallet retrieval cycles.
Gravity Flow & Push-Back Racking
Utilizes inclined wheel beds or nested gravity carts on structural channel rails. Gravity flow guarantees strict FIFO for dated consumer goods; push-back delivers 2 to 6 deep storage utilizing standard counterbalance trucks with zero aisle intrusion.
Very Narrow Aisle (VNA) High Bay
Reduces aisle clearances down to 1.6 - 1.8 meters, lifting reach heights up to 17 meters with wire or mechanical rail-guided turret trucks. Delivers high volumetric density alongside unrestricted 100% access to individual pallet locations.
Structural Cantilever & Mezzanines
Engineered without front upright obstruction for awkward long-span items such as timber packs, structural tubing, PVC extrusions, and heavy sheet stock, integrating seamless column-supported multi-tier platforms to multiply vertical pick floors.
Technical Benchmark Matrix: Warehouse Storage Topologies
Procurement directors and material handling consultants must evaluate trade-offs between initial capital expenditure, square meter floor utilization, accessibility, and material handling vehicle requirements. The table below outlines technical benchmarks across standard heavy industrial storage models.
| System Architecture | Floor Space Utilization | Pallet Selectivity | Rotation Principle | MHE (Forklift) Compatibility | Target Capital Cost Tier |
|---|---|---|---|---|---|
| Standard Selective Pallet Racking | 40% - 50% | 100% (Instantaneous) | FIFO or LIFO | Standard Counterbalance, Reach Truck | Economic (Baseline) |
| Double-Deep Racking | 55% - 65% | 50% Direct Access | LIFO | Deep-Reach Pantograph Truck | Low - Medium |
| Drive-In Storage System | 70% - 80% | 20% - 30% (Lane level) | Strict LIFO | Narrow Counterbalance / Reach | Moderate |
| Push-Back (Cart/Roller) | 65% - 75% | Lane Facing (2-6 Deep) | LIFO | Standard Reach / Counterbalance | Moderate - High |
| Radio Shuttle Automation | 80% - 88% | Channel Selective | FIFO & LIFO Programmed | Standard Forklift + Automated Carrier | Advanced Investment |
| Pallet Live Gravity Flow | 75% - 85% | Lane Face Selectivity | Automatic Dynamic FIFO | Separate Loading & Retrieval Trucks | Advanced Engineering |
| VNA (Very Narrow Aisle) | 60% - 70% | 100% Direct Access | FIFO or LIFO | Wire-Guided Turret / Man-Up Truck | Medium (Floor critical) |
Future Procurement Trends in Industrial Storage & Material Handling (2025–2030)
Procuring warehouse racking from Chinese manufacturing leaders has shifted from a pure cost-per-ton transaction to a strategic engineering partnership. High-throughput distribution facilities require equipment that accommodates automation, withstands environmental stress, and minimizes total lifecycle costs.
Automation & AMR Readiness
Traditional racking is being upgraded with high-tolerance floor guide angles, LiDAR reflective targets, and rack-mounted positioning tags to support Autonomous Mobile Robots (AMRs) and automated shuttle carriers operating without direct operator intervention.
Cold Chain Surge & Low-Temp Alloys
The global boom in fresh groceries and pharmaceutical cold supply chains requires specialized micro-alloyed structural steels that resist low-temperature embrittlement at -25°C to -40°C, combined with moisture-shedding drainage channels and antimicrobial finishes.
Sustainability & Closed-Loop Coatings
International environmental targets are accelerating the adoption of lead-free, TGIC-free thermoset epoxy-polyester powder formulations. Electrostatic recovery booths ensure 98% powder reuse, cutting emissions while delivering over 500 hours of ASTM B117 salt spray resistance.
Factory Direct Advantage: Guangzhou Heda Shelves Co., Ltd.
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized metal fabrication workshop into an international manufacturer of heavy-duty industrial racking and structural steel mezzanine floors. Our 30,000 m² modern manufacturing plant houses automated continuous roll-forming lines, automated laser-cutting cells, and robotic welding lines.
Operating with over 300 experienced technical specialists, our monthly production capacity reaches 30,000 metric tons. We serve international distributors, material handling contractors, and EPC logistics builders in more than 120 countries. Our production workflows strictly follow certified quality systems, ensuring structural safety and batch-to-batch consistency across complex logistics projects.
CE Certificate No. 2435-CPR-8605159
Full European Construction Products Regulation (CPR) compliance for load-bearing steel components. Structural calculation dossiers comply with EN 15512 static load guidelines and EN 15620 tolerance requirements.
ISO 9001:2015 No. 18624Q00169R0M
Certified operational quality management spanning mill cert verification, spectrometer testing of raw cold coils, gauge dimension tolerance verification, and cross-hatch paint adhesion testing.
Compliant RoHS & Safe Chemistry
All finished powder coatings comply with European chemical restrictions (RoHS and REACH). Pre-treatment utilizes environmentally conscious silane or eco-friendly zinc phosphate technology for strong bonding without toxic sludge.
Our 10-Stage Precision Fabrication Workflow
Every beam, upright column, base plate, and brace is manufactured through our integrated in-house quality cycle:
Coil Inspection
Spectrometer analysis of Q235B/Q355B coils for yield, tensile strength, and elongation.
CNC Slitting
High-precision uncoiling and continuous slitting to accurate sheet widths.
Auto Punching
Continuous CNC progression punching of 50mm / 75mm pitch diamond and teardrop patterns.
Roll Forming
Cold continuous roll forming across up to 24 roller passes for precise profile geometry.
Laser Cutting
Precision sizing of box-beams, step beams, and structural connection components.
Robotic Welding
Automated multi-axis welding of beam connectors to beam sections, minimizing human error.
Pickling & Rinse
Multi-stage immersion cleaning, degreasing, and acid pickling to eliminate mill scale.
Phosphating
Chemical surface conversion creating a uniform crystalline base for paint adhesion.
Powder Coating
Electrostatic spray application cured at 200°C for a durable, scratch-resistant finish.
Export Packing
Padded timber dunnage, protective edge boards, and steel strapping for ocean freight protection.
Frequently Asked Questions: Global Industrial Procurement
Direct technical answers addressing engineering standards, container packing, seismic compliance, and international warranties.
What steel grades are used, and how do they impact maximum allowable load capacities?
Can your engineering team adapt designs for standard Euro pallets (EUR/EPAL) and US GMA standards?
How do you guarantee corrosion protection in high-humidity or sub-zero blast freezer conditions?
What calculations and engineering documentation accompany European and North American projects?
How are high-volume racking shipments packed to prevent transit abrasion across long sea voyages?
Can you support OEM / ODM private labeling for material handling distributors and installers?
What is the standard production lead time and typical ocean transit timeline to major ports?
Request an Engineered Layout & Wholesale Factory Quotation
Send our senior engineering team your warehouse floor layout (CAD/PDF), clear internal ceiling height, pallet dimensions, and forklift specifications. We will return an optimized bay layout, load tables, and factory-direct pricing within 24 hours.