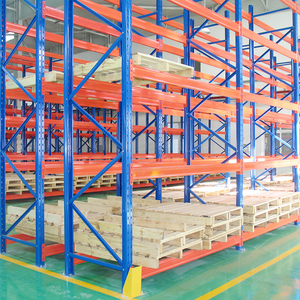
Heavy Duty Industrial Steel Stacking Pallet Storage Rack
High load-bearing modular beams with custom shelf layers, designed for heavy industrial distribution hubs.
Custom OEM/ODM configurations manufactured to EN 15512, ISO 9001:2015, and CE factory-direct specifications.
High load-bearing modular beams with custom shelf layers, designed for heavy industrial distribution hubs.
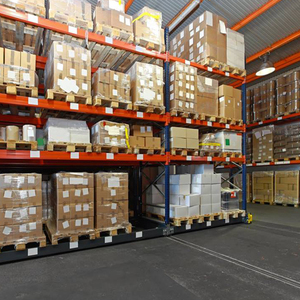
Certified multi-ton mobile chassis, rated for 1300KG–1500KG+ bay capacity, consolidating floor footprints.
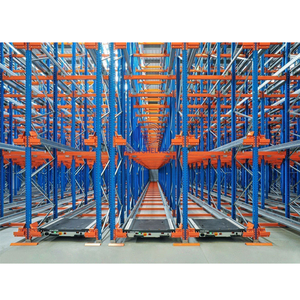
Ultra-high density multi-directional robotic transport supporting both FIFO & LIFO logic in sub-zero freezers.
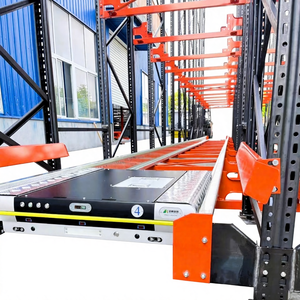
Radio-guided shuttle carrier rails ensuring high-speed automated cycle runs with zero fork impact risk inside lanes.
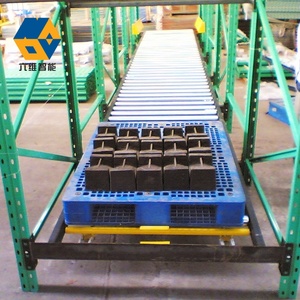
Engineered incline roller beds with dynamic centrifugal speed controllers for deterministic inventory rotation.
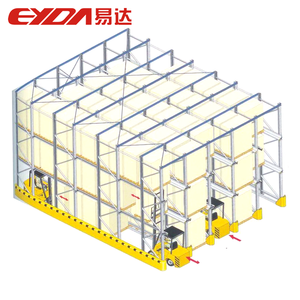
Continuous lane drive-through configuration enabling true FIFO handling for uniform bulk commodities.
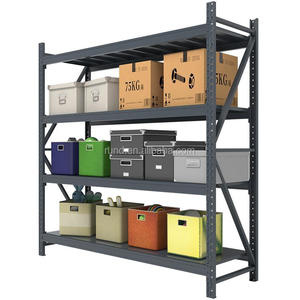
Interlocking node floor system with fall-free retainers and free CAD/3D optimization for secondary storage tiers.
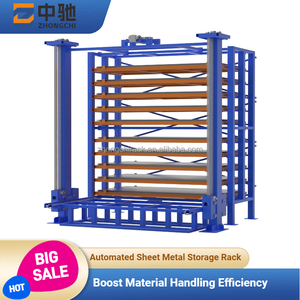
Intelligent automated retrieval with multi-layer high load capacity, anti-corrosion finishes, and cassette docks.
A technical analysis of mechanical gravity flow, radio shuttle lanes, and high-density warehouse efficiency.
In modern industrial logistics, optimizing throughput velocity while mitigating SKU obsolescence is paramount. Implementing First-In, First-Out (FIFO) pallet racking represents the operational gold standard for cold chain facilities, pharmaceutical distribution centers, and fast-moving consumer goods (FMCG) operations. Unlike static LIFO (Last-In, First-Out) drive-in systems, an engineered FIFO infrastructure ensures physical stock rotation occurs systematically without operational intervention, reducing handling touches and spoilage costs to near zero.
From an engineering perspective, mechanical FIFO systems leverage gravity flow beds set at an incline of 2.5% to 3.5%. Heavy pallets travel along steel roller tracks modulated by speed controllers—centrifugal brake rollers installed at designated intervals. These mechanical dampers prevent runaway acceleration by maintaining pallet momentum below 0.3 m/s, irrespective of whether the unit load weighs 400 kg or 1,500 kg. At the discharge end, heavy-duty separator mechanisms decouple the lead pallet from subsequent line pressure, allowing forklifts to extract pallets cleanly without dangerous line drag or structural buckling.
As warehouse heights expand beyond 12 meters to maximize cubic utilization, semi-automated radio shuttle and 4-way ASRS systems bridge the gap between mechanical gravity racks and full automation. Instead of continuous roller tracks, deep storage channels are fitted with high-precision cold-formed steel guide rails. Autonomous battery-powered shuttles glide underneath pallet positions, lifting and transferring loads from the rear replenishment aisle to the front retrieval face. This architecture decouples transport speed from gravity friction, completely eliminates forklift transit inside racking lanes, and delivers the ultimate cubic storage density available in modern warehouse engineering.
Founded in 2001, our 30,000 m² factory operates automated roll-forming, continuous punching, and robot-welded lines producing up to 30,000 tonnes of structural racking every month.
Independently audited and certified under CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 No. 18624Q00169R0M, and aligned with EN 15512 structural calculation frameworks.
Our in-house application engineers prepare full warehouse layout schematics, static stress analysis, and forklift aisle clearances before fabrication, ensuring turnkey site execution.
How supply chain dynamics, decarbonization, and smart automation are reshaping warehouse racking specifications.
Procurement teams are shifting away from monolithic manual racking toward hybrid topologies. High-throughput distribution centers increasingly integrate FIFO gravity lanes and radio shuttles with automated guided vehicles (AGVs) and stacker cranes. Specifying standardized upright tolerances and high-tensile upright punchings ensures future-proof retrofit capability without tearing down civil infrastructure.
With industrial refrigeration energy tariffs surging across Europe and North America, every cubic meter of chilled volume must be monetized. Procurement trends show a decisive migration from wide-aisle selective systems to 4-way deep shuttle lanes. Concentrating thermal mass within compact racking grids lowers HVAC cycle demands by up to 35% per stored pallet position.
International buyers require customized steel grade compositions (Q235B / Q355B equivalent to S235JR / S355JR) and electrostatic powder coatings resistant to thermal shock down to -30°C. Standard off-the-shelf distributor racks fail to address irregular pallet footprints (EUR 1200x800mm, Industrial 1200x1000mm, or specialized beverage skids), making direct factory OEM partnership the preferred sourcing model.
Technical, logistical, and structural clarifications for project managers, engineers, and supply chain directors.
Partner directly with an established ISO 9001 and CE certified manufacturer. Connect with our engineering department today for custom layout planning, static calculations, and factory-direct OEM pricing.
Inquire Now