Direct OEM Teardrop & Industrial Storage Solutions
Manufactured under ISO 9001:2015 and CE quality assurance. Select a standardized framework or collaborate with our engineering team for custom gauge, beam profile, and seismic load parameters.
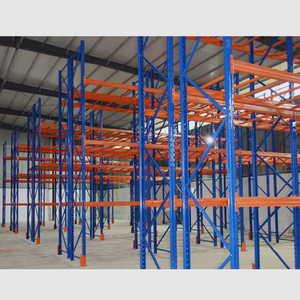
Double Deep High-Density Teardrop Pallet Rack
Increases warehouse footprint utilization by up to 60% compared to selective racking by eliminating secondary operational access aisles.
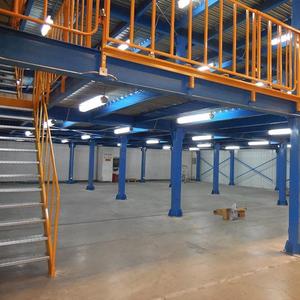
Industrial Warehouse Steel Mezzanine Platform
Multi-tier rack-supported structure delivering dual functional utilities: floor-level pallet storage beneath upper picking and assembly platforms.
5-Layer Cold Rolled Bolt-Free Storage Shelving
Anti-corrosion powder-coated modular shelving engineered for manual picking environments, tool rooms, and rapid assembly lines.
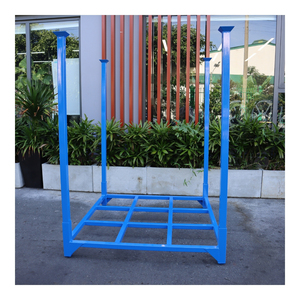
Foldable Stackable Heavy-Duty Steel Pallet
Collapsible tubular steel framework built for rugged reverse logistics, automated conveyor transfer, and dynamic multi-tier block stacking.
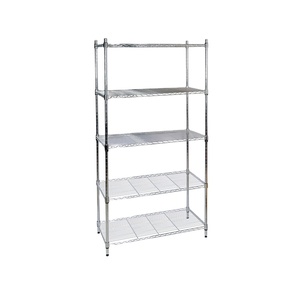
5-Tier Metal Wire Narrow Aisle Shelving
Maximizes vertical cube utilization within restricted corridors; open wire mesh guarantees code compliance for ESFR in-rack sprinkler penetration.
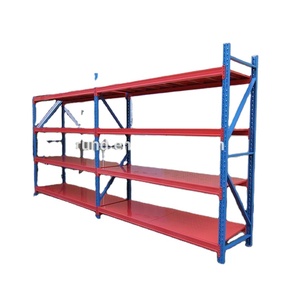
Portable Modular Metal Stacking Rack (Manurack)
Flexible bulk-storage framework allowing instant warehouse rearrangement without permanent anchor drilling; ideal for seasonal cargo overflow.
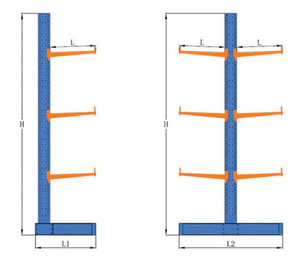
Heavy-Duty Adjustable Cantilever Arm Racking
Engineered with unobstructed horizontal bay openings for continuous timber, extruded aluminum profiles, steel rebar, and tubular material storage.
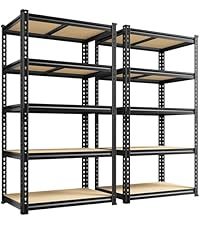
5-Layer Industrial Boltless Rivet Storage Rack
Quick mallet-lock keyhole connection with heavy-gauge roll-formed upright posts and durable steel/wire decking for industrial fulfillment facilities.
1. Architectural Engineering & Metallurgy of Teardrop Pallet Racking
The teardrop hole pattern is the uncontested standard of the North American logistics sector and an increasingly prominent system across global material handling operations. Its popularity originates from the patented inverted keyhole punch geometry, which produces a natural gravity-assisted wedge action when the step beam's conical connector pins engage the upright column. As external vertical pallet loading increases, the mechanical interlock tightens dynamically, transferring axial forces down the column without inducing localized torque or beam displacement.
From a metallurgical perspective, our custom OEM manufacturing protocol employs prime certified high-strength cold-rolled structural steel coils (grades Q235B and Q355B, corresponding strictly to ASTM A1011 and A36 standards). High yield strength (Reh ≥ 355 MPa) and minimal elongation under tensile fatigue guarantee that upright frame columns sustain high dynamic impacts from Class I, II, and IV forklifts without catastrophic buckling failure. The uprights undergo progressive continuous roll-forming across 24 CNC roller stages, eliminating localized material micro-fissuring and preserving cross-sectional geometric integrity along the entire column length.
Comparative Metallurgy: Structural Integrity vs. Rolled Form Tolerances
| Structural Parameter | HEDA Custom OEM Teardrop Standard | Generic Market Competitor Standard | Compliance Reference / Test Protocol |
|---|---|---|---|
| Steel Grade & Yield Strength | Certified Q235B / Q355B (Yield ≥ 235 - 355 MPa) | Uncertified Commercial Grades (≤ 195 MPa) | ASTM A1011 / EN 10025-2 Mill Verification |
| Upright Hole Precision Pitch | CNC Punched 50.8 mm (2.0 Inch) True Pitch ±0.1 mm | Mechanical Stamping with ±0.8 mm Drift | ANSI MH16.1 Section 5.3 Beam Fit Testing |
| Pre-Treatment Protocol | 9-Stage Immersion Pickling & Zirconium Phosphating | Simple Wipe Down or Basic 3-Stage Wash | ASTM B117 500-Hour Salt Spray Resistance |
| Electrostatic Powder Coating | 60 - 90 μm TGIC-Free Thermosetting Polyester | 35 - 45 μm Standard Industrial Paint | ISO 2409 Cross-Hatch Adhesion Class 0 |
| Safety Locking Mechanism | Integral Auto-Engage Spring Steel Safety Pins | Manual Detached Drop Pins (High Loss Rate) | RMI Uplift Requirement (≥ 1,000 lbs Force) |
Precision punching is performed prior to the final cold profile bends. This sequence ensures the center-of-gravity alignment between the punch centerline and the upright's shear axis does not drift. By standardizing the teardrop hole orientation at an exact 2-inch pitch increment, our racks offer universal compatibility with major legacy teardrop brands, enabling distributors and project contractors to supply cross-compatible aftermarket components without spatial or load mismatches.
2. Global Teardrop Racking Procurement Trends (2025–2030)
Procurement directors and 3PL facility managers are re-evaluating intralogistics infrastructure purchasing strategies. Rising industrial square-foot leasing rates across key global logistics corridors require maximizing clear warehouse storage heights (cube utilization) rather than expanding facility footprints. This shift has triggered noticeable procurement transitions:
A. Migration Toward Hybrid Automated Warehouses (ASRS & Shuttle-Ready Bays)
Static manual warehousing is evolving toward semi-automated topologies. Modern teardrop racking procurement contracts increasingly specify reinforced lower frame tiers and customized heavy-duty baseplates designed to accommodate autonomous mobile robots (AMRs) and automated guide rails. Beam spans must retain strict deflection limits under continuous service (≤ L/180 according to RMI specifications, or ≤ L/200 under European EN 15512 guidelines) to prevent pallet hang-ups during automated shuttle retrieval cycles.
B. Rigorous ESG Audits and Powder Coating Sustainability
Environmental, Social, and Governance (ESG) guidelines increasingly influence Tier-1 enterprise procurement. Suppliers must eliminate heavy metals, lead additives, and volatile organic compounds (VOCs) from finish coatings. In response, our manufacturing utilizes 100% recyclable, TGIC-free thermosetting polyester powder coatings baked in gas-fired curing ovens at 200°C. This process delivers high abrasion, chemical, and chipping resistance while lowering embodied carbon metrics for green building validations (such as LEED or BREEAM).
C. Seismic Resilience and Regional Building Code Adaptations
Seismic events present substantial financial and life-safety hazards in logistics hubs. Procurement specifications now routinely demand site-specific engineered baseplate anchor calculations based on International Building Code (IBC) seismic design categories (C through F). Our engineering team employs finite element modeling (FEM) to tailor upright column web thicknesses, diagonal brace angles, and concrete wedge anchor dimensions to match peak ground acceleration (PGA) metrics across destination markets.
3. Enterprise Manufacturing Strengths: Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from an industrial racking workshop into a global enterprise exporting to over 120 countries. We provide end-to-end integration across warehouse planning, CAD engineering, in-house roll forming, and export delivery. We operate under registered CE certification (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 quality management standards (Certificate No. 18624Q00169R0M), offering commercial distributors and end-users audited transparency and verified load capacities.
Full OEM/ODM Private Labeling
We provide comprehensive branding, custom RAL powder-coat color formulation, laser-etched bay capacity placards, and export palletization tailored for regional distribution partners.
Complimentary 3D & CAD Layouts
Send your warehouse architectural drawings (DWG/PDF), and our engineering team provides structural bay elevations, pallet capacity simulations, and seismic calculations within 24–48 hours.
Rigorous 10-Stage Production QC
From raw metallurgical optical emission spectrometry to post-cure salt-spray evaluation, our production lines ensure tight dimensional tolerances and reliable weld penetration across every component.
Step-by-Step Quality Governance & Manufacturing Workflow
Every teardrop pallet rack produced in our 30,000 m² facility follows a structured 10-step manufacturing protocol. Raw coil stock is verified for tensile and chemical consistency before high-speed CNC punching and roll forming. Beam connector end-plates are assembled via multi-axis robotic welders to prevent weld porosity and uneven heat dissipation. Components then move through automated cleaning stages (degreasing, acid pickling, rinse, phosphating, passivation) before entering electrostatic powder spray booths and curing ovens.
4. Structural Mechanics: Teardrop Interlock vs. European Keyhole & Slotted Racks
Engineers specifying storage equipment across international borders must navigate differing frame connection geometries. Understanding the structural behavior of the teardrop configuration compared to alternative connection designs informs proper system selection.
| Evaluation Parameter | Teardrop Racking (North American Standard) | Hook-and-Slot Racking (European Standard) | Bolt-Together Structural Racking |
|---|---|---|---|
| Assembly Speed & Labor Cost | Fastest Tool-less slip-in locking | Moderate: Requires mallet and safety clip alignment | Slow: High labor overhead; torqued bolt validation |
| Beam Dislodgement Protection | Automatic spring-lock pin resists vertical upward lift | Drop-in spring clips (prone to accidental misplacement) | Bolted shear pins provide high resistance |
| Component Interchangeability | High Universally cross-compatible across brands | Low: Proprietary hook tabs differ across suppliers | Low: Hole spacing and hardware vary widely |
| Impact Resistance (Forklift Collision) | Moderate to High (enhanced via column wrap protectors) | Moderate: Prone to localized tab deformation | Highest Thick structural channel sections |
| Total Cost of Ownership (TCO) | Optimized Balanced steel efficiency & ease of setup | Moderate to High due to regional supplier markups | High steel consumption and prolonged assembly hours |
The self-locking taper pin design of the teardrop connector distributes vertical beam deflection into a clamping force that grips the face of the column. This dynamic reduces bending stress at the connection tabs under heavy loading. When outfitted with wire decking, front-to-back crossbar pallet supports, and structural frame guards, teardrop systems provide an adaptable, safety-compliant foundation for fast-paced fulfillment operations.
5. Frequently Asked Procurement & Engineering Questions (FAQ)
Are your OEM teardrop racks cross-compatible with other major North American brands?
Yes. Our teardrop upright punch profile and step-beam end connectors conform to industry-standard 2.0-inch (50.8 mm) center-to-center pitch increments with matching teardrop cutout dimensions. They integrate seamlessly with standard legacy systems, allowing straightforward expansion of your existing distribution bays without specialized modification.
What engineering documentation and load data do you supply for permitting?
Every commercial quote and project shipment includes comprehensive engineering documentation. This comprises CAD layout plans, bay elevation load capacity tables, steel mill material test certificates (MTCs), CE Declaration of Performance (Certificate No. 2435-CPR-8605159), and ISO 9001:2015 certifications. On project request, our structural engineers deliver certified calculations referencing ANSI MH16.1, RMI, and EN 15512 standards to facilitate local building permit reviews.
What production lead time and global shipping schedules can we anticipate?
Standard fabrication lead times average 15 to 25 days depending on overall container volume and custom RAL powder color requirements. Components are packed with protective corner wrapping, strapped on steel dunnage, and loaded into 40ft High Cube containers to maximize sea freight volume and reduce maritime shipping expenses. Transit times from our Guangzhou loading terminal to West Coast North American ports average 14–18 days, East Coast destinations 25–30 days, and major European deepwater ports 28–35 days.
Can you manufacture heavier steel gauges or reinforced frame profiles for seismic zones?
Yes. As a direct OEM manufacturer, we roll-form upright column gauges ranging from 16-gauge (1.5 mm) up to 12-gauge (2.75 mm) structural thicknesses, coupled with oversized seismic baseplates pre-punched for heavy-duty concrete anchor studs. We also engineer structural column reinforcements, such as welded front column inserts or heavy-gauge bullnose protectors, to handle high impact risk at aisle corners.
How can overseas distributors order private label racking under their own brand?
We provide complete OEM/ODM manufacturing partnerships. We apply your exact corporate RAL powder coat colors, produce branded load placards with your company logo and capacity ratings, customize packaging sleeves, and supply blind-drop shipping documentation directly to your project job sites.
Request an Engineered Layout & Factory-Direct OEM Quotation
Send your warehouse floor plan, ceiling clear heights, and pallet specifications. Our engineers will return a complete 2D/3D layout, load-capacity matrix, and competitive factory-direct proposal within 24 hours.