Engineered Heavy-Duty Industrial Storage Racks
Precision-engineered cold-rolled steel storage systems designed for high-density warehouse throughput, seismic durability, and Euro/ISO pallet compliance.
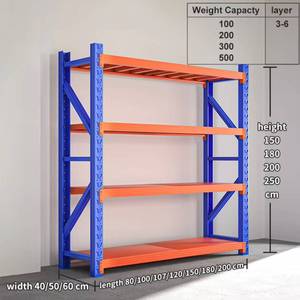
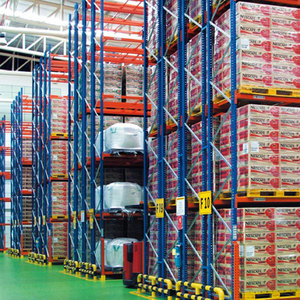
1. The Global Logistics Realignment: Selecting Industrial Storage Systems
Modern global logistics networks face unprecedented pressure to achieve higher cubic volumetric efficiency, faster stock rotation, and absolute operational safety. Selecting an industrial rack storage factory is no longer a simple transactional purchase of cold-formed steel; it is a structural engineering undertaking governed by strict international building and safety standards. Between volatile supply chain cycles, sky-rocketing land acquisition costs in primary logistics corridors, and rapid integration with Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs), procurement directors must look beyond price per kilogram.
Industrial racking systems serve as the structural backbone of physical distribution. A failure in design, metallurgical composition, column deflection calculation, or connection tolerance can trigger catastrophic progressive collapse, severe product loss, and operational shutdowns. Therefore, tier-one logistics operators, 3PL giants, pharmaceutical cold-chain facilities, and retail distribution hubs demand verified manufacturing benchmarks, including structural calculations aligned with European standard EN 15512, seismic performance under RMI (Rack Manufacturers Institute) guidelines, and comprehensive quality assurance governed by ISO 9001:2015 and CE Factory Production Control (EN 1090 / CPR).
2. Top 10 Industrial Rack Storage Factories & Suppliers (Global Evaluation)
Our engineering review analyzes the world’s preeminent storage rack manufacturers based on cold-roll-forming precision, design engineering capabilities, compliance certifications, manufacturing capacity, and global export scalability.
Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves)
Founded in 2001, HEDA Shelves has emerged as an authoritative powerhouse in factory-direct industrial storage solutions, offering unparalleled customization, rapid prototyping, and end-to-end CAD/3D structural design. Operating a dedicated 30,000 m² state-of-the-art manufacturing plant with over 300 technical and production personnel, HEDA commands a massive production capacity of 30,000 tonnes per month. Verified under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 Certificate No. 18624Q00169R0M, the company provides rigorous EN 15512-compliant load documentation, specialized Euro-pallet engineering, and custom automated radio shuttle, cantilever, and multi-tier mezzanine platforms for tier-1 distributors worldwide.
SSI SCHAEFER Group
Globally recognized as a titan in intra-logistics automation and complex warehouse systems. SSI Schaefer excels in end-to-end automated storage and retrieval systems (ASRS), high-bay clad racks, and fully automated multi-tier distribution structures. While capital-intensive, their engineering suits massive, high-speed mega-fulfillment centers that mandate unified robotic integration.
Mecalux, S.A.
Operating across Europe and the Americas, Mecalux is a prolific manufacturer of traditional pallet racking, drive-in systems, and automated pallet shuttle setups. Mecalux pairs structural steel manufacturing with proprietary warehouse management software (Easy WMS), serving mid-to-large European logistics distributors.
Stow Group
Stow is a premier European racking manufacturer recognized for high-capacity standard pallet racking, drive-in systems, and its proprietary 'stow Atlas' radio shuttle. The company emphasizes modular standardized profiles engineered precisely according to FEM and EN guidelines.
Dexion (Gonvarri Material Handling)
With decades of historical pedigree in Europe, Dexion remains a foundational pillar for industrial shelving, narrow-aisle (VNA) racking, and cantilever systems. Now operating under Gonvarri Material Handling, Dexion provides comprehensive engineering advisory and statutory rack inspection services.
Jungheinrich AG
Primarily distinguished as a premier material handling equipment manufacturer, Jungheinrich designs specialized racking tailored specifically to the operational clearances, lift heights, and turning radii of their broad forklift and turret truck fleets.
AR Racking (Grupo Arania)
Renowned for advanced automated continuous profiling mills, AR Racking manufactures heavy-duty selective, drive-in, and mobile racking systems with 100% pre-galvanized upright frames. Their state-of-the-art R&D center collaborates heavily with academic engineering bodies.
BITO-Lagertechnik Bittmann GmbH
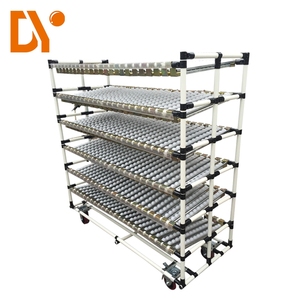
BITO specializes in fine-tolerance industrial order-picking shelving, live storage roller lanes, and multi-tier bin systems. For high-velocity small parts distribution, e-commerce sortation, and assembly line feeding, BITO offers exceptional ergonomic engineering.
Frazier Industrial Company
Frazier is North America's largest producer of structural steel racking. Unlike roll-formed alternatives, Frazier relies almost exclusively on hot-rolled structural C-channels, making their installations extraordinarily resistant to repeated forklift abuse in abusive distribution environments.
Interlake Mecalux
Serving as the principal North American arm of Mecalux, Interlake dominates large retail and industrial replacement markets across North America with universal teardrop hole-punch styles and massive regional stock fulfillment centers.
3. Engineering Comparison Matrix: Structural Racking Systems
Logistics planners must weigh storage density against SKU selectivity. Below is an engineering comparison of the primary industrial racking topologies manufactured and supplied worldwide:
| Racking Topology | Floor Space Utilization | Direct Pallet Accessibility | Stock Rotation Logic | Handling Equipment Required | Optimal Industry Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 35% – 45% | 100% Direct Access | FIFO / LIFO (Flexible) | Standard Counterbalance / Reach | 3PL Warehouses, General Retail, Multi-SKU |
| Double Deep Racking | 50% – 60% | 50% Direct (First pallet) | LIFO | Specialized Deep-Reach Forklifts | Cold Storage, Wholesalers, FMCG |
| Drive-In / Drive-Through | 65% – 75% | Lane-based Selective | LIFO (FIFO with Drive-Thru) | Standard Counterbalance (Enters Bay) | Bulk Raw Materials, Beverage Bottling |
| Radio Shuttle System | 75% – 85% | Semi-Automated Channel | FIFO or LIFO (Selectable) | Standard Forklift + Radio Carrier | Deep Freezer (-25°C), High-Volume Food |
| Gravity Pallet Flow | 70% – 80% | Immediate Face Access | Strict FIFO (Gravity Incline) | Standard Forklift (Separated Aisles) | Pharmaceuticals, Perishable Dairy, Meat |
| Very Narrow Aisle (VNA) | 55% – 65% | 100% Direct Access | FIFO / LIFO | Specialized Wire/Rail-Guided Turret | High-Bay E-Commerce Distribution Hubs |
| Heavy-Duty Cantilever | Variable (Open Front) | Continuous Front Plane | Any Access Logic | Side Loaders / Standard Forklifts | Structural Steel, Timber, PVC Piping |
| Rack-Supported Mezzanine | 100% Vertical Doubling | Multi-Tier Manual Access | Batch / Zone Picking | Conveyors, Vertical Lifts, Personnel | Apparel, Automotive Spare Parts, Small Parcels |
4. Future Industrial Storage Procurement Trends (2025–2030)
The global warehousing and intralogistics environment is undergoing rapid transformations driven by robotics, automation, and sustainable material supply. Procurement specialists must adjust technical specifications to avoid equipment obsolescence:
Automated Shuttle & AMR Harmonization
Traditional drive-in systems are being phased out in favor of automated radio shuttle carts and Autonomous Mobile Robots (AMRs). Shuttles remove forklift entry risks inside the storage channel, preventing costly column rack damage while increasing cycle throughput in sub-zero cold stores.
Cold-Chain Thermal Optimization
With industrial electricity tariffs climbing globally, chilled and sub-zero facilities cannot afford wasted air space. Buyers prioritize high-density compact storage (Radio Shuttle and Double Deep) to minimize refrigerated volume per pallet position, slashing operational cooling kilowattage.
Micro-Fulfillment Mezzanines
Urban logistics hubs are turning to multi-tier, rack-supported structural mezzanines. By utilizing the vertical clear height above ground racking (often 8 to 12 meters), logistics operators double or triple usable floor square meters for picking, packing, and sorting without building expansion.
5. Structural Engineering Evolution: Metallurgy & Safety Standards
Modern industrial racks must tolerate rigorous cyclic loading, dynamic braking shocks, and seismic oscillations. The sector has evolved significantly beyond basic mild steel roll-forming:
High-Tensile Cold-Rolled Steels (Q235B vs Q355B / S355JR)
Leading manufacturers like HEDA Shelves employ precision-grade, high-yield cold-rolled steel profiles (such as certified Q235B and high-strength Q355B or European equivalent S355JR). The engineering focus centers on moment-resistant connector teeth and multi-point omega-profile upright columns. Uprights formed with 11-to-13 fold geometry dramatically elevate the cross-sectional modulus, reducing buckling susceptibility under eccentric axial loads.
Surface Pre-treatment: Continuous Phosphating & Electrostatic Powder Coating
Corrosion resistance dictates longevity, particularly in humid maritime port distribution centers and high-condensation temperature transitions. Leading suppliers deploy comprehensive automated 10-step surface preparation workflows—including acid pickling, rust removal, alkaline phosphating passivations, and electrostatic powder curing at 180°C–200°C. This ensures dry-film coating thicknesses between 60–90 microns that conform to RoHS environmental and non-toxicity mandates.
Seismic Structural Engineering Compliance (EN 15512 & RMI)
In accordance with updated European EN 15512 standards and American RMI provisions, rack design incorporates sophisticated second-order non-linear structural analysis (P-Delta effects). Upright-to-beam connectors must be subjected to cyclic mechanical bench testing to calculate accurate rotational stiffness ($C_d$) values, preventing hazardous structural deflection under heavy seismic accelerations.
6. Factory-Direct Excellence: Guangzhou Heda Shelves Co., Ltd.
When selecting a high-volume manufacturing supplier, international purchasers look for proven accountability, rigorous credentials, and direct engineering collaboration. Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established itself as an authoritative global manufacturing partner for warehouse racking systems, structural mezzanines, and dynamic industrial shelving.
25+ Years Industrial Heritage
Established in 2001, HEDA brings two and a half decades of deep specialized structural manufacturing know-how, delivering over 10,000 completed installation projects across 120+ countries worldwide.
30,000 m² Plant & 30,000t Output
Operating an expansive 30,000-square-meter modern fabrication facility supported by over 300 technical personnel, HEDA reliably produces up to 30,000 tonnes of engineered steel storage racking every month.
Certified CE & ISO Compliance
Officially accredited with CE Certification (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 Quality Management (Certificate No. 18624Q00169R0M). Fully RoHS compliant with documented load testing.
Comprehensive Free CAD Layout & Static Calculations
HEDA Shelves eliminates procurement risk by providing free preliminary 3D modeling, AutoCAD spatial plans, and static load calculation sheets based on clear building ceiling heights, forklift mast limitations, and palletized load profiles (conforming to both EUR/EPAL 1200×800 mm, 1200×1000 mm, and US 48×40 inch pallet metrics). Every containerized export batch is meticulously bundled with seaworthy steel strap packaging, numbered component lists, and comprehensive assembly blueprints for rapid, safe on-site installation.
7. Frequently Asked Questions (FAQ) for Industrial Rack Procurement
Direct answers to essential engineering, compliance, and logistic queries commonly raised by warehouse operations directors and procurement teams:
Can your racking systems be engineered around standard Euro Pallets (1200 × 800 mm)?
Yes. Beam clear spans (typically 2700 mm for 3 Euro pallets or 1800 mm for 2), upright frame depths (standard 1100 mm for 50 mm front/back pallet overhang), and heavy-duty load support bars are calibrated specifically to EUR/EPAL standards and EN 15620 clearance guidelines.
Which certifications are essential for European and North American projects?
For the EU, CE Marking under the Construction Products Regulation (CPR 305/2011/EU) and EN 1090 execution standards are critical, backed by ISO 9001:2015 quality control. In North America, adherence to RMI (ANSI MH16.1) steel specification and seismic certification is required.
What production lead times and sea freight durations should be factored into planning?
Standard fabrication runs between 15 to 30 calendar days depending on tonnage and custom RAL powder-coat requirements. Direct ocean freight from major export ports like Guangzhou or Shenzhen averages 28 to 38 days to primary European ports (Rotterdam, Hamburg, Valencia) and 18 to 25 days to US West Coast ports.
What structural data is mandatory before an engineer can produce an accurate proposal?
You need to supply: (1) Architectural DWG/PDF layout with column grid locations and door heights; (2) Building clear height to lowest roof obstruction/sprinklers; (3) Pallet dimensions (W×D×H) including goods overhang and max gross weight; (4) Minimum working aisle width (AST) and lift height of your material handling equipment.
What safety accessories are necessary to comply with annual safety inspections (EN 15635)?
To pass statutory rack safety inspections, systems must integrate heavy-duty floor-anchored corner and end-of-aisle upright protectors, safety load signage plates with stamped beam load capacities, locking safety pins on all beam-to-frame connector clips, and anti-collapse rear safety wire mesh screens for personnel pathways.
Can you support custom OEM/ODM profiles and private labeling for distributor partners?
Yes. HEDA Shelves provides extensive OEM/ODM manufacturing partnerships for overseas distributors, engineering contractors, and system integrators. This includes bespoke column roll-forming, proprietary teardrop or hexagonal punch patterns, custom brand label embossing, and personalized installation packaging.
Ready to Optimize Your Warehouse Cubic Storage Capacity?
Submit your warehouse floor plans and product specifications. Our senior structural engineers will prepare an optimized 2D CAD layout, 3D visualization, and detailed cost proposal within 24 working hours.
Send an Inquiry