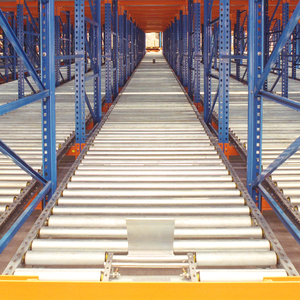
Dynamic Gravity Flow
High-Capacity Q235B Phosphorized Gravity Flow Racking
Full ISO/CE/RoHS certified flow lane system with speed controllers and separator separators for strictly enforced FIFO cold storage and FMCG distribution.
Selecting the right metal pallet rack manufacturer determines warehouse throughput efficiency, structural safety, and capital expenditure amortization over decades. As an elite factory and worldwide exporter, our automated production lines turn premium Q235B and Q355 structural steel into high-density static and dynamic storage systems engineered to European and international structural benchmarks.
Full ISO/CE/RoHS certified flow lane system with speed controllers and separator separators for strictly enforced FIFO cold storage and FMCG distribution.
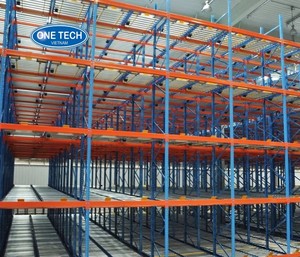
Self-sliding roller track design engineered with high-yield uprights and impact-resistant frame profiles to eliminate forklift intrusion into storage lanes.
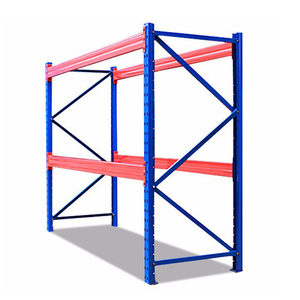
Custom structural profiles offering 100% direct pallet selectivity. Finished with electrostatic powder coating over an acid-pickled and phosphorized steel base.
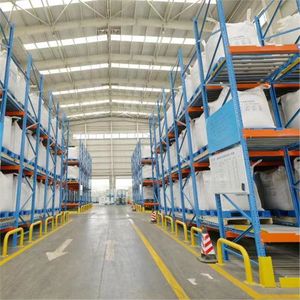
Engineered for perishables and pharmaceutical cold stores requiring optimal temperature distribution, continuous turnover, and zero operational bottlenecks.
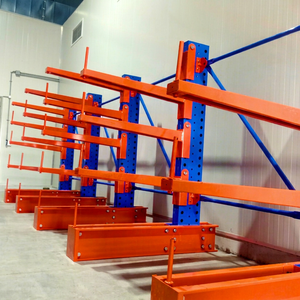
Eliminates front column constraints to provide continuous horizontal storage for timber, extrusion profiles, pipes, and oversized non-standard palletized stock.
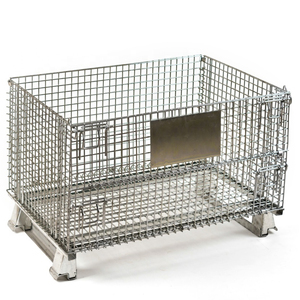
Collapsible and stackable electro-galvanized storage containers engineered for harsh shop-floor environments, auto parts distribution, and empty return freight savings.
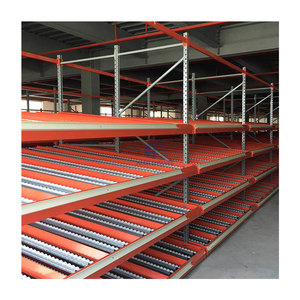
Hybrid high-density racking incorporating vertical flow tracks and ergonomic pick-faces tailored specifically for e-commerce split-case operations.
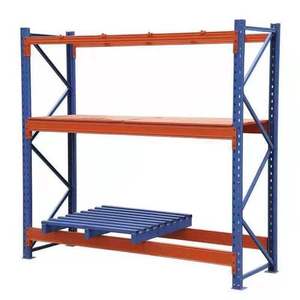
The proven industrial workhorse featuring precision 50mm and 75mm beam adjustment pitches, load-rated up to 4,500 kg per level for variable palletized inventories.
Direct-from-factory procurement of metal storage racking requires deep technical verification beyond superficial price-per-bay comparisons. Our engineering team breaks down the structural design standards, metallurgic grades, and surface treatments critical for longevity and regulatory sign-off.
The fundamental integrity of heavy-duty pallet racking begins at the steel mill. Certified exporters utilize hot-rolled structural coils adhering to certified mechanical properties. Standard upright columns and roll-formed box beams are manufactured from certified Q235B (yield strength ≥ 235 MPa) or high-strength Q355B (yield strength ≥ 355 MPa) steel. When designing multi-tier systems or rack-supported mezzanines exceeding 12 meters in clear height, structural calculations must account for dead load, live pallet loads, seismic horizontal forces, and forklift impact safety margins in compliance with EN 15512:2020 and RMI ANSI MH16.1 standards.
Delamination and sub-film corrosion are the leading causes of premature rack failure in high-humidity distribution hubs and cold storage facilities. World-class metal pallet rack factories employ an automated, multi-stage chemical pretreatment line prior to electrostatic spraying:
Stage 1: Alkaline Degreasing & Acid Pickling completely strips rolling oils and mill scale from the raw cold-formed steel.
Stage 2: Zinc Phosphating creates a crystalline chemical conversion layer that micro-mechanically anchors powder polymers and prevents rust migration if the finish is scratched.
Stage 3: Electrostatic Polyester Powder Application cured at 180°C to 200°C produces a durable 60–80 micron coating resistant to impact, chipping, and standard chemical spills.
International supply chains demand precise beam spacing and frame depth sizing. Standard European pallet specifications (EUR 1: 1200 × 800 mm, EUR 2: 1200 × 1000 mm) require specific frame depths (typically 1100 mm) to guarantee the mandatory 50 mm front and rear overhang. Utilizing substandard dimensions creates unapproved point loading on internal pallet deck boards and voids European warehouse safety insurance certifications.
Macro trends reshaping warehouse logistics: how automated guided vehicles, cold chain growth, and sustainability regulations affect racking procurement strategies.
Warehouses are transitioning from traditional drive-in racks to 4-way radio shuttle systems. Radio shuttles eliminate forklift travel inside deep racking channels, reducing rack impact structural damage by over 85% and cutting pallet cycle times significantly.
Autonomous mobile robots and turret trucks mandate strict floor-to-beam tolerances within ±1.5mm across 15-meter vertical rises. Racking manufacturers must adopt continuous roll-forming and CNC optical punching to ensure dimensional accuracy.
Sustainability audits and carbon border adjustment mechanisms (CBAM) are prioritizing bolted, modular racking systems manufactured from certified low-carbon steel. Standardized bolt-together modularity allows 100% component reconfiguration and zero-waste reinstallation when business operational footprints change.
As a dedicated manufacturing facility established in 2001, we provide global 3PLs, project contractors, and distribution networks with an integrated single-source supply chain from CAD layouts to sea container dispatch.
Equipped with 10 automated roll-forming lines, robotic beam welders, and an advanced electrostatic powder line delivering up to 30,000 tonnes of capacity every month.
Our in-house structural engineers supply customized layout drawings, aisle clearance verifications, and certified static load tables within 24 to 48 hours.
Certified with CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 No. 18624Q00169R0M, and comprehensive steel mill test certificates (MTC) with each shipment.
Standard seaworthy bundle strapping, numbered beam packaging, clear installation blueprints, and regular export shipping to Rotterdam, Hamburg, Felixstowe, and beyond.
Clear, definitive answers to essential technical, logistics, and compliance inquiries.
Receive a complimentary, engineer-certified 2D/3D layout proposal, bay load calculation, and factory-direct price quotation tailored to your operational specifications.