Engineered Systems
Featured Industrial Storage & Carton Flow Solutions
Explore our precision-fabricated gravity roller shelves, carton flow bays, and heavy-duty structural steel warehousing racks engineered for seamless logistics throughput.
Technical Whitepaper
Engineering Dynamic Carton Flow Racks: Mechanics, Physics, & Ergonomics
A comprehensive examination of dynamic gravity-fed live storage systems for international logistics directors, supply chain designers, and procurement managers seeking maximum throughput density.
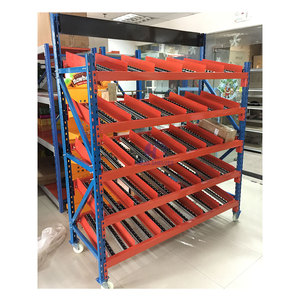
In modern high-velocity fulfillment environments, order picking represents up to 55% of total warehousing operational expenditure. Carton flow racking systems—often termed live storage or gravity roller shelving—solve the critical travel-time bottleneck by converting static shelving into continuous, gravity-powered replenishment corridors. Manufactured with inclined roller tracks, these systems separate replenishing crews at the rear charge face from picking operators at the front discharge face, guaranteeing absolute First-In, First-Out (FIFO) stock turnover and reducing operator travel distance by up to 75%.
75%
Travel Time Reduction
40%
Floor Footprint Savings
100%
Strict FIFO Compliance
300+
Picks Per Hour / Picker
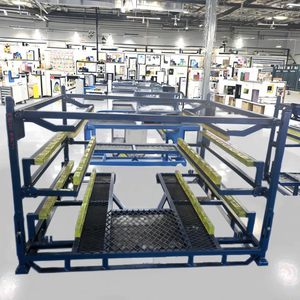
Engineered carton flow systems operate via an optimized gravitational incline gradient, typically between 2.5% and 5.0% (1.5° to 3.0°). When an operator extracts the leading tote or cardboard box from the picking shelf, subsequent cartons glide smoothly forward under gravity. This eliminates dead storage space, keeps picking aisles permanently replenished without forklift congestion, and creates an ergonomic presentation shelf equipped with tilt trays that position carton interiors directly in the picker's natural field of motion.
Mechanical Architecture
Key Structural Components of Heavy-Duty Carton Flow Beds
Comparing roller track compositions, load-bearing capacities, and anti-friction engineering designed to endure millions of load cycles.
Roller Tracks vs. Skatewheel Beds
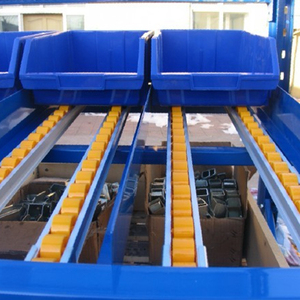
High-density polyethylene (HDPE) skatewheel tracks provide continuous multidirectional adaptability for variable carton widths. In contrast, full-width steel or polypropylene cylindrical roller tracks excel under heavy, uneven carton bases, distributing loads up to 150 kg per linear meter without corrugated carton deflection or snagging.
Integrated Flow Dividers & Guides
Full-depth zinc-plated steel lane dividers prevent skewing and package cross-track wedging. Tool-free clip-on adjustable lane separators allow immediate warehouse reconfiguration when packaging geometries change during seasonal SKU re-profiling or fast-fashion product rotations.
Ergonomic Tilt Trays & Impact Shelves
At the charging side, heavy-duty impact plates absorb the kinetic drop shock of heavily loaded totes without deforming roller axles. At the discharging pick face, 5° to 15° angled presentation tilt trays maximize visual SKU recognition and eliminate wrist-strain during rapid case piece extraction.
| Flow Bed Technology | Optimal Container Type | Load Rating (kg/m) | Incline Gradient | Maintenance Index | Industrial Suitability |
|---|---|---|---|---|---|
| Polypropylene Skatewheel Lane | Rigid plastic totes, KLT bins | 50 – 90 kg | 2.5% – 3.5% | Low / Self-Lubricating | E-commerce fulfillment, 3PL fast-pick |
| Continuous Steel Roller Tracks | Corrugated boxes, wooden crates | 100 – 250 kg | 3.5% – 5.0% | Zero / Sealed Bearings | Automotive lineside, heavy hardware |
| Full-Width Aluminium Roller Beds | Flexible polybags, blisters, uneven bins | 60 – 120 kg | 3.0% – 4.0% | Minimal / Anti-Static | Pharmaceutical, electronics assembly |
| Braked Dynamic Gravity Rollers | Heavy liquid drums, chemical totes | 200 – 400 kg | 2.0% – 3.0% | Periodic Inspection | Cold storage, chemical storage, beverage |
Market Intelligence
Future Procurement Trends in Carton Flow Racking Systems (2025–2030)
How automation convergence, sustainable metallurgy, and near-line micro-fulfillment are reshaping B2B carton flow procurement.
The global intralogistics landscape is experiencing a structural pivot. While classical static pallet racking remains fundamental for reserve storage, distribution centers are converting lower levels into high-throughput dynamic picking tunnels. Sourcing directors in North America, Europe, Australia, and the Middle East are prioritizing four primary technological shifts when issuing RFQs to Chinese racking exporters:
1. AMR & Cobot Synergy (Hybrid Flow Faces)
Future-ready carton flow tracks are designed with clearance apertures for Autonomous Mobile Robots (AMRs). Automated guided vehicles navigate picking aisles to receive items directly dropped by human pickers or robotic articulated arms, bridging manual order consolidation with fully automated warehouse execution systems (WES).
2. Integrated Pick-to-Light & RFID Sensors
Procurement teams are ditching standalone aftermarket light bars in favor of pre-wired, factory-slotted beam profiles. These channels conceal low-voltage cabling and bus communication networks, enabling instant plug-and-play Pick-to-Light (PTL) displays, wireless sensor nodes, and real-time inventory level recalculation.
3. Decarbonized Steel & Eco-Coatings
Under tightening global Scope 3 ESG regulations (such as the EU Carbon Border Adjustment Mechanism - CBAM), international buyers require Chinese manufacturers to provide mill test certificates verifying scrap-metal recycling rates, clean electric-arc-furnace steel billets, and lead-free, zero-VOC thermosetting powder coatings.
Verified Manufacturing Authority
Why Global Supply Chains Partner With Guangzhou Heda Shelves Co., Ltd.
Established in 2001, Guangzhou Heda Shelves Co., Ltd. delivers institutional-grade racking production, rigorous international standard compliance, and turnkey OEM/ODM export solutions.
2001
Year Established
30,000m²
Modern Manufacturing Plant
30,000t
Monthly Production Capacity
120+
Countries Successfully Served
As one of China's premier racking and shelving exporters, Guangzhou Heda Shelves Co., Ltd. maintains a staff of over 300 experienced technical specialists, structural engineers, and QA inspectors. Our systems are engineered in strict accordance with the European racking standard EN 15512, the structural tolerance code EN 15620, and international load testing protocols. We hold official CE Certification (No. 2435-CPR-8605159), accredited ISO 9001:2015 Quality Management Certification (No. 18624Q00169R0M), and full RoHS compliance documentation.
Our 10-Step In-House Precision Manufacturing Lifecycle
STEP 01
Steel Inspection
Spectrometric tensile verification of prime Q235B cold-rolled coils.
STEP 02
CNC Slitting
Micrometer-calibrated longitudinal coil cutting with zero edge burr.
STEP 03
Auto Punching
High-speed CNC progressive punch dies maintaining exact 50mm pitch.
STEP 04
Cold Roll Forming
Multi-station continuous roll formers creating stiff omega upright profiles.
STEP 05
Laser Beam Cutting
Automated fiber lasers profiling connector brackets and bed hooks.
STEP 06
Robotic Welding
Multi-axis automated gas-shielded arc welding ensuring weld root integrity.
STEP 07
Surface Polishing
Automated mechanical deburring and shot blasting to Sa 2.5 purity.
STEP 08
Pickling & Phosphating
Multi-tank chemical bath pre-treatment preventing sub-surface oxidation.
STEP 09
Powder Coating
Electrostatic spray guns curing 60–90µm durable thermoset epoxy-polyester.
STEP 10
Export Packaging
Component-numbered seaworthy bundling with protective edge steel straps.
Procurement Guidance
Frequently Asked Technical Questions (FAQ) for Global Buyers
Clear, authoritative engineering guidance addressing installation tolerances, load factors, shipping logistics, and custom integrations.
What is the recommended pitch gradient for varying carton weights?
For standard cardboard cartons weighing between 5 kg and 25 kg, an incline of 3.0% to 3.5% (approx. 18 mm to 21 mm drop per linear meter) ensures dependable gliding without excessive terminal impact. Lightweight boxes below 3 kg require up to 4.5% to overcome initial roller inertia, whereas rigid plastic containers gliding on precision HDPE skatewheels operate flawlessly at 2.5%.
Can HEDA carton flow beds retrofit into existing pallet rack uprights?
Yes. Guangzhou Heda Shelves Co., Ltd. manufactures universal bracket adaptors and drop-in hanger clips compatible with tear-drop, slotted, diamond, and European 50mm/75mm upright pitch profiles. Our engineers calculate beam deflection limits according to EN 15512 to ensure the retrofitted flow bed preserves structural integrity without field welding.
How do you resolve carton hanging or deflection on roller tracks?
Corrugated cardboard absorbs atmospheric humidity, causing the bottom flap to soften and deflect over widely spaced skatewheels. To eliminate this friction trap, we specify full-width cylindrical steel rollers or multi-track skatewheel beds with tightened roller centers (30mm–50mm pitch), distributing the base load across multiple simultaneous contact points.
What is the typical production and overseas shipping lead time?
Standard carton flow configurations require 15 to 25 calendar days for production at our Guangzhou factory. Ocean container shipping to major ports (Rotterdam, Hamburg, Felixstowe, Long Beach, Sydney) spans 18 to 38 days. Every consignment includes detailed piece-marked 3D assembly blueprints, hardware lists, and step-by-step installation manuals.
Are custom RAL powder coat colors available for OEM branding?
Yes. As a direct manufacturer, we provide complete electrostatic powder coating customisation across the standard RAL color spectrum (including RAL 5015 Blue, RAL 2004 Orange, RAL 7035 Grey, and custom corporate colors). Our automated line applies high-adhesion anti-scratch coatings tested against 500-hour salt spray corrosion resistance.
What documentation is provided for local building & safety permits?
We supply official Mill Test Certificates (MTCs), CE Declaration of Performance (DoP), ISO 9001:2015 certificates, CAD installation drawings, and certified load capacity plaques complying with EN 15635 warehouse safety standards, ensuring smooth sign-off by municipal structural inspectors and insurance auditors.
Request Your Custom Carton Flow Engineering Layout & Catalog
Consult with our structural engineering team today. Submit your warehouse floor plan (CAD or PDF), SKU dimensions, and load specs for a complimentary 3D layout, load-deflection calculation, and factory-direct volume quotation.