Precision-Engineered Industrial Rack Systems
Explore our flagship product configurations manufactured from certified high-tensile Q235B and Q355B hot-rolled micro-alloyed structural steel. Designed to optimize high-cube storage volume, accelerate unit-load throughput, and withstand rigorous seismic and dynamic forklift loads.
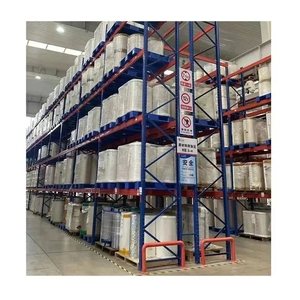
Metal Racking Adjustable Heavy Duty Rack System Warehouse Storage Steel Warehouse Pallet Shelving
Engineered with continuous multi-bend upright omega columns, providing unmatched rigidity and vertical deflection control for high-bay logistics facilities.
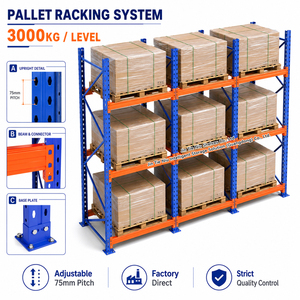
3 Pallet Levels Heavy Duty Steel Warehouse Rack Selective Pallet Racking System 3000KG
Heavy-duty step beams and boxed profile connectors with 4-finger locking pins deliver structural stability under heavy pallet load distributions.
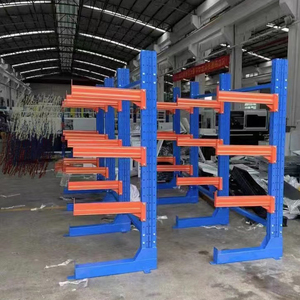
Industrial Pipe Shelves Arm Steel Warehouse Shelf Storage Metal Heavy Duty Rack Cantilever Racking
Eliminates frontal upright obstruction for rapid handling of timber packs, steel tubes, aluminum profiles, and extruded industrial construction materials.
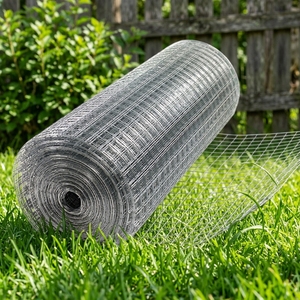
Galvanized Welded Wire Mesh Roll Hardware Cloth Square Grid Garden Fence Animal Cage Screen Wholesale Manufacturer
Industrial galvanized wire containment grids engineered for rack safety cladding, flanged pallet drop decking, and perimeter security enclaves.
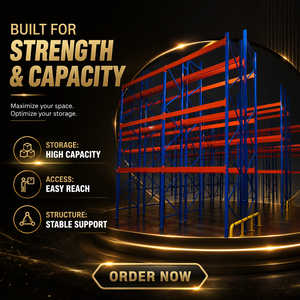
High Density Narrow Aisle Pallet Racking Adjustable Beam Steel Storage System Powder Coated for Warehouses
Shrinks operational aisle width down to 1,600mm. Boosts volumetric footprint utilization by over 45% while preserving 100% individual pallet selectivity.
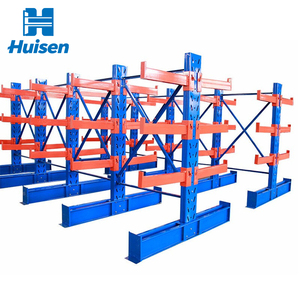
Wholesale Industrial Warehouse High Density Cantilever Rack Industrial Steel Single Double Side Cantilever Rack Shelving
Heavy structural I-beam columns paired with pivoting articulated arms that protect both stock and rack uprights during forklift impact and placement.
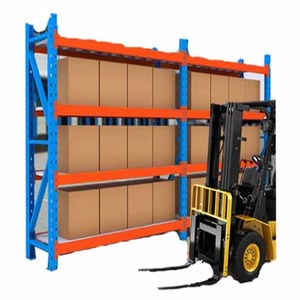
Selective Heavy Duty Pallet Rack 4000kg Capacity Industrial Warehouse Steel Storage System Rack Pallet Shelving Solution
Engineered for high unit weights, master tooling, dies, and liquid bulk totes. Features reinforced base anchoring and heavy-gauge diagonal brace lattices.
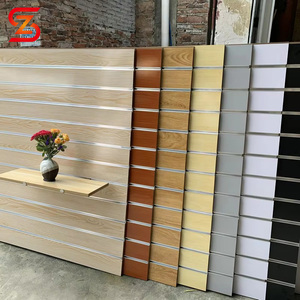
Modern Custom Shop Wall-mounted Display Rack Retail Display Wooden Display Rack Lightweight Wall-mounted Display Rack
Industrial-grade wall-mounted uprights combining architectural aesthetics with high load strength for commercial distribution showrooms and retail parts counters.
Guangzhou HEDA Shelves: Engineering Global Storage Reliability Since 2001
For B2B procurement leaders, supply chain executives, and EPC system integrators, rack failure is never an option.
Founded over two decades ago in Guangzhou, China, Guangzhou HEDA Shelves Co., Ltd. has grown into an international powerhouse in structural warehouse racking manufacturing. Operating an expansive 30,000 m² state-of-the-art manufacturing campus staffed by over 300 experienced engineers, certified welders, and logistics planners, HEDA Shelves manufactures up to 30,000 metric tons of certified racking monthly.
Unlike commodity fabricators, HEDA Shelves integrates complete design authority. Every storage rack project undergoes multi-stage structural design verification, finite element modeling (FEM), and adherence to local regulatory wind, seismic, and floor slab load requirements—whether deploying in Western Europe, North America, the Middle East, or Australia.
Zero-Cost 3D & CAD Design
Tailored structural blueprints, aisle turning clearances, and beam profile calculations supplied within 24 hours.
Automated Profiling Lines
Continuous CNC roll-forming lines guarantee millimeter-accurate upright hole pitch (50mm/75mm) across entire high-bay spans.
10-Stage Surface Finish
Acid pickling, zinc phosphating, and electrostatic powder coating create high salt-spray corrosion resistance (up to 500+ hours).
Turnkey Global Export
Exporting to Rotterdam, Hamburg, Antwerp, Los Angeles, Dubai, and Sydney with custom bundling, numbered components, and direct DDP support.
Strategic Procurement Trends Transforming Global Warehousing
Modern supply chain leaders face escalating industrial land rents, labor constraints, and complex SKU omni-channel demands. The storage equipment procurement paradigm has evolved from commodity metal buying to strategic architectural capital investment.
High-Cube Verticalization Over Horizontal Expansion
With industrial urban real estate rates surging globally, operators are replacing conventional 6-meter ceiling layouts with 12 to 24-meter ultra-vertical footprints. This trend demands superior steel yield strength (e.g., micro-alloyed Q355B), precise column straightness tolerances (L/1000 per EN 15620), and engineered seismic anchor base plates capable of absorbing significant moment stresses.
Total Cost of Ownership (TCO) vs. Initial CapEx
Sophisticated procurement committees prioritize whole-life structural integrity over initial bidding price. Inexpensive light-gauge racking often results in catastrophic beam sagging, frame twist, forklift damage downtime, and premature replacement. Top enterprise buyers evaluate weld penetration geometry, epoxy-polyester powder film thickness (60–80 microns), and structural safety factors (1.5x to 2.0x working load limits).
Carbon Footprint & Circular Steel Sourcing
Corporate ESG benchmarks now mandate verifiable green manufacturing footprints. Modern racking tenders demand electric arc furnace (EAF) low-carbon steel, heavy metals elimination under RoHS compliance, and 100% closed-loop zero-VOC powder-coating recovery systems. HEDA Shelves integrates resource-efficient cold-forming and eco-friendly pre-treatments aligned with international net-zero mandates.
Next-Generation Engineering & Automation Integration
The line separating static structural steel from automated material handling has dissolved. Contemporary rack systems serve as high-precision physical infrastructures supporting autonomous guided vehicles (AGVs), automated storage and retrieval systems (ASRS), and artificial intelligence-driven warehouse management platforms.
Semi-Automated Radio Shuttle Satellites
By pairing structural drive-in chassis channels with radio-controlled lithium-powered shuttle carriers, high-density storage transforms into a high-throughput, low-impact engine. Forklifts stay strictly in access aisles, completely eliminating in-lane frame collisions, slashing SKU transit cycles, and enabling dynamic conversion between FIFO (First-In, First-Out) and LIFO (Last-In, First-Out) operations.
Cold-Formed High-Tensile Micro-Alloy Steels
Advanced metallurgical profiling allows manufacturers to engineer multi-ribbed upright sections with reduced tare weight yet higher yield properties (up to 355–420 MPa). Cold-formed profiles with complex stiffening folds resist local torsional buckling and secondary flexure, delivering extreme seismic load-carrying reliability with minimized freight cubic weight.
Digital Twin & FEA Structural Simulations
Prior to physical roll-forming, comprehensive 3D finite element analysis (FEA) simulations stress-test beam-to-column connector moments, frame base flexibility, and floor anchoring shear loads under maximum seismic acceleration. This ensures precision compliance with local building codes, preventing over-engineering costs while verifying rigorous structural safety.
Industrial Storage Systems Technical Selection Matrix
A technical evaluation guide utilized by our senior structural project engineers to guide B2B buyers in matching inventory velocity, building geometry, and equipment investment.
| Storage System Type | Space Density | SKU Selectivity | Picking Throughput | Handling Equipment Required | Target Sector & Operational Fit |
|---|---|---|---|---|---|
| Standard Selective Pallet Racking | Standard (40%) | 100% Direct | High Speed | Standard Counterbalance / Reach Truck | 3PL multi-client distribution, FMCG warehouses, e-commerce retail hubs. |
| Very Narrow Aisle (VNA) Racking | High (65%) | 100% Direct | Very High | VNA Man-up / Turret Forklift (Wire-guided) | High-bay warehouses, pharmaceutical spare-parts, premium cubic space sites. |
| Radio Shuttle High-Density Racking | Ultra High (85%) | Channel-Based | Automated / Fast | Standard Forklift + Automated Shuttle Unit | Cold storage (-25°C), beverage distributors, meat & produce deep freezing. |
| Drive-In / Drive-Through Systems | Very High (75%) | Low (LIFO / FIFO) | Moderate | Standard Reach Truck / Counterbalance | Raw commodity bulk storage, seasonal agricultural harvests, uniform SKUs. |
| Heavy-Duty Cantilever Racking | Variable | 100% Open Access | Fast | Side Loader / Four-Directional Forklift | Steel pipes, timber bundles, extrusions, gypsum drywall, bar materials. |
| Rack-Supported Mezzanines | Max Cubic (100%+) | 100% Multi-Tier | Manual / Conveyor | Pallet Gate, Freight Elevator, Hand Cart | Garment distribution, small-parts automotive picking, document archives. |
Frequently Asked Questions for Storage Rack Procurement
Direct answers from our structural engineering and export compliance department addressing common technical, regulatory, and logistics inquiries.
Our rack components are engineered strictly from certified prime structural carbon steel grades Q235B and Q355B (equivalent to European EN 10025 S235JR and S355JR; and ASTM A36 / A572 Grade 50). Structural designs, allowable stress limits, and deflection criteria are calculated in compliance with European standard EN 15512:2020, FEM 10.2.02, and US RMI (ANSI MH16.1) protocols. Mill test certificates (MTC) detailing chemical composition, yield strength, elongation, and Charpy impact values accompany every production lot.
Per EN 15512 specifications, the maximum allowable vertical elastic deflection of a horizontal load beam under full safe working load (SWL) cannot exceed L/200 (span length divided by 200). For high-precision automated systems such as VNA or ASRS, deflection criteria are tightened to L/300 or L/400. Our structural design implements a minimum safety factor of 1.5 against steel yield and a factor of 1.95 against ultimate tensile rupture for all load-bearing connections.
To generate an engineered layout and preliminary bill of materials (BOM), our application engineers require: (1) An architectural warehouse floor plan (DWG or PDF) noting column grids, ceiling clear height, fire sprinklers, and overhead doors; (2) Pallet dimensions (W x D x H) including overhang and gross load weight; (3) Handling equipment model and turning radius (AST); (4) Operating temperature (ambient vs -25°C cold chain); and (5) Local seismic zone acceleration values if known.
International maritime shipments face high relative humidity and salt air exposure. Prior to powder coating, components undergo automated multi-bath chemical cleaning, acid pickling, and micro-crystalline zinc phosphating to seal the steel substrate. We then apply thermosetting epoxy-polyester powder coating (60–80μm) baked at 180°C–200°C. For international freight, components are secured with dense corrugated wrapping, heavy-duty plastic film buffering, corner protectors, and steel-banded seaworthy timber skids designed for rapid container destuffing without surface abrasion.
Yes. Over 40% of our production volume supports private-label distributors, racking installers, and warehouse equipment integrators across North America, Europe, Australia, and the Middle East. We offer custom roll-forming tooling for unique upright column hole patterns, branded end-plate stamping, tailored corporate RAL powder-coat hues (e.g., RAL 5015 Blue, RAL 2004 Orange, RAL 7035 Grey), and white-label component identification and packing lists.
In high seismic regions (such as Chile, New Zealand, California, or Southern Europe), dynamic ground acceleration generates severe overturning moments on upright frames. Our structural engineers compute P-Delta lateral sway effects and enlarge column base plates from standard 100x100mm to heavy 160x180mm or larger with dual M12/M16 chemical adhesive anchors. Floor slab compressive strength ($f'_c \ge 25\text{–}30\text{ MPa}$) and slab rebar clearance are verified to ensure zero anchor pull-out failure under design-basis earthquake (DBE) scenarios.
Following final CAD layout sign-off and structural approval, standard order fabrication requires 15 to 25 days at our Guangzhou factory. Major multi-thousand pallet high-bay installations are produced in planned container batches. Ocean transit typically takes 18–24 days to US West Coast ports, 28–35 days to US East Coast, 28–32 days to Northern European hubs (Rotterdam/Hamburg), and 12–16 days to Australian ports. HEDA Shelves coordinates full export customs documentation, bills of lading, and certificate of origin protocols.
Every container shipped includes comprehensive piece-marked installation drawings, assembly sequence diagrams, torque verification specifications for all structural bolts (grade 8.8 minimum), and safe working load (SWL) bay warning placards. For major turnkey projects, HEDA Shelves can dispatch bilingual site installation supervisors or coordinate live video technical assistance to guide local installation teams through anchor drilling, plumb alignment, and laser leveling.
Plan Your Next Warehouse Expansion With HEDA Shelves
Partner directly with a trusted global manufacturer. Leverage our 25 years of structural racking expertise, free 3D CAD design engineering, verified CE/ISO certifications, and cost-efficient factory-direct pricing for your logistics facility.