Featured Industrial Racking & Heavy-Duty Shelving Systems
Direct-from-manufacturer heavy and medium-duty configurations compliant with EN 15512, FEM 10.2.02, and ANSI MH16.1 standards. Tailored for Euro-pallet dimensions, multi-tier distribution centres, and automated logistics hubs.
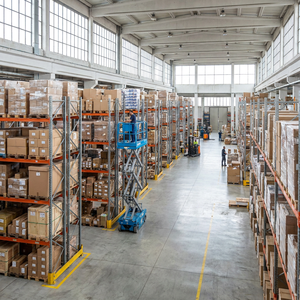
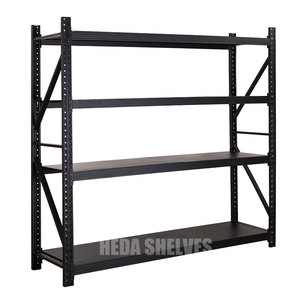
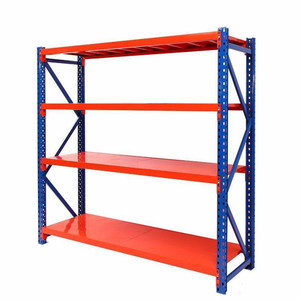
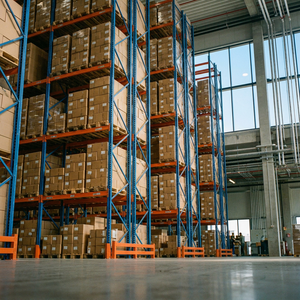
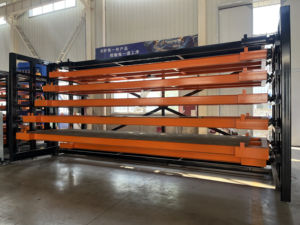
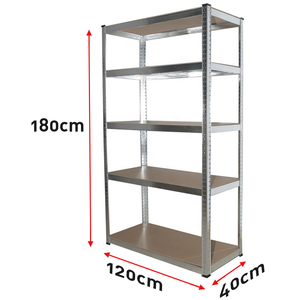
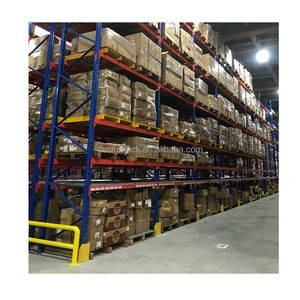
Navigating the Global Industrial Racking & Storage Matrix
How leading logistics engineers, 3PL aggregators, and manufacturing enterprises systematically de-risk capital procurement, verify structural engineering standards, and calculate lifecycle TCO.
Structural Safety & EN Compliance
Sourcing industrial storage is fundamentally an engineering liability decision. Structural failures trigger catastrophic operational paralysis. Procurement teams must demand full traceability under European Standard EN 15512:2020 (Steel static storage systems), verification of beam deflection limits (strictly ≤ L/200), and Eurocode 8 seismic resistance criteria for unbraced and braced pallet frames.
Metallurgical Grade Transparency
A supplier's certified mill test certificates (MTC) dictate long-term frame stability under extreme cyclic loading. Premium exporters utilize Q235B (yield strength ≥ 235 MPa) or high-yield Q355B (equivalent to European S355JR), featuring cold-formed continuous profiling that avoids micro-fractures in column omega-sections and prevents beam teardrop detachment.
Total Cost of Ownership (TCO)
Freight packaging efficiency, pre-treatment chemical coating lifecycles, and boltless field reconfigurability represent 42% of a warehouse racking system's actual 10-year operating cost. Direct factory sourcing with automated punching lines reduces installation labor hours by 30% through zero-tolerance component fitment.
Comparative Engineering Architecture: Racking & Shelving Systems
Compare load characteristics, SKU selectivity, and facility footprint optimization to match your specific supply-chain throughput requirements.
| System Architecture | Volumetric Efficiency | SKU Access Speed | Typical Payload / Level | Target Handling Equipment | Structural Compliance |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Immediate | 1,000 – 4,500 kg | Counterbalance, Reach Trucks | EN 15512 / ISO 9001 / CE |
| Double Deep Racking | High (60-65%) | 50% Immediate (FILO) | 1,000 – 3,000 kg | Deep-Reach Pantograph | EN 15620 Tolerances |
| Drive-In / Drive-Through | Very High (75-85%) | Lane Dependent (LIFO/FIFO) | 800 – 2,000 kg | Standard Counterbalance | FEM 10.2.07 Guidelines |
| Radio Shuttle Automation | Maximum (85-92%) | Semi-Automated High Throughput | 500 – 2,500 kg | Forklift + Smart Shuttle Cart | CE Machinery Directive / EN 15512 |
| Multi-Tier Mezzanine Racking | Vertical Expansion (>200%) | 100% Manual Hand-Pick | 300 – 1,000 kg / m² | Pedestrian, Conveyors, Vertical Lifts | Eurocode 3 / EN 1090-2 |
| Industrial Longspan Shelving | Flexible Bin Storage | 100% Ergonomic Pick | 200 – 800 kg / shelf | Manual Cart / Toter Handlers | TUV / GS Safety Certified |
* Note: Realized density percentages depend on facility clear ceiling heights, aisle dimensions, and emergency egress corridors prescribed by local fire protection regulations (NFPA 13 / EN 12845).
Future Procurement Trends in Warehouse Storage (2025–2030)
Macro-economic shifts, environmental mandates, and robotic integration are redefining global industrial shelving procurement specifications.
1. Scope 3 Carbon Audits & Green Steel
Global logistics operators and institutional developers (Prologis, Goodman) now mandate embodied carbon accounting for warehousing infrastructure. Racking manufactured from Electric Arc Furnace (EAF) recycled billet versus traditional Basic Oxygen Furnaces (BOF) yields an immediate 40–58% reduction in Scope 3 embodied carbon. Pre-treatment powder coatings formulated with VOC-free electrostatic polyester cure at lower thermal bands, satisfying stringent ESG due-diligence protocols.
2. AMR & Robotic Automation Readiness
The boundary between static racking and automated material handling has dissolved. Future-proof procurement dictates upright baseplate tolerances configured for autonomous mobile robots (AMRs) and automated guided vehicles (AGVs). Floor anchor shear capacities must accommodate heavy point-loads, and lower beam elevations require laser-guided target reflectors and minimum deflection margins under continuous 24/7 robotic cycle wear.
3. High-Density Micro-Fulfillment
E-commerce pressure for sub-2-hour urban delivery is driving suburban warehouse mezzanines and multi-tier picking structures. Instead of building expansive new facilities, procurement heads specify rack-supported multi-tier platforms that expand cube utilization up to 300%. These systems require unified modular integration: sprinkler line cutouts, integrated carton flow tracks, anti-collapse back-mesh, and pick-to-light bracket channels.
4. Nearshoring Strategic Safety Stocks
Supply chain vulnerabilities have catalyzed a global transition from strict "Just-in-Time" to resilient "Just-in-Case" buffering. Importers and warehouse operators are configuring deeper storage layouts—such as 4-to-6-pallet deep push-back and radio shuttle lanes—to buffer volatile sea-freight lead times while preserving high throughput selectivity for critical fast-moving industrial and consumer inventory.
Guangzhou HEDA Shelves: 25 Years of Precision Storage Engineering
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a high-capacity 30,000 m² production complex, exporting mission-critical warehouse storage racking and mezzanine platforms across Europe, the Americas, Oceania, and Southeast Asia.
Rigorous European Accreditations
Our manufacturing infrastructure is accredited under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 Certification No. 18624Q00169R0M. All engineered pallet racks conform to EN 15512 static steel storage design guidelines and undergo continuous third-party mechanical deformation audits.
Free 3D Layout & CAD Engineering
Before cutting a single coil of steel, our senior in-house application engineers provide comprehensive AutoCAD layout plans, DWG files, and 3D architectural renderings. We calculate aisle turning radiuses for your specific forklift fleet (VNA, Reach, Counterbalance) to optimize square-meter utilization.
Turnkey Global Export & Port Shipping
Exporting heavy structural components across international boundaries demands seaworthy bundle packaging, specialized strapping, and optimized container nesting to prevent transit abrasion. We regularly manage high-volume direct dispatches to Rotterdam, Hamburg, Antwerp, Felixstowe, Valencia, Long Beach, and Santos.
Inside the Factory: The 10-Step Quality Assurance Cycle
How raw cold-rolled steel coils are precision-transformed into heavy-duty, corrosion-resistant racking assemblies under automated ISO 9001 supervision.
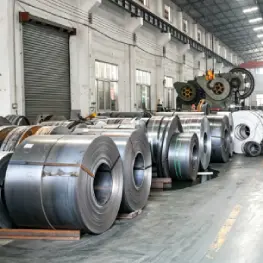 STEP 01
Raw Material Spectrometry
Certified metallurgical testing of prime carbon steel coils for chemical composition and tensile yield.
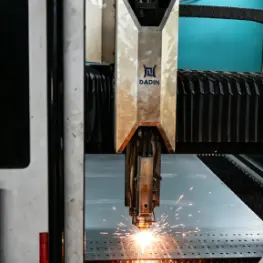 STEP 02
Precision CNC Slitting
Automated continuous de-coiling and narrow tolerance slitting ensures razor-sharp edge uniformity.
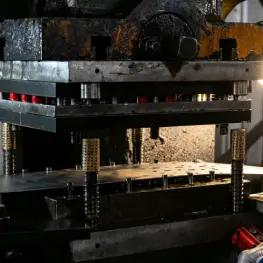 STEP 03
Multi-Hole High Speed Punching
Automated pitch punching on 50 mm / 75 mm centers with 0.1 mm repeatability along 12 m vertical lengths.
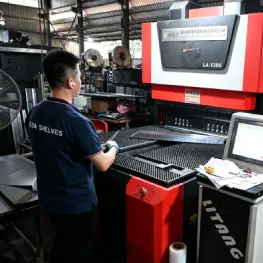 STEP 04
Continuous Cold Roll-Forming
18-to-24 rolling station passes form high-stiffness omega upright sections and interlocking step beams.
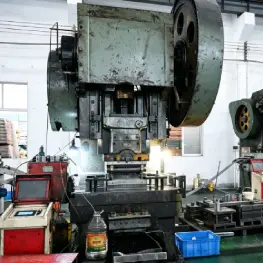 STEP 05
Box Beam Cold Joining
Twin C-channels interlocked and continuous seam-welded to form high-inertia structural box beams.
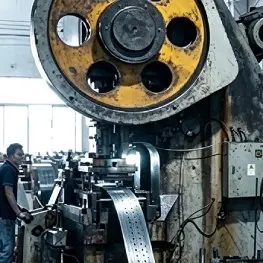 STEP 06
Laser Deburring & Polishing
Removal of steel slag, micro-burrs, and sharp edges to ensure flawless surface adhesion and operator safety.
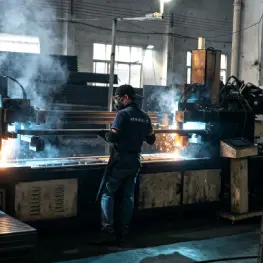 STEP 07
Robotic Connector Welding
Multi-claw connector brackets welded via automated Panasonic robotic cells for zero-defect weld beads.
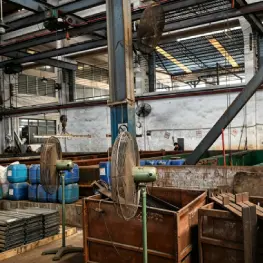 STEP 08
8-Stage Chemical Pre-Treatment
Degreasing, acid pickling, passivation, and zinc-phosphating create a nanoscale rust-inhibiting anchor layer.
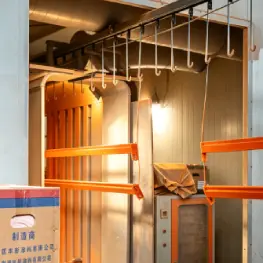 STEP 09
Electrostatic Powder Coating
Swiss Gema automatic guns deposit 60–90 μm of epoxy-polyester powder, cured in a 200°C tunnel oven.
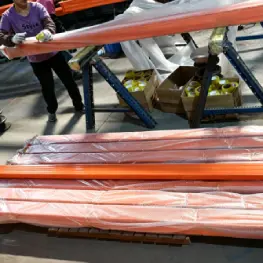 STEP 10
Load Testing & Seaworthy Pack
Deflection load cell validation followed by timber battens, air-cushion wrapping, and steel container bundling.
Frequently Asked Engineering & Sourcing Questions
Straightforward, technical answers for supply chain directors, warehouse operations leads, and global EPC procurement managers.
How can overseas buyers verify that racking products genuinely meet EN 15512:2020 standards?
What is the allowable beam deflection limit for heavy-duty pallet racking under full payload?
How do Euro pallets (1200 x 800 mm) impact beam length and upright frame depth configurations?
What anti-corrosion finish is recommended for outdoor yards vs. cold storage sub-zero environments?
What are typical production lead times, and how do you optimize ocean freight container stuffing?
Can HEDA Shelves manufacture OEM/ODM private-label racking for European racking distributors?
Request an Engineered CAD Layout & Factory Quote
Collaborate directly with our senior structural storage engineers. Send us your architectural floor plan or operational requirements to receive a complete CAD design, pallet capacity schedule, and landed cost estimation within 24 hours.
- Free 2D/3D AutoCAD Layout Plans
- Certified EN 15512 Load Calculation
- FOB / CIF / DDP Logistics Pricing
- Direct Manufacturer Pricing Advantage
Talk to an Application Engineer
Live project consultation with English-speaking technical personnel. Fast turnaround on custom configurations.
Contact Us