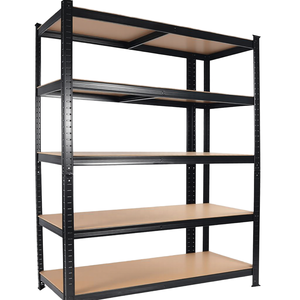
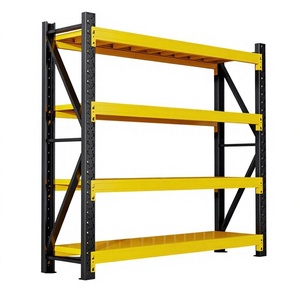
1200mm Electrostatic Powder Coated Steel Multi Tier Stacking Rack with Pallet Support Bar
Stackable Mobile Base
Anti-Corrosion Finish
Explore our factory-engineered storage systems designed to maximize vertical capacity, streamline pallet accessibility, and lower total cost of ownership across distribution centres.
An in-depth analysis of high-density dynamic storage engineering, seismic safety mitigation, and ROI benchmarking for cold chain logistics and enterprise distribution hubs.
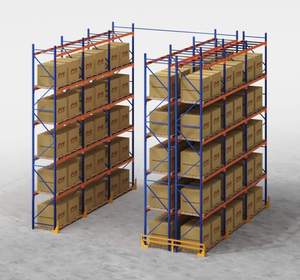
Traditional selective pallet racking requires dedicated aisle access for every storage row, resulting in aisles consuming up to 60% of total warehouse floor footprint. In contrast, electrical or rail-guided movable pallet racking systems mount heavy-duty shelving units onto motor-driven mobile carriages traversing embedded floor tracks.
By compressing inactive service aisles into a single movable access corridor, facilities recover between 80% and 100% more storage volume within an identical building envelope. This spatial density proves transformative for high-cube warehousing and controlled-atmosphere storage facilities.
Movable pallet racking systems operate under dynamic vibrational stress, inertia, and cyclic lateral displacement. As a China wholesale manufacturer certified to ISO 9001:2015 and CE standards, our engineering methodology integrates rigorous EN 15512 and FEM 10.2.07 structural compliance protocols.
Uprights are cold-formed from certified Q235B and high-yield Q355B structural steel coils. We apply multi-stage finite element modeling (FEM) to analyze frame deflection limits, base connection moments, dynamic torque loads during carriage acceleration, and seismic shear mitigation.
In low-temperature and deep-freeze logistics (-25°C to -30°C), thermal volume cooling constitutes up to 70% of ongoing operational expenditures. Storing ambient air in unused forklift corridors accelerates thermodynamic thermal transfer and escalates electrical refrigeration demands.
Deploying movable pallet racking collapses unnecessary empty void space. By concentrating pallet volume density by up to 2×, facilities reduce the required refrigerated chamber footprint by roughly 45%, achieving measurable electrical savings and decreasing corporate carbon footprint under global ESG mandates.
| System Architecture | Floor Space Utilization | Pallet Selectivity | Handling Equipment Required | Primary Industrial Use-Case |
|---|---|---|---|---|
| Movable Pallet Racking (Motorized) | 85% – 92% (High-Density) | 100% Direct (Dynamic Aisle) | Standard Counterbalance / Reach Truck | Cold Storage, Pharma DC, High-Value Inventory |
| Selective Pallet Racking (Static) | 35% – 42% (Aisle Intensive) | 100% Direct (Static Aisles) | Any Standard Forklift Fleet | Multi-SKU 3PL Fulfillment, Retail Fast-Movers |
| Drive-In Pallet Racking | 65% – 75% (Dense Lane) | LIFO / Restricted Lane Access | Specialized Narrow-Chassis Forklifts | Batch Manufacturing, Seasonal Raw Materials |
| Radio Shuttle High-Bay | 80% – 88% (Deep-Lane) | LIFO / FIFO (Shuttle Automated) | Standard Forklift + Automated Carrier | FMCG, High-Turnover Beverage Logistics |
How automation, IoT sensorization, and resilient manufacturing processes are transforming international racking procurement across North America, Europe, and the Middle East.
Procurement teams are moving away from isolated manual mobile racks toward integrated automated fleets. The modern movable racking carriage is interfaced directly with the warehouse control system (WCS) and warehouse management software (WMS) via industrial Wi-Fi and optical protocols.
Carriages open automatically upon the dispatch call of an autonomous reach truck or AMR. This eliminates human waiting intervals, synchronizes dispatch algorithms, and reduces forklift collision accidents through sensor-locked aisle interlocks.
Smart movable racking now incorporates embedded dynamic load cells, strain gauges, and vibration sensors along carriage tracks and critical frame nodes. These telemetric nodes stream real-time data to maintenance dashboards.
Any uneven floor settlement, rail misalignment, structural load imbalance, or accidental forklift impact is flagged instantly before structural fatigue compromises rack geometry, ensuring full alignment with OSHA and EN 15635 annual inspection regimens.
Global supply chain volatility has pushed Tier-1 racking distributors and 3PL enterprises away from intermediaries toward direct wholesale relationships with Chinese manufacturing powerhouses. Wholesale buyers prioritize manufacturers offering verifiable CE / ISO certifications, in-house roll forming, and automated powder coating.
A direct factory relationship lowers landed equipment costs by 25% to 38% while unlocking direct engineering support for custom bay layouts, non-standard RAL colors, and specialized seismic floor anchoring schemes.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a premier Chinese manufacturer specializing in high-capacity warehouse racking, cantilever platforms, and engineered mobile storage.
A 30,000 m² state-of-the-art facility featuring 10 precision production stages: automated CNC punch presses, continuous roll-forming lines, robotic welding stations, and a dual-line electrostatic powder coating facility delivering 30,000 tonnes monthly.
All structural calculations and weld procedures carry authoritative certifications: CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 No. 18624Q00169R0M, and comprehensive RoHS compliance, ensuring smooth local regulatory compliance in the EU, UK, and Americas.
Our in-house design engineering office delivers site-specific DWG floor plans, 3D parametric simulations, and capacity load matrices within 24 to 48 hours of initial brief submission, allowing rapid review by local architects and civil inspectors.
Serving over 120 countries with seaworthy bundle packaging, anti-abrasion wrapping, and numbered component coding. We offer seamless FOB, CIF, or DDP shipments delivered directly to major ports including Rotterdam, Hamburg, Los Angeles, and Felixstowe.
Authoritative guidance covering structural design, civil floor preparation, lead times, and OEM customization protocols.
Movable pallet racking rails demand tight floor flatness tolerances under DIN 18202 or ASTM E1155 standards (typically Flatness FF 50 / FL 50). Tracks can be embedded within the initial floor slab pour or installed into precision diamond-cut slab trenches followed by non-shrink high-strength epoxy grouting to ensure zero rail deflection under dynamic wheel loads.
Yes. All beam profiles, connector brackets, and frame depths are tailored to your target pallet types. For Euro pallets, we specify 1,000mm to 1,100mm frame depths with standard 2,700mm clear beam spans for 3-pallet configurations, accounting for required 75mm side clearances per EN 15620 guidelines.
Our mobile carriages feature redundant safety systems: full-length optical safety light curtains at the base and waist height, emergency push-button bars on carriage endpoints, acoustic-optical move indicators, and ultrasonic chassis proximity sensors that arrest all motor drive operations within 150 milliseconds upon obstruction detection.
Production for standard project volumes (2 to 8 40-foot HQ shipping containers) spans 15 to 25 calendar days. Ocean freight from Guangzhou / Shenzhen port takes approximately 28 to 35 days to European main base ports (Rotterdam, Antwerp, Hamburg) and 18 to 24 days to US West Coast ports (Long Beach, Oakland).
Yes. Approximately 40% of our production volume serves international racking brands, distributors, and material handling systems integrators. We provide private-label branding, custom punch profiles (including teardrop, hex, and diamond slots), customized RAL powder-coat matchmaking, and non-branded or distributor-branded installation manuals.
Submit your architectural floor plan, ceiling clear height, and pallet payload parameters. Our engineering department will supply a complete 2D/3D CAD layout, load compliance calculation, and direct wholesale quotation within 24 business hours.