ENGINEERING PORTFOLIO
High-Density Industrial Storage Systems & Racking Configurations
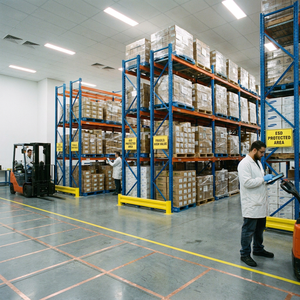
Explore heavy-duty, certified industrial racking solutions tailored for global logistics facilities, cold storage chains, and high-density pallet warehousing operations.
STRUCTURAL MECHANICS & AUTOMATION
Engineering Architecture of Radio Shuttle Racking Systems
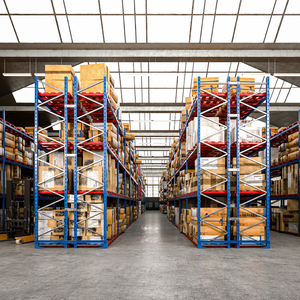
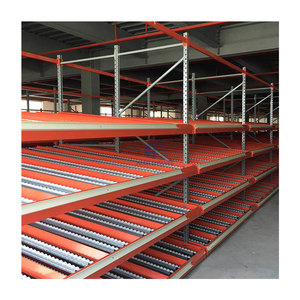
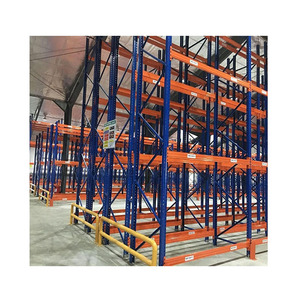
In the landscape of modern supply chain engineering, maximizing the volumetric storage ratio ($\text{Storage Capacity} / \text{Gross Cubic Volume}$) without compromising retrieval velocity represents a primary operational challenge. A Radio Shuttle Racking System—also categorized as an independent semi-automated pallet runner system—is a high-density compact storage solution where an electrically powered, radio-controlled shuttle car travels along internal running rails within continuous storage tunnels to transport pallets smoothly between the front working aisle and deep storage locations.
Unlike static drive-in or drive-through racking configurations, the forklift truck does not physically penetrate the interior storage lanes. Instead, material handling operators position the radio shuttle vehicle into the target tunnel at the designated vertical level using conventional counterbalance, reach, or articulated forklifts. Pallets are then deposited at the lane entry, where the battery-driven shuttle lifts the pallet through an electromechanical or hydraulic lifting platform and relocates it autonomously deep into the channel. This mechanical segregation completely eliminates forklift-structure collision incidents, dramatically diminishing structural fatigue, upright twisting, and catastrophic rack frame failure while lowering handling turnaround times by up to 50% compared to traditional drive-in racking operations.
| System Attribute | Radio Shuttle Racking | Drive-In Racking | Standard Selective Pallet Rack | Automated AS/RS Crane System |
|---|---|---|---|---|
| Storage Density Efficiency | Ultra-High (Up to 85%) | High (65% - 75%) | Low (35% - 45%) | Maximum (85% - 92%) |
| Operating Paradigm | Both FIFO & LIFO Supported | Strictly LIFO (FIFO requires drive-through) | 100% Direct Accessibility | Full Autonomous Integration |
| Forklift Impact Risk | Near Zero (Operates external to channels) | High (Vehicles drive inside bays) | Moderate (Aisle collisions) | Zero (Fully automated) |
| Operational Cycle Velocity | 0.8 m/s – 1.1 m/s (Fast autonomous shuttling) | Slow (Cautious vehicle maneuvering) | High direct picking rate | Variable continuous high-speed |
| Cold Storage Feasibility | Optimal (-30°C with heated LiFePO4 cells) | High structural maintenance cost | Low volumetric energy efficiency | High initial sensor maintenance |
| Capital Expenditure (CapEx) | Moderate (Rapid 14–22 month ROI) | Low Initial / High Maintenance | Lowest Baseline | Extremely High (Multi-million) |
From a structural metallurgy and design standpoint, our cold-formed upright columns and load-bearing beams are manufactured from certified Q235B and Q355B structural carbon steel, rigorously engineered to satisfy European Standards EN 15512:2020 (Steel static storage systems – Adjustable pallet racking systems – Principles for structural design) and EN 15620 (Tolerances, deformations and clearances). The custom-engineered continuous shuttle rail profile is cold-rolled with integrated positioning indexing stops, dual-edge anti-tipping guide lips, and optical positioning notches, ensuring steady linear guidance and micron-level positioning precision for industrial shuttle carts.
Structural Galvanized Rail Guides
Continuous heavy-duty zinc-coated or powder-coated roll-formed runners serve both as structural tie-beams and vehicle tracks, withstanding 1500kg dynamic pallet impact forces.
Intelligent PLC & Optical Sensors
Multi-sensor logic, laser distance finders, and CAN-bus industrial controllers prevent rack collisions, detect irregular pallet overhang, and optimize acceleration profiles.
LiFePO4 Power Management
High-discharge lithium iron phosphate battery packs yield 8 to 10 hours of continuous operation per single charge, featuring integrated thermal jackets for -30°C cold stores.
MARKET INSIGHTS & EVOLUTION
Future Procurement Trends & Technology Roadmap (2025–2030)
Procurement strategies among international supply chain operators are evolving rapidly from basic static steel frame procurement toward intelligent, scalable semi-automation. Corporate real estate pressures, soaring land-acquisition expenses, escalating warehouse thermal conditioning power costs, and regional labor shortages across Europe, North America, and the Middle East are shifting capital investments toward deep-lane shuttle technology.
1. 2D to 4D Multi-Directional Transit
Transition from conventional 2-way lane shuttles to 4D multi-directional shuttles capable of traversing both lane rails and lateral transfer beams, eliminating manual forklift repositioning entirely.
2. Open Architecture WMS/WCS Integration
Global procurement heads now demand non-proprietary API interfaces. Shuttles are controlled through standard industrial tablet Wi-Fi, industrial RF gateways, or direct connection with SAP and Manhattan WMS platforms.
3. Green Cold Chain Subsidies
High-density shuttle architectures shrink refrigerated air volume by 35% to 45% compared to selective aisle layouts, lowering utility kWh demand and qualifying projects for international green warehouse certifications.
4. Pre-Engineered Modular Scalability
Procurement teams increasingly prefer standard modular bays that can be initially deployed in semi-automated shuttle mode and subsequently upgraded to full automated pallet lifts and mother-child AGV systems without structural demolition.
SOURCE MANUFACTURER VALIDATION
Enterprise Strengths & Factory Direct Export Competence
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. stands as one of China's premier heavy-duty warehouse storage rack designers, engineers, and exporters. With over 25 years of specialized manufacturing experience, our modern production base spans more than 30,000 square meters in Guangdong, manned by 300+ skilled technical craftsmen and structural engineers. We maintain an independent monthly production capacity exceeding 30,000 tonnes of certified structural steel racking.
HEDA Shelves has completed over 10,000 turn-key warehouse engineering projects across 120+ countries and territories worldwide, including key markets across Germany, the Netherlands, France, Poland, the United Kingdom, the Americas, Australia, and Southeast Asia. We eliminate intermediate trading layers by providing direct factory-to-port and DDP engineering deliveries, saving European and international distributors 20% to 35% in direct procurement overheads while maintaining rigorous European compliance benchmarks.
2001
Established Year (25+ Years Experience)
30,000m²
Factory Floor Area & Rolling Mills
30,000t
Monthly Structural Steel Capacity
10,000+
Completed Global Storage Projects
Verified CE & ISO Credentials
Official CE Factory Production Control (Certificate No. 2435-CPR-8605159) and certified Quality Management System under ISO 9001:2015 (No. 18624Q00169R0M), meeting strict European standards.
Free 3D & CAD Layouts
Our dedicated structural engineering division furnishes DWG floor layouts, finite element analysis (FEA) deflection models, and 3D warehouse simulations within 24–48 hours at zero cost before order confirmation.
Full OEM/ODM Private Labeling
We engineer custom profiles, punch hole geometries (teardrop, hex, or diamond pitch 50mm/75mm), custom RAL architectural powder-coat shades, and branded packaging for regional racking systems integrators.
Automated Surface Pretreatment
Automated 10-step pickling, phosphating, and electrostatic powder coating line delivers a smooth 60–80 micron cured polyester epoxy film resisting scratch, acid, and salt fog deterioration.
PROCUREMENT INTELLIGENCE
Frequently Asked Questions on Radio Shuttle Racking Procurement
Essential technical, operational, and commercial answers for project engineers, procurement directors, and warehouse operations managers.
Can HEDA radio shuttle racking accommodate mixed Euro (1200x800mm) and Industrial (1200x1000mm) pallets?
Yes. Our shuttle running rail assemblies and shuttle chassis are engineered with adjustable guide wheel flanges and variable pallet bottom skids. During the initial CAD and structural design phase, we specify customized rail width spacing and lateral guide entry funnels that safely handle EUR 1 (1200 × 800 mm), EUR 2 (1200 × 1000 mm), US Standard 48 × 40-inch GMA pallets, or custom industrial plastic runners without requiring physical rail realignments.
How do the lithium shuttle batteries perform in sub-zero cold storage facilities (-25°C to -30°C)?
For cold room and deep-freeze facilities, HEDA Shelves equips shuttle vehicles with low-temperature rated Lithium Iron Phosphate (LiFePO4) battery packs containing built-in internal heating circuits (PTC heat jackets), sealed IP65 electronic enclosures, and low-temperature synthetic lubricants. This prevents battery capacity drops and electrolyte crystallization, ensuring reliable 8-hour continuous cycle shifts before swap-out or fast recharging.
What warehouse floor slab specifications and load-bearing capacities are required?
Because radio shuttle racking concentrates multiple pallet loads in continuous deep vertical blocks, concentrated upright point loads typically range between 5,000 kg and 14,000 kg per baseplate. The concrete floor slab should adhere to DIN 18202 Table 3 flatness standards with a minimum compressive strength of C25/30 or C30/37 and a thickness of 180mm–250mm, reinforced with welded wire mesh or structural steel fibers. Our structural engineering team provides precise baseplate loading calculation sheets to present to your civil building contractor.
What is the production lead time, and how is sea freight to European and global ports organized?
Standard manufacturing duration for a 500 to 3,000 pallet position radio shuttle project is typically 20 to 30 working days from drawing sign-off and deposit receipt. Shipping from our Guangzhou factory to primary European destination ports (such as Rotterdam, Hamburg, Antwerp, Valencia, Felixstowe) takes roughly 28 to 35 transit days. Products are packed with protective steel dunnage, corrugated cardboard guards, plastic wrap, and steel strapping to eliminate transit abrasions inside sea containers.
What structural calculations and compliance documentation are provided for local building inspectors?
Every export project is accompanied by a full technical dossier, including static load calculation reports referencing EN 15512 and FEM 10.2.02 methodology, assembly layout diagrams with clear load-sign designations, CE Factory Production Control Certificate No. 2435-CPR-8605159, ISO 9001:2015 certification, and steel mill test certificates (MTC) proving Q235B/Q355B chemical composition and yield tensile strength.
Do you provide installation supervision and after-sales maintenance support overseas?
Yes. We provide complete step-by-step 3D exploded assembly diagrams, labeled part schematics, and high-definition video walkthroughs. For larger projects across Europe, the Americas, and Southeast Asia, HEDA Shelves can deploy experienced English-speaking structural installation supervisors to direct your local rigging crew. In addition, all shuttle cart electronic components and motors come with a 12-month replacement warranty and lifetime remote engineering troubleshooting.
Plan Your High-Density Warehouse with HEDA Engineering
Submit your warehouse DWG floor plan, ceiling clear heights, and pallet specifications. Our certified structural engineers will deliver a free 3D simulation, CAD layout, and factory-direct wholesale quotation within 24 hours.
Send an Inquiry