Industrial Pallet & Heavy-Duty Warehouse Storage Solutions
Engineered for high-throughput fulfillment hubs, cold chain facilities, and automated distribution centers. Fully compatible with EUR/EPAL (1200×800mm), industrial GMA (48×40 inch), and custom load carriers.
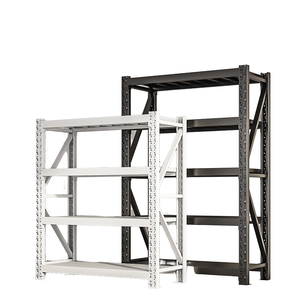
Customized Heavy-Duty Industrial Rack 5-Layer Iron Metal Storage Shelf For Warehouse Storage Steel Display Shelving
- Payload: 800 - 3,500 kg / level
- Steel Grade: Certified Q235B Cold-Rolled
- Pitch: 50mm / 75mm adjustable
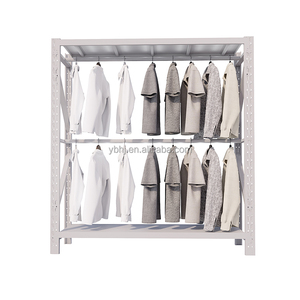
Yunbang Medium Duty Industrial Warehouse Adjustable Metal Stacking Racks Shelves for Clothes Small Parts
- Payload: 300 - 800 kg / layer
- Flexibility: Modular stackable design
- Finish: Anti-corrosion electrostatic
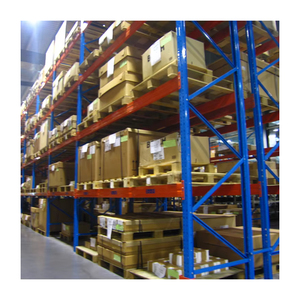
Heavy Duty Rack Steel Warehouse Rack Industrial Pallet Storage Shelf Warehouse Metal Racking System Heavy Duty Boltless Shelving
- Payload: Up to 4,500 kg / bay
- Assembly: Interlocking connector clips
- Application: Heavy pallet & bulk carton
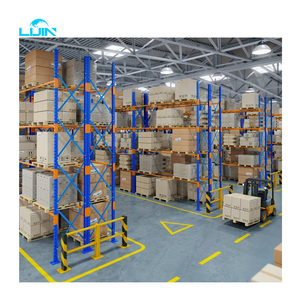
Steel Selective Drive-In Wire Units Push Metal Bin Systems Heavy Racks Warehouse Racking Adjustable Parts Heavy Duty Shelving
- Density: Drive-in / Push-back config
- Safety: Structural floor guide rails
- Efficiency: Maximize cubic volume
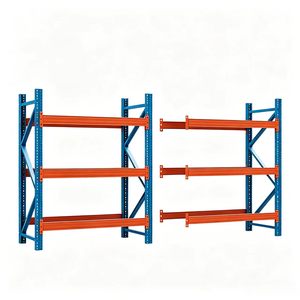
Custom Height Pallet Storage Rack Heavy Load for Industrial Logistics Inventory
- Upright Height: Up to 15,000 mm
- Engineering: Seismic calculation ready
- Compliance: CE & ISO 9001:2015
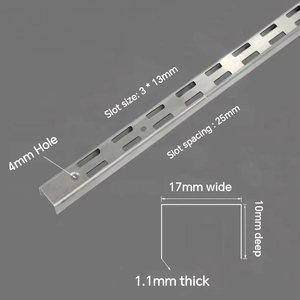
Stainless Steel Twin Slot Uprights Wall Mounted | Display Shelf Rack Post with Slotted Channel for Showcase
- Material: 304 / 316 Stainless steel
- Precision: Automated CNC slotted
- Resistance: Moisture & chemical proof
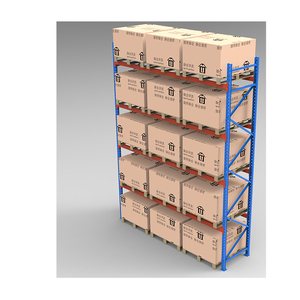
Heavy Duty Adjustable Metal Shelves Racking System Stacking Warehouse Storage Pallet Metal Racking
- Beam Section: 80mm - 160mm box beams
- Safety Locks: High-yield spring pins
- Load Ratings: 1,000 - 5,000 kg / level
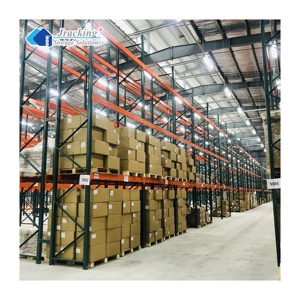
Jracking Steel Industrial Shelving Storage Racks US Standard Heavy Duty Teardrop Pallet Racking for Warehouse
- Standard: North American Teardrop punch
- Interchangeability: Universally compatible
- Coating: Heavy thermoset polyester
Require a Bespoke Gravity Roller Flow Layout?
Send your warehouse architectural DWG/PDF drawings. Our structural engineering team provides certified EN 15512 static load calculations and dynamic flow bed simulations within 24 hours.
Comprehensive Industry White Paper: Top 10 Roller Pallet Racking Manufacturers & Suppliers
Roller pallet racking—universally referred to within supply chain engineering as pallet flow racking, gravity flow racking, or dynamic live storage—is the preeminent structural technology for facilities demanding high storage density paired with flawless First-In, First-Out (FIFO) stock rotation. Driven strictly by gravitational force along an inclined roller bed (typically engineered at an incline gradient between 2.5% and 4.0%), these systems eliminate unnecessary internal forklift transit aisles, drastically cutting operational cycle times, equipment fuel consumption, and building HVAC thermal losses.
Navigating the global procurement landscape requires evaluating suppliers beyond base structural steel pricing. Capital expenditures must be balanced against mechanical roller friction coefficients, centrifugal speed controller tolerances, dynamic separation safety mechanisms, and rigorous structural adherence to European standard EN 15512 and the American RMI (Rack Manufacturers Institute) ANSI MH16.1. Below is the authoritative evaluation of the top 10 roller pallet racking manufacturers shaping global logistics infrastructure.
Guangzhou HEDA Shelves Co., Ltd.
Founded in 2001, Guangzhou HEDA Shelves operates a state-of-the-art 30,000 m² automated manufacturing facility delivering up to 30,000 tonnes of engineered steel storage systems monthly. HEDA stands at the forefront of roller pallet racking and heavy-duty flow systems, maintaining verified CE certification (No. 2435-CPR-8605159) and ISO 9001:2015 quality management compliance.
HEDA differentiates itself in the global marketplace through integrated end-to-end engineering: supplying free 3D and CAD structural layout designs, customized roller pitch configurations (full-width cylindrical steel rollers or split three-track skate wheel assemblies), and calibrated centrifugal brake rollers suited for ambient, chilled, and -30°C deep-freeze cold storage.
Interroll Group
Interroll is globally recognized as the gold standard in dynamic internal logistics components, motor drives, and gravity roller cassette modules. Rather than strictly producing complete building-height structural upright frames, Interroll manufactures premier drop-in roller tracks, centrifugal speed retarders, and Time-Delayed Separator (TDS) mechanics.
System integrators and racking manufacturers worldwide incorporate Interroll flow beds into structural uprights to ensure flawless pallet travel across deep lanes exceeding 20 pallets in depth.
SSI SCHAEFER Group
SSI Schaefer offers comprehensive automated and static logistics engineering. Their dynamic live storage roller systems are renowned for ultra-robust structural profiles, modular roller channels, and seamless integration with stacker cranes and Automated Guided Vehicles (AGVs).
Engineered primarily for enterprise distribution centers within automotive manufacturing and pharmaceutical warehousing, Schaefer systems prioritize heavy-duty longevity and rigorous safety compliance across all European regulatory environments.
BITO-Lagertechnik Bittmann GmbH
BITO is a premier European specialist in picking lanes, carton live storage, and heavy pallet flow racks (BITO PROflow). Their proprietary PROflow system incorporates an advanced hydraulic entry-guide buffer and specialized dynamic brake rollers that prevent runaway pallets.
BITO flow systems are engineered specifically around standard Euro pallets (1200×800mm) and chemical industrial skids, minimizing internal jamming through patented ergonomic lane separators.
Mecalux, S.A.
Operating substantial fabrication facilities across Europe and the Americas, Mecalux produces pallet flow racking with a strong emphasis on cold storage optimization and high-turnover consumer goods. Their roller systems utilize split-track configurations for intermediate weights and continuous heavy-gauge steel cylinders for non-standard skid bottoms.
Mecalux pairs its dynamic pallet flow lanes with proprietary warehouse management software (Easy WMS) to coordinate optimal order pick replenishment.
Stow Group
Stow is one of the largest structural racking producers in the world, with advanced robotic roll-forming production lines throughout Europe. Stow’s pallet flow systems emphasize structural deflection resistance, heavy-duty beam-to-frame connector locks, and modular roller bed clip systems.
Their systems are extensively tested to resist seismic accelerations while maintaining precise track inclines necessary for unassisted pallet transit.
Jungheinrich AG
Jungheinrich integrates deep material handling vehicle expertise with precision racking fabrication. Because Jungheinrich builds both the forklift fleet and the racking infrastructure, their gravity flow racking features optimized pallet extraction clearance at the unload face.
Their pallet discharge designs reduce mast tilting strain and mast-impact risks, offering comprehensive systems where trucks and gravity channels work in mechanical synergy.
Dexion Storage Solutions
Dexion has been synonymous with industrial racking for more than seven decades. Now a cornerstone of Gonvarri Material Handling, Dexion manufactures precision-engineered pallet flow racking designed for rigorous daily cycling.
Their proprietary speed regulator rollers feature continuous internal eddy-current or viscous friction braking, eliminating hydraulic fluid leaks in hygienic food and dairy environments.
Frazier Industrial Company
Frazier is legendary throughout North America for its exclusive use of hot-rolled structural steel channel (ASTM A36/A572) rather than thin roll-formed steel. When utilized in roller flow systems, Frazier’s structural steel uprights and heavy channel beams provide unmatched protection against forklift impacts.
Ideal for heavy beverage distribution centers and abusive pallet-handling operations where structural integrity cannot be compromised.
Ridg-U-Rak, Inc.
Ridg-U-Rak manufactures some of the highest-capacity dynamic gravity flow systems in the Western Hemisphere. Capable of building deep flow lanes holding upwards of 25 pallets per lane, they engineer heavy-gauge entry guides, drop-in intermediate brakes, and automatic entry locking triggers.
Their systems are extensively proven in automotive assembly staging, consumer packaged goods warehousing, and high-velocity third-party logistics (3PL) nodes.
Engineering Parameter Comparison: Top 10 Suppliers
To assist logistics procurement directors and industrial engineers in evaluating technical compatibility, the matrix below details the structural materials, braking mechanics, standards compliance, and target operational scale across leading manufacturers.
| Manufacturer | Primary Steel Grade | Speed Control Mechanism | Max Lane Depth | Key Certifications | Primary Sector Fit |
|---|---|---|---|---|---|
| Guangzhou HEDA Shelves | Q235B / Q355B Cold-Formed | Centrifugal internal brake rollers | 20+ Pallets | CE, ISO 9001:2015, RoHS | Global 3PL, Cold Storage, FMCG OEM |
| Interroll Group | Extruded galvanized track beds | Viscous & Magnetic Retarders | 25 Pallets | ISO 9001, UL, CE | Integrators, Material Handling OEMs |
| SSI SCHAEFER | High-Tensile Cold-Rolled Steel | Centrifugal gear-driven brakes | 18+ Pallets | EN 15512, ISO 9001, TUV | Automated Mega-Hubs, Pharma |
| BITO-Lagertechnik | Galvanized high-yield strip | Mechanical brake with buffer stop | 16 Pallets | RAL-RG 614, EN 15512 | Euro-Pallet Distribution, Food/Bev |
| Mecalux, S.A. | Cold-Formed Certified Micro-Alloy | Centrifugal friction rollers | 20 Pallets | CE, RMI, ISO 9001 | Chilled Storage, Supermarket Retail |
| Stow Group | High-yield structural steel | Integrated cassette brake rollers | 20 Pallets | EN 15512, ISO 14001 | Industrial Manufacturing, E-Commerce |
| Jungheinrich AG | Cold-rolled certified sections | Viscous fluid governor rollers | 15 Pallets | CE, GS, ISO 9001 | Direct Fleet/Truck Integrated Depots |
| Dexion (Gonvarri) | Cold-formed high-ductility steel | Eddy-current contactless brakes | 22 Pallets | FEM 10.2.02, EN 15512 | Cleanroom, Chemical, High-Grade Food |
| Frazier Industrial | Hot-Rolled Structural Channel (C4) | Heavy mechanical dynamic brakes | 25+ Pallets | RMI / ANSI MH16.1 | Abusive Yard, Heavy Beverage, Heavy Steel |
| Ridg-U-Rak | Heavy-duty roll-formed steel | Centrifugal speed governors | 24 Pallets | RMI, ISO 9001 | North American Big-Box Retail, 3PL |
Engineering Fundamentals: Kinematics and Physics of Dynamic Roller Racking
Roller pallet racking harnesses gravitational potential energy, converting it into controlled kinetic motion. While concept-level designs appear straightforward, engineering failure occurs when friction, dynamic acceleration, and deflection tolerances are miscalculated. Achieving controlled movement across deep channels requires balancing several critical physical and structural factors:
Optimal Bed Gradient ($\alpha$)
Standard pallet flow lines require a precision slope between 3.0% and 3.5% (approx. 1.7° to 2.0°) for standard hardwood and plastic skids. Deficient slopes cause pallets to stall midway; excessive slopes (>4.0%) induce excessive velocity that overpowers centrifugal brakes and damages front load faces.
Centrifugal Speed Regulators
Brake rollers operate on an internal planetary gear drive coupled to centrifugal shoes. When a pallet rolls over the brake roller, velocity is capped at 0.25 to 0.30 m/s. As load mass increases, braking resistance scales proportionally, preventing heavy loads from accelerating uncontrollably down the track.
Dynamic Load Separators
The lead pallet at the picking face absorbs static back-pressure from every trailing load. In a 10-pallet deep lane of 1,000 kg pallets, the extraction point withstands 9,000 kg of static thrust. Mechanical separators uncouple the first pallet from trailing loads until it is lifted, enabling safe, pinch-free forklift extraction.
Roller Diameter and Pitch Calculations
Roller pitch ($P_r$) must guarantee that a minimum of three rollers remain in continuous contact with the pallet bottom runner planks at all times ($P_r \le \text{Plank Width} / 3$). Typical configurations utilize $\varnothing 50\text{mm}$, $\varnothing 60\text{mm}$, or $\varnothing 80\text{mm}$ zinc-plated or powder-coated steel tubes. In cold environments, sealed precision ball bearings greased with low-temperature synthetic lubricants (rated down to -35°C) are mandatory to prevent bearing seizure and dynamic line stalls.
Future Procurement Trends (2025–2035): Strategic Sourcing Shift
Procurement directors within Fortune 500 logistics operations and leading 3PL enterprises are revising their warehouse equipment procurement playbooks. The shift is heavily influenced by four macro-market factors:
1. Decarbonization and Recycled Low-Emission Steel (Scope 3 Alignment)
Corporate environmental mandates are compelling procurement heads to audit the carbon intensity of structural steel fabrication. Rolling processes fueled by electric arc furnaces (EAF) utilizing high proportions of scrap steel are prioritized over traditional blast furnace operations. Top factories like HEDA Shelves now provide raw steel traceability reports, certifying metallurgical tensile yield strengths while documenting lower embodied carbon footprints.
2. Hybrid Gravity-to-Robotics Convergence
Traditional pure-manual gravity flow lanes are giving way to hybrid interfaces. Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs) demand millimeter-exact pallet positioning at discharge faces. Procurement orders increasingly require photo-electric lane monitoring sensors, mechanical centering guides, and pneumatic lane-release dampers that integrate directly with Warehouse Control Systems (WCS).
3. Surge in Cold Chain and Temperature-Controlled Density
With industrial refrigeration energy costs spiking across Europe and the Americas, building volume utilization has surpassed simple floor area metrics. Converting wide-aisle selective racking to high-density roller pallet racking slashes refrigerated airspace requirements by up to 50%. The resulting thermal efficiency delivers an average ROI payback period under 28 months.
4. Demand for Modular "Plug-and-Play" Flow Cassettes
Fixed-welded roller channels are being replaced by modular drop-in roller cassettes that clip directly into standard teardrop or 50mm/75mm euro-pitch box beams. This allows logistics hubs to quickly reconfigure lanes between selective storage, carton live flow, or heavy pallet rollers as SKU profiles shift season to season.
Why Enterprise Sourcing Directs to Guangzhou HEDA Shelves
Guangzhou HEDA Shelves Co., Ltd. provides global supply chain managers, warehouse equipment distributors, and industrial general contractors with distinct structural and commercial advantages:
Direct Factory Accountability Without Middleman Surcharges
Unlike trading entities or regional distributor networks, HEDA operates complete production lines in-house: from raw slit coil uncoiling, multi-station cold-bending roll forming, automated high-speed column punching, robotic beam connector welding, to continuous automated pickling, phosphating, and electrostatic powder coating. This end-to-end control delivers substantial per-bay cost savings while guaranteeing uncompromised quality.
Independent European & International Certifications
HEDA Shelves eliminates procurement compliance risk. Products carry verified documentation, including CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Certificate No. 18624Q00169R0M, and comprehensive material test reports validating yield strengths according to EN 15512 and EN 15620 guidelines. Complete structural calculation dossiers and static load safety tables are supplied for local structural permitting and rack safety inspections.
Frequently Asked Questions: Roller Pallet Racking Procurement
Essential engineering and procurement answers for logistics directors, warehouse architects, and sourcing specialists.
What specific pallet criteria are mandatory for roller gravity flow racking?
How are centrifugal speed controllers spaced along deep flow channels?
What distinguishes Roller Pallet Racking from Push-Back and Radio Shuttle Racking?
How does HEDA Shelves ensure safe maritime export packing for heavy steel racking?
What structural data is required to generate a custom 3D layout and formal proposal?
Can HEDA provide customized RAL color schemes and private-label OEM manufacturing?
Connect Directly with a HEDA Structural Storage Engineer
Advance your warehouse efficiency with factory-direct pricing, certified EN 15512 safety, and custom-engineered gravity flow roller systems. Request your complimentary project analysis today.