Heavy Industrial Racking & Material Handling Equipment
Manufactured with high-tensile cold-rolled steel, high-micron electrostatic powder coating, and precision CNC punchings tailored to regional warehousing specifications.
Why Double Deep Pallet Racking Dominates Modern Warehousing in Kuwait
In the contemporary logistics ecosystem of Kuwait, industrial warehouse footprint is under unparalleled economic pressure. From the central trading arteries of Shuwaikh Industrial Area and Al Rai to the strategic food logistics hubs in Sulaibiya and the heavy industrial complexes of Mina Abdulla and Shuaiba, the cost of industrial land acquisition and ongoing facility operations has surged. Consequently, supply chain directors and structural engineering consultants are forced to maximize volumetric cube efficiency without ballooning capital expenditure into full-scale, energy-intensive automated AS/RS facilities.
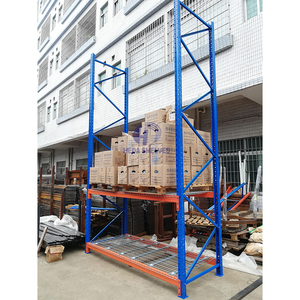
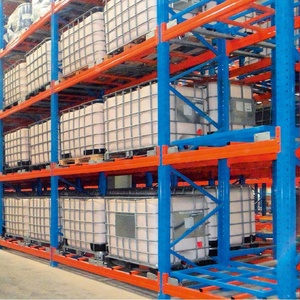
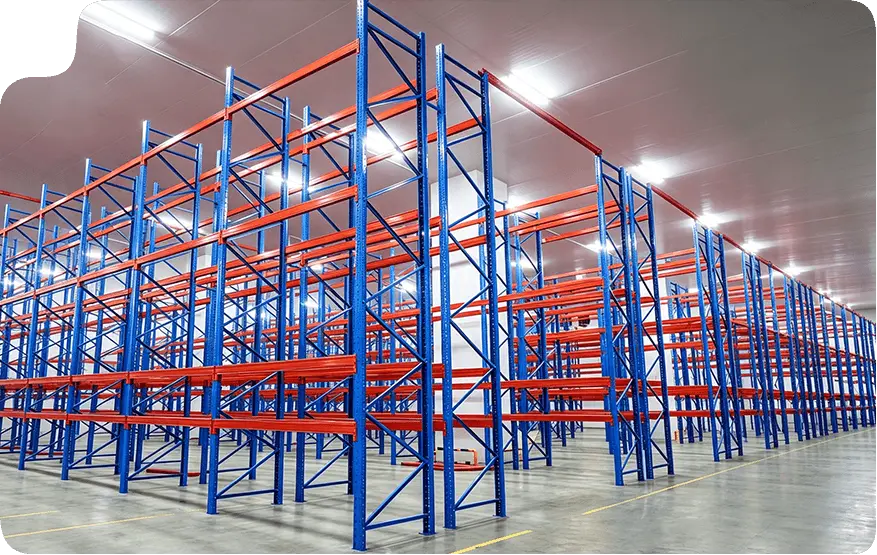
Double Deep Pallet Racking systems have established themselves as the mathematically optimized middle-ground between single-selective pallet accessibility and high-density, multi-lane storage. By eliminating 50% of the interior access aisles required by standard selective configurations, a double deep system places two pallet positions back-to-back within a single bay profile. This architectural layout immediately delivers an up to 40% to 50% increase in storage volume across the identical building floor plate, drastically lowering the amortized operational cost per pallet position.
Adapting Structural Storage to Kuwait's Environmental and Operational Constraints
Exporting structural steel systems into the Arabian Gulf demands rigorous attention to environmental stressors that western European or temperate-zone storage designs rarely encounter. The climatic realities of the State of Kuwait represent an engineering benchmark: ambient external temperatures regularly surpass +50°C during peak summer months, triggering substantial thermal gradients across non-air-conditioned warehouse envelopes and exacerbating thermal expansion within steel frames.
Furthermore, pervasive airborne particulates from seasonal Shamal sandstorms penetrate deep into industrial facilities. These micro-abrasive mineral dusts can settle on horizontal beam ledges, jam low-tolerance moving mechanisms, and wear away inferior painted surfaces. As an established direct-factory exporter, our Double Deep Pallet Racking is constructed using high-yield structural hot-rolled coil that undergoes computerized cold-roll profile forming, followed by a rigorous 10-stage chemical pre-treatment and an ultra-tough electrostatic powder coating (60–80 microns thick) that guarantees long-term chemical, UV, and mechanical scuff resistance.
| Racking Architecture | Storage Density Ratio | Direct Pallet Selectivity | MHE (Forklift) Equipment Required | Kuwait Industry Suitability |
|---|---|---|---|---|
| Standard Selective Racking | Baseline (100%) | 100% Immediate Direct Access | Standard Counterbalance / Reach Truck | Retail Picking, High-SKU / Low-Volume Stock |
| Double Deep Pallet Racking | High (+40% to 50%) | 50% Direct Access (2-Deep Filo) | Pantograph Double-Reach / Telescopic Mast | Cold Storage, FMCG, Beverage, 3PL Distribution |
| Drive-In / Drive-Through | Maximum (+65% to 75%) | Low (Lane-dependent LIFO/FIFO) | Standard Counterbalance (Enters Rack) | Seasonal Agricultural Inflow, Raw Bulk Materials |
| Push-Back Trolley Racking | Medium-High (+30% to 40%) | 2 to 5 Pallets Deep LIFO | Standard Reach Truck | Fast-Moving Consumer Goods with Moderate Batches |
Targeted Deployment Across Kuwait's Key Industrial Zones
From temperature-controlled perishables along the Sixth Ring Road to oilfield consumables in the south, our export engineering accommodates distinct localized warehouse operational profiles.
Sulaibiya Cold Storage Hub
Because Kuwait imports roughly 85% of its national nutritional consumption, refrigerated and deep-freeze cubic meterage in Sulaibiya is the country's most valuable storage space. Our double deep racking cuts HVAC energy dissipation per pallet position by 38% through compact thermal-mass concentration.
Shuwaikh & Al Rai Wholesale
Characterized by restrictive urban ceiling heights (6m to 9m clear height) and high rental premiums per square meter. Our double deep systems allow central retail distributors and FMCG wholesalers to double their stock capacity without moving out of inner-city distribution radii.
Mina Abdulla Petrochemical Spares
Serving downstream refining operations, engineering contractors, and drilling spares storage. Equipped with structural pallet support bars, reinforced heavy-duty box beams, and front-entry upright column protectors to endure massive heavy components and aggressive rough-service forklift transit.
Airport Free Zone & 3PL Hubs
Bonded air cargo consolidation centers requiring tight cycle inventory turnover. Double deep layouts match paired SKU batches effortlessly: when standard shipping manifests feature 2 to 4 pallets per SKU, front-to-back storage provides direct accessibility without reshuffling delays.
Cold-Formed High-Tensile Steel Engineered to EN 15512 Standards
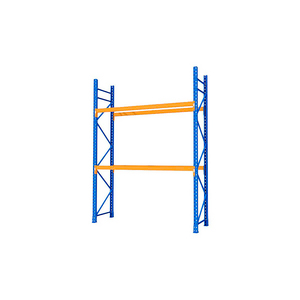
Every double deep pallet rack manufactured in our 30,000 m² factory is engineered around strict deflections limits (L/200 under maximal working loads). Because reach trucks with extended pantographs or telescopic tines exert eccentric moment forces when accessing the rear pallet position, our frames are designed with wider Omega (Ω) upright profiles and heavier gauge horizontal and diagonal truss bracings.
-
High-Yield Q235B & Q355B Steel: Sourced from top-tier primary mills, ensuring zero impurities and superior ductility under cyclical loading.
-
50mm Continuous Pitch Punching: CNC-punched uprights allow millimetric beam height adjustability to match Kuwait's standard 1200×1000mm and 1200×800mm pallet stacks.
-
Integrated Pallet Support Guide Bars: Structural guide rails welded to beam profiles ensure the rear pallet is loaded at the proper level without risk of edge slipping.
-
Seismic and Soil Settlement Anchoring: Kuwait's coastal and desert ground strata can be prone to localized slab differential settlement; our enlarged 10mm steel baseplates and chemical floor anchors distribute point loads safely.
Forklift Fleet Compatibility: Operating Pantograph & Telescopic Reach Trucks
A successful Double Deep Pallet Racking installation relies completely on the synchronized engineering between the racking structure and the material handling fleet operating within the aisles. In the Kuwait market, warehouse operators typically deploy one of two specialized MHE configurations:
Pantograph Reach Trucks
Featuring a scissor-like mechanical pantograph mechanism that extends the carriage outward into the second pallet position. Highly popular in GCC distribution centers for their versatility across varied mast heights.
Telescopic Fork Reach Trucks
Utilizing hydraulic extending outer fork tines to retrieve the second-depth load. Requires less deadweight counterbalancing at height, making it an excellent match for high-bay warehouses over 9 meters in height.
Camera & Laser Alignment Systems
At lift elevations exceeding 7 meters, operators cannot visually judge fork entry into the rear pallet runners. We engineer our beam levels to work with carriage-mounted camera feeds and laser tine guides, virtually eliminating rack impacts.
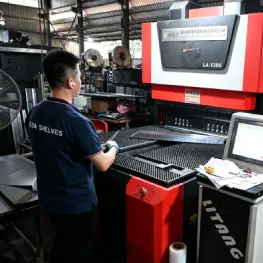
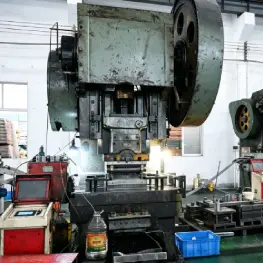
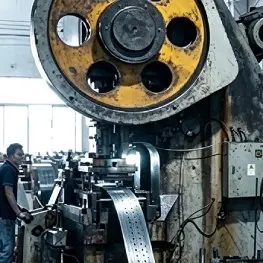
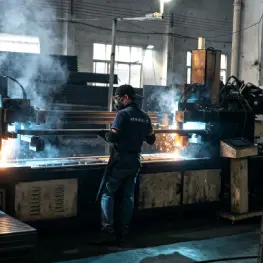
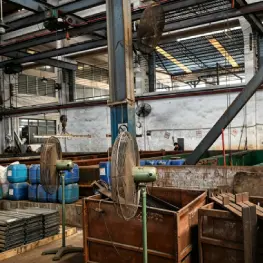
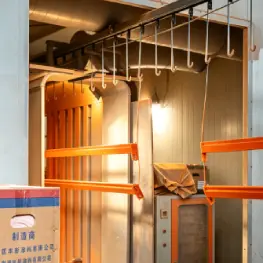
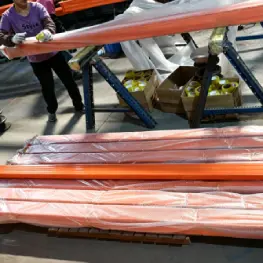
Our 10-Step Precision Industrial Fabrication Workflow
Every component shipped to Kuwait undergoes closed-loop quality control at our Guangzhou manufacturing facility, ensuring flawless on-site bolting and long-term structural integrity.
HEDA Shelves: 25+ Years of Export Manufacturing Authority
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into one of Asia's most prominent manufacturers of high-density warehouse racking and automated storage solutions. Spanning over 30,000 square meters of production plant with more than 300 experienced technical and engineering professionals, our monthly production capacity reaches 30,000 tonnes.
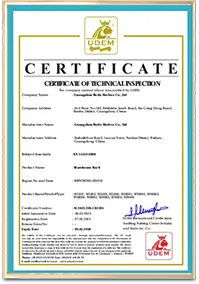
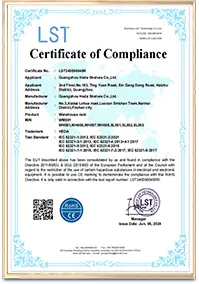
For Kuwaiti EPC general contractors, logistics developers, and commercial procurement departments, working directly with our factory guarantees verified mill test certificates, certified EN 15512 static load calculations, and compliant documentation for municipal inspection approval under the Public Authority for Industry (PAI) and KUCAS clearance.
-
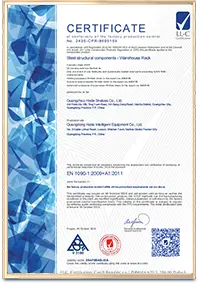
CE Factory Production Control: Certified under CE No. 2435-CPR-8605159 for structural steel components.
-
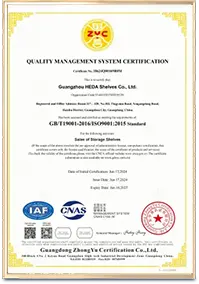
ISO 9001:2015 Management: Registered certification No. 18624Q00169R0M covering design, fabrication, and export testing.
-
Export Track Record: Over 10,000 storage projects engineered and shipped across 120+ countries worldwide.
Frequently Asked Questions for Kuwaiti Storage Projects
Direct answers addressing customs documentation, climatic engineering, MHE requirements, and turnkey ocean delivery into Shuwaikh Port.
How does a Double Deep racking layout compare to Single-Selective in warehouse density?
What forklift machinery is required to operate a Double Deep Pallet Rack in Kuwait?
How do your steel racking finishes withstand Kuwait's high ambient heat and sandstorm dust?
Can your double deep systems support non-standard Kuwaiti plastic and wooden pallets?
What documents are provided for Kuwait Customs clearance and PAI/KUCAS compliance?
What is the expected production and shipping lead time from Guangzhou to Kuwait?
Do you offer on-site installation support in Kuwait?
Request a Free DWG Layout & Static Load Calculation
Send our senior engineering team your warehouse architectural floor plans, ceiling clearances, pallet dimensions, and handling equipment specs. Receive an optimized 2D/3D CAD design proposal within 24 hours.