FMCG & Garments
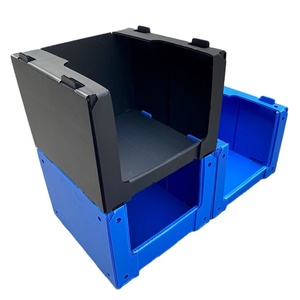
Precision-manufactured in our certified automated facility, each system is engineered around UK Standard (1200 x 1000 mm) and Euro (1200 x 800 mm) pallet footprints to maximise vertical volumetric efficiency.
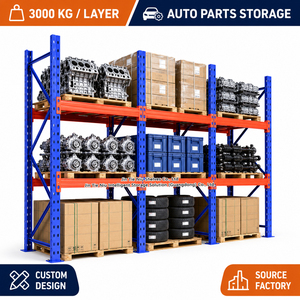
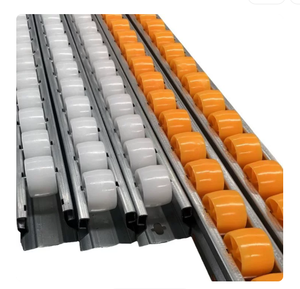
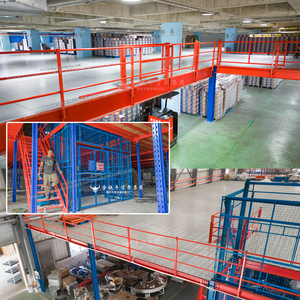
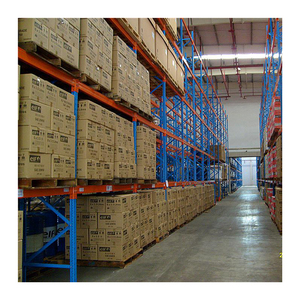
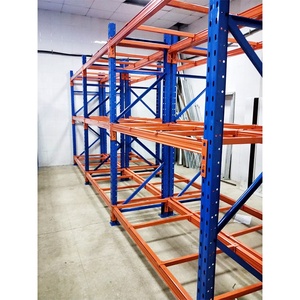
The commercial warehousing environment in the United Kingdom has undergone a fundamental transformation over the last five years. Prime industrial rents across the "Logistics Golden Triangle" of the East and West Midlands—including key transport nodes in Northamptonshire, Leicestershire, Warwickshire, and along the M1/M6 corridors—have escalated past £11 to £16 per square foot. Concurrently, regional fulfillment hubs surrounding London, Greater Manchester, and the South East face stringent greenbelt restrictions that restrict lateral site development.
In response, logistics engineering directors and operational planners are compelled to seek maximum volumetric utilization (m³) rather than mere floor footprint (m²). Standard wide-aisle pallet racking layouts that surrender up to 60% of slab surface area to forklift transit lanes are rapidly giving way to Very Narrow Aisle (VNA) systems, semi-automated Radio Shuttle lanes, and multi-tier mezzanine floor integrations.
In the UK, racking systems are governed strictly by the Health and Safety at Work etc. Act 1974 via the Storage Equipment Manufacturers' Association (SEMA) Codes of Practice and the British Standard BS EN 15512:2020. UK facilities directors require precise finite element load calculations, structural steel resilience against forklift impact, and clear deflection thresholds under British climatic and seismic design criteria.
Guangzhou HEDA Shelves bridges the gap between premium global steel fabrication economies and meticulous UK compliance. By manufacturing from certified high-tensile structural coil steel (Q235B and Q355B equivalent to S235JR and S355JR under European grading), HEDA provides direct factory supply that eliminates middleman price escalations while delivering fully traceable, CE-certified (No. 2435-CPR-8605159) structural profiles tailored specifically for British distribution facilities.
| System Architecture | Density Level | Pallet Access | Aisle Requirement | UK Market Application |
|---|---|---|---|---|
| Wide Aisle APR | Baseline (1.0x) | 100% Direct | 2.8m – 3.2m | General 3PL & Multi-SKU |
| Narrow Aisle (VNA) | High (+45%) | 100% Direct | 1.6m – 1.8m | Midlands High-Bay DCs |
| Double Deep | High (+35%) | 50% Direct (LIFO) | 3.0m | Wholesale & Manufacturing |
| Radio Shuttle | Ultra (+85%) | Lane Access (FIFO/LIFO) | Forklift Free Lanes | Cold Stores & Ambient FMCG |
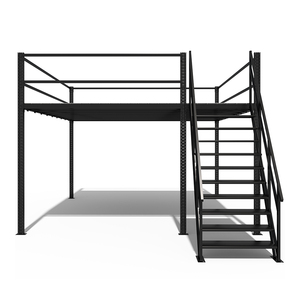
| Rack Mezzanine | Multiplies Floor | Full Hand-Picking | Manual / Trolley | Fashion & Retail E-Commerce |
Every British distribution centre operates under distinct product handling constraints. Explore how HEDA Shelves tailors load-bearing infrastructure to withstand the daily operational demands of UK industry.
Operating within Daventry International Rail Freight Terminal (DIRFT), Magna Park Lutterworth, and Milton Keynes, contract logistics providers juggle thousands of fluctuating SKUs for multinational clients. High-bay APR and VNA racking systems must provide instant pallet selectivity while withstanding continuous 24/7 dual-shift reach truck cycling.
Energy costs per cubic metre in UK cold stores (operating at -18°C to -25°C) represent the highest overhead category outside labor. In facilities across Yorkshire, Humberside, and Wisbech, Drive-In and semi-automated Radio Shuttle racking systems compress chilled air volume by eliminating working aisles, slashing refrigeration requirements.
With the UK boasting one of the highest online retail penetration rates in Europe, parcels require high-density split-case picking. Rack-supported multi-tier mezzanine floors and carton flow picking bins maximize clear ceiling heights, separating pallet replenishment at lower levels from manual multi-trolley order pickers on timber or grating decks above.
Strategic infrastructure investments must account for shifting UK safety standards, labour market challenges, and supply chain automation.
Autonomous mobile robots demand tighter floor tolerance (BS EN 15620 Class 300) and precision bottom-beam clearances for robotic low-profile pallet lifters operating in British fulfillment centres.
UK building frameworks increasingly scrutinise Scope 3 embodied carbon. Direct factory shipments from continuous energy-efficient electric-arc or optimized blast furnace coils cut carbon transit steps.
With UK land supply constricted, warehouses prefer upgrading brownfield sites via heavy structural mezzanines, effectively doubling internal floor area without incurring planning permission delays.
Insurance underwriters in the UK now routinely mandate annual SEMA Approved Racking Inspector (SARI) surveys. System components must retain genuine structural compliance documentation and load plaques.
Guangzhou HEDA Shelves Co., Ltd. operates a flagship 30,000 m² heavy industrial production base equipped with automated roll-forming lines, robotic CNC beam welding, and multi-stage pre-treatment powder coating plants. With an output capacity exceeding 30,000 tonnes per month, we engineer complete systems for direct export to UK ports including Felixstowe, London Gateway, Southampton, and Liverpool.
Unlike local UK racking traders who add 25% to 40% margin on subcontracted steel, HEDA provides direct mill-to-project accountability. We deliver turnkey CAD layouts, complete load tables aligned with BS EN 15512, and comprehensive engineering documentation ready for immediate building inspector review.
Every upright column, box beam, and bracing channel is manufactured under uncompromising ISO 9001:2015 traceability protocols.
Supply your warehouse DWG floorplan or simple dimensions, and our senior engineering team will return a 3D visual CAD layout, bay loading calculations, and a transparent FOB/CIF UK quotation within 48 hours.
Speak directly with our senior racking applications engineers to discuss custom upright profiles, seismic base plates, or VNA floor guidance rails.