Factory-Direct Heavy-Duty Racking Systems
Precision cold-rolled profiles engineered for high-density logistics, automotive buffer stores, and manufacturing warehouses across Slovakia and Central Europe.
Drive-Through vs Drive-In: Kinematics and Structural Mechanics
Demystifying high-density warehouse storage systems within the Central European automotive manufacturing and logistics cluster.
1. Kinematic Principles: True First-In, First-Out (FIFO) in High Density
In warehouse logistics nomenclature, Drive-In Racking and Drive-Through Racking are frequently conflated. However, their structural behavior and operational logic diverge fundamentally. Drive-In racking operates strictly on a Last-In, First-Out (LIFO) protocol: material handling equipment (MHE) enters and exits through the same aisle aperture, making the rack bank a closed-end cul-de-sac. This design utilizes rear structural cross-bracing to resist horizontal longitudinal forces.
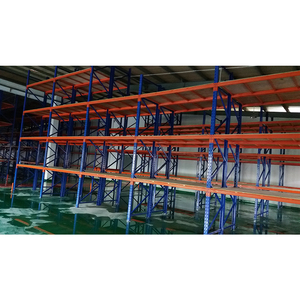
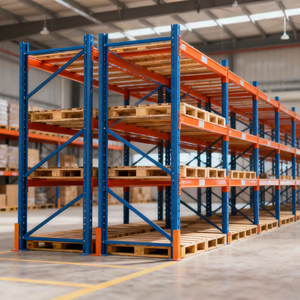
Conversely, Drive-Through Racking provides dual-sided accessibility: forklifts deposit palletized unit loads from the loading face (input aisle) and retrieve them from the opposite discharge face (output aisle). This establishes a strictly regulated First-In, First-Out (FIFO) inventory workflow. For industries where shelf-life decay, chemical lot expiration, or automotive Just-In-Sequence (JIS) staging is mandatory, drive-through systems represent the highest volumetric storage efficiency achievable without fully automated ASRS shuttle machinery.
Overhead Portal Bracing
To compensate for absent rear vertical bracing, Drive-Through systems employ box-beam portal framing across the top bays, transmitting dynamic sway loads safely down into the upright columns and anchor points.
Continuous Pallet Support Rails
Roll-formed 3.0mm–3.5mm thick structural angle rails with flared entry horns ensure smooth pallet entry, minimizing edge snagging while providing safe load bearing for EUR-1 (800×1200mm) and EUR-2 (1200×1000mm) pallets.
Heavy-Duty Floor Guide Rails
Floor-anchored C-section or structural angle guides shield uprights from counterbalance and reach truck impact, channeling forklift steering precisely down long interior drive-through corridors.
Slovakia as Central Europe’s High-Density Warehousing Fulcrum
Strategic positioning along the Pan-European corridors and Europe's densest automotive manufacturing matrix.
Industrial Footprint & Geographical Clusters
The Slovak Republic has established itself as an indispensable powerhouse in Central and Eastern Europe's (CEE) industrial fabric. Anchored by the D1 highway corridor spanning from Bratislava through Trnava, Trenčín, and Žilina to Košice, as well as the southern D2 corridor connecting to Brno (Czechia) and Győr/Budapest (Hungary), the country hosts unparalleled manufacturing density.
With major automotive assembly plants including Volkswagen Slovakia (Bratislava), Stellantis (Trnava), Kia Slovakia (Žilina), Jaguar Land Rover (Nitra), and the developing Volvo electric vehicle mega-complex in Valaliky near Košice, storage systems face exacting demands. Warehouses operating in Senec (Bratislava region), Lozorno, and Sereď are not merely static stockpiles; they function as mission-critical sequencing buffers handling massive flows of automotive subassemblies, battery modules, and FMCG retail goods.
Bratislava & Senec Hub
The primary 3PL gateway to Austria, Hungary, and Czechia. Characterized by high land leasing costs, demanding extreme volumetric density such as multi-tier drive-through and radio shuttle configurations.
Trnava & Nitra Cluster
Center for Tier-1 and Tier-2 automotive component staging. Heavy emphasis on strict FIFO drive-through lanes feeding assembly parts directly to synchronized robotic transport lines.
Považie & Žilina Axis
High concentration of precision metalworking, mechanical sub-assemblies, and heavy cold chain operations. Systems require heavy column steel gauge (3.0mm+) to sustain continuous high-cycle operations.
Košice & Prešov Region
Rapidly growing logistics frontier driven by e-mobility investments. Projects require compliance with both Eurocode seismic zones and high-capacity floor loading standards.
Top 10 Drive-Through Racking Factories & Suppliers in Slovakia
An objective assessment of structural engineering capabilities, manufacturing footprint, lead times, and regulatory compliance.
| Supplier Name | Manufacturing Origin | Engineering Standards | Custom Design Flexibility | Slovakia Delivery Lead Time | Primary Market Suitability |
|---|---|---|---|---|---|
| HEDA Shelves | Factory Direct (30,000m² Plant) | CE (2435-CPR-8605159), ISO 9001, EN 15512 | Full Bespoke OEM/ODM | 15–30 Days (Direct Production) | 3PLs, Direct Factory Buyers, Large Logistics Centers |
| Jungheinrich Slovensko | European Central Plants (Germany/EU) | FEM, EN 15512, ISO 9001 | High (Standard Integrated Catalog) | 6–12 Weeks | Integrated Forklift + Racking Turnkey Projects |
| BITO Skladovacia Technika | Germany / Regional EU Distribution | EN 15512, RAL-RG 614 | Moderate (Modular System Focus) | 4–8 Weeks | High-Precision Small Parts & Buffer Storage |
| Dexion (Gonvarri Material Handling) | Germany / Romania / Poland | FEM 10.2.02, EN 15512, ISO 14001 | High (Heavy Engineering Support) | 6–10 Weeks | Automotive & Industrial Manufacturing Facilities |
| Mecalux Slovensko | Spain / Poland Production Hubs | EN 15512, ISO 9001, CE Mark | High (Automated System Focus) | 5–9 Weeks | Standard Pallet Storage & 3PL Logistics Centers |
| SSI Schaefer Slovensko | Germany / Austria / Czechia | DIN EN 15512, FEM Standard | High (Large Scale Automation) | 8–14 Weeks | Automated & Semi-Automated Distribution Hubs |
| Nedcon Racking | Netherlands / Czech Republic | EN 15512, EN 15620 | Very High (Complex Mezzanines & Racks) | 7–12 Weeks | Custom Structural & High-Bay Installations |
| Stow Group (Stow Slovakia) | Belgium / France / Portugal | EN 15512, CE Mark | Moderate (Standard Profile Rolling) | 5–8 Weeks | High-Density Drive-In/Drive-Through Pallet Warehouses |
| Proman s.r.o. Slovakia | Czech Republic / Regional Assembly | ČSN EN 15512, STN Compliance | Moderate (Regional Catalog System) | 4–7 Weeks | SME Warehousing & Commercial Distribution |
| STILL Slovensko | Germany / European Facilities | EN 15512, VDMA Standard | Moderate (Material Handling Tied) | 6–10 Weeks | Fleet-Integrated Forklift & Racking Combinations |
1. HEDA Shelves (Guangzhou Heda Shelves Co., Ltd.) — Factory Direct Advantage
Direct ManufacturerOperating a massive 30,000 m² modern manufacturing plant since 2001, HEDA Shelves bridges the gap between top-tier heavy structural steel engineering and factory-direct cost efficiency. Holding official CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 registration, HEDA designs and manufactures complete Drive-Through and Drive-In racking assemblies fully calculated according to EN 15512 principles. Unlike local brokers, HEDA controls 10 precision roll-forming lines, automated upright punching cells, and continuous pickling/phosphating electrostatic powder-coating systems, producing over 30,000 tonnes monthly with full customization on frame depths, beam heights, and RAL color finishes for European distributors and corporate end-users.
2. Jungheinrich Slovensko s.r.o.
Systems IntegratorHeadquartered in Senec, Jungheinrich Slovensko is widely recognized for delivering complete turn-key intralogistics packages where high-density drive-through systems are closely matched to their proprietary electric reach trucks and narrow-aisle counterbalance forklifts. Their systems offer exemplary build quality and compliance with European FEM regulations, though capital expenditure and long-range customization cycles represent higher budget commitments.
3. BITO Skladovacia Technika s.r.o.
German EngineeringBITO's Slovak subsidiary delivers high-precision modular steel components manufactured primarily in Germany. Their drive-through solutions incorporate specialized beam bracket hooks and patented boltless assembly features. Highly favored in pharmaceutical and high-cleanliness FMCG warehouses in Western Slovakia, BITO excels in standardized modular reliability.
4. Dexion (Gonvarri Material Handling)
European Racking GiantWith extensive production across Europe, Dexion remains a foundational pillar for industrial pallet racking in Slovakia. Their drive-through racking modules feature cold-formed upright profiles engineered to withstand heavy dynamic forces from forklift collisions, frequently deployed across heavy industrial sectors in Nitra and Žilina.
5. Mecalux Slovensko
Global Automation & RacksMecalux maintains a substantial footprint in Slovakia through its Warsaw production nexus. Their drive-through racking solutions are frequently paired with proprietary warehouse management software (Easy WMS), serving large retail distribution networks along the D1 corridor.
6. SSI Schaefer Slovensko
Global Mega-IntegratorSpecializing in complex automated intralogistics, SSI Schaefer provides heavy structural drive-through framing often configured as dynamic buffer staging ahead of automated sorting and pallet conveyor systems. Best suited for high-budget corporate capital expenditure projects.
7. Nedcon Racking
Structural SpecialistsPart of the voestalpine group, Nedcon delivers ultra-heavy structural steel racking profiles engineered in the Netherlands and manufactured in the Czech Republic. Their drive-through frameworks are renowned for high torsional rigidity in extreme-height configurations exceeding 12 meters.
8. Stow Group (Stow Slovakia)
High-Volume Pallet SystemsStow is one of Europe's largest racking producers, supplying high-density drive-through systems across Central Europe. Their standardized upright and pallet rail designs offer broad interoperability, supported by an established dealer and installation network across Slovakia.
9. Proman s.r.o. Slovakia
Regional CEE SupplierOperating extensively across Czechia and Slovakia, Proman supplies dependable industrial storage equipment tailored to small and medium enterprise (SME) facilities. Their drive-through configurations provide quick turnaround times for standard bay heights.
10. STILL Slovensko
MHE & Racking SynergiesSTILL Slovensko mirrors the German standard of pairing counterbalance and reach truck fleets with certified racking frameworks. Their drive-through setups focus on ergonomic transit clearance and integrated collision-avoidance sensor systems.
Engineered Applications in the Slovak Market
How drive-through racking architectures resolve critical capacity and workflow bottlenecks across core Slovak economic sectors.
Automotive JIT / JIS Buffer Staging
Location: Trnava, Nitra, Bratislava industrial zones.
Operational Challenge: Automotive component manufacturers must deliver parts in precise assembly order without line disruptions.
Drive-Through Role: Drive-through lanes act as FIFO accumulators. Parts enter from the manufacturing discharge side and are retrieved on the loading dock side without MHE criss-crossing or reversing maneuvers.
Cold-Chain & Frozen Distribution
Location: Senec Logistics Hub, Nové Zámky, Sládkovičovo.
Operational Challenge: Extreme electrical refrigeration expenses demand maximum pallet density to reduce refrigerated cubic volume.
Drive-Through Role: Eliminates service aisles entirely. By utilizing full building height and depth in -25°C environments, drive-through racks reduce the refrigeration energy consumption per stored pallet position by up to 35%.
Chemical & Industrial Battery Staging
Location: Šaľa, Považská Bystrica, Košice periphery.
Operational Challenge: Strict lot separation and dangerous goods segregation without dead storage space.
Drive-Through Role: Each dedicated bay lane holds a single production batch. Unloading occurs strictly in chronological sequence, preventing dangerous aging of reactive materials and ensuring complete batch traceability.
Structural Engineering & Compliance Benchmarks for Slovak Inspectors
Procuring drive-through racking systems in the Slovak Republic requires rigorous adherence to European and national technical standards. When executing a project, technical directors must ensure that structural calculations comply with:
1. STN EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design): Mandates limit-state design methodology, validating global frame stability under full live load, seismic coefficients, and horizontal placement imperfections.
2. STN EN 15620 (Tolerances, deformations and clearances): Strictly governs beam deflection limits (typically 1/200th of span) and floor slab flatness tolerances (Class 300 / Class 400 under DIN 18202 standards) to ensure forklift masts do not bind against the racking structure at elevated reach levels.
3. STN EN 15635 (Application and maintenance of storage equipment): Governs operational safety protocols, mandatory load notice plaques (Nosnostné tabule), and statutory annual rack inspection routines (Odborná technická kontrola regálov).
Frequently Asked Questions by Slovak Procurement Engineers
Direct technical answers addressing structural feasibility, standards compliance, and logistics delivery to Slovakia.
Can HEDA Shelves drive-through systems accommodate standard European EPAL / EUR pallets?
What engineering documentation is supplied for Slovak fire safety and building permits?
What forklift clearance and truck dimensions are required inside drive-through lanes?
How does sea freight and customs clearance work for delivery to Slovakia?
How does drive-through racking withstand seismic activity in Central Europe?
Can you manufacture OEM custom RAL powder coatings for European distributors?
10-Step Quality Assurance Production Pipeline
How HEDA Shelves executes millimeter-accurate roll-forming, automated CNC punching, and structural integrity control.
01. Raw Steel Inspection
Every coil of Q235B and Q355B high-tensile hot-rolled steel undergoes metallurgical laboratory testing for yield strength, tensile elongation, and chemical composition.
02. Precision CNC Slitting
Automated uncoiling and high-precision laser/rotary shearing slit master coils into exact profile strip widths without edge burrs or micro-fissures.
03. Automated Punching
Continuous multi-station CNC punching presses punch 50mm / 75mm pitch teardrop and butterfly upright slot patterns with ±0.1mm dimensional tolerance.
04. Multi-Stage Cold Forming
18-to-24 station roll-forming lines progressively fold steel strips into proprietary Omega (Ω) and C-profiles without inducing internal residual stress.
05. Automated Robotic Welding
Cantilever arms, baseplates, and portal brackets are welded via robotic MIG/MAG workstations, ensuring complete weld penetration and zero seam porosity.
06. 8-Stage Chemical Pre-Treatment
Components pass through automated immersion tanks for hot degreasing, rust pickling, phosphating, and deionized water rinsing to ensure maximum coating adhesion.
07. Electrostatic Powder Coating
Thermoset epoxy-polyester powder is electrostatically applied and cured in 200°C infrared baking tunnels, producing a durable, impact-resistant 70–90 micron finish.
Plan Your High-Density Slovak Warehouse Project Today
Send us your warehouse floor plan (DWG or PDF), clear ceiling height, pallet specifications, and handling equipment model. Our senior engineering team will calculate your load tables and provide a complimentary 3D/CAD layout proposal within 24 to 48 hours.