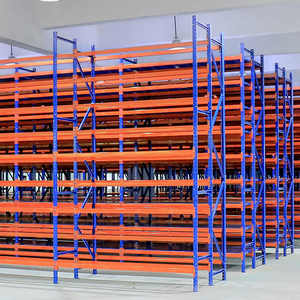
Heavy Duty Warehouse Storage Rack Steel Shelving System
Engineered with multi-ribbed upright columns and high-tensile box beams designed for high-density multi-tier distribution logistics.
Manufactured to rigid ISO 9001:2015 and CE standards, our industrial storage series bridges heavy structural mechanical reliability with modular customization across commercial distribution centers, retail fulfillment, and raw material logistics.
Engineered with multi-ribbed upright columns and high-tensile box beams designed for high-density multi-tier distribution logistics.
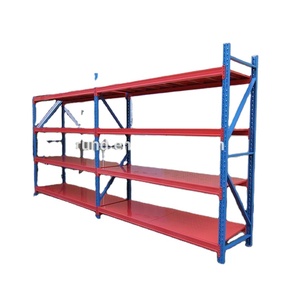
Rated for medium-duty handling up to 300kg per tier, optimized for modular staging, rapid disassembly, and dynamic floor arrangements.
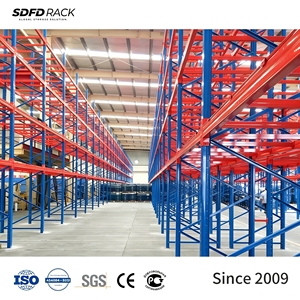
The international standard for 100% pallet accessibility. Offers 50mm/75mm vertical pitch adjustability and high torsional stiffness.
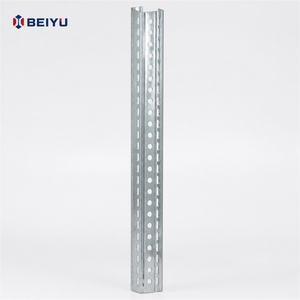
Precision roll-formed cold-rolled structural steel profiles custom-punched for bespoke integrators, system manufacturers, and OEM distributors.
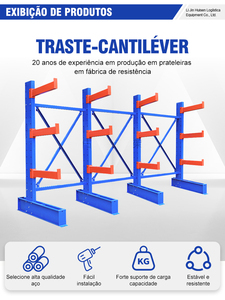
Heavy structural hot-rolled I-beam columns engineered to eliminate front upright obstruction for long stock, pipes, timber, and sheet packs.
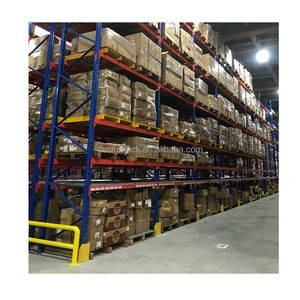
Reduces aisle-to-storage ratio by holding pallets two-deep per bay, increasing footprint volume by 30% compared to pure selective systems.
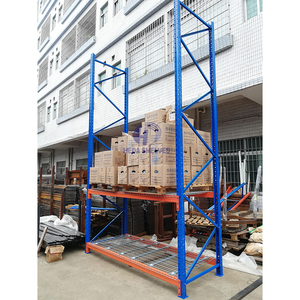
Engineered specifically for high vertical clearances exceeding 12 meters, incorporating narrow aisle floor-guidance and tight deflection control.
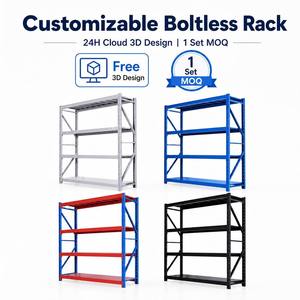
Tool-free quick assembly shelving crafted for bin handling, parcel sorting, spare parts bins, and light-industrial assembly environments.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is an industry-leading manufacturer supplying warehouse racking, shelving, and cantilever systems across 120+ countries. Backed by certified ISO 9001 and CE compliance, we deliver end-to-end technical reliability.
Full CE certification (No. 2435-CPR-8605159) alongside ISO 9001:2015 registration (No. 18624Q00169R0M). Every structural beam and column component is calculated in accordance with EN 15512, EN 15620, and RMI design standards to withstand static, dynamic, and seismic forces.
We operate advanced continuous roll-forming lines capable of handling bespoke open profiles, tear-drop designs, diamond punch patterns, and high-yield Q235B/Q355B cold-rolled steel. We support private-label custom branding, specialized RAL powder coatings, and engineered stamping.
Our in-house team of structural engineers drafts full DWG layouts, volumetric 3D simulations, and load safety tables prior to manufacturing. This eliminates building interference risks, optimizes forklift turning radii, and expedites municipal safety and insurance reviews.
Spectrometric chemical analysis and tensile testing of coil steel.
High-tolerance coil decoiling, leveling, and mechanical longitudinal cutting.
CNC progressive multi-ton stamping of column pitch holes.
Multi-station roller banks form rigid load-bearing profiles.
CO₂ shielded automated continuous welding of beam connectors.
Mechanical scale removal to ensure optimal zinc-phosphate adherence.
Multi-stage immersion cleaning, degreasing, and anti-rust pre-treatment.
Automated powder application cured under 200°C thermal baking lines.
Deflection load validation, film thickness checks, and dimensional audits.
Reinforced steel strapping, protective edge cushioning, and container packing.
Achieving total operational safety demands a rigorous assessment of physical racking parameters. Below is an engineering comparison of primary pallet racking configurations used in modern fulfillment infrastructure.
In structural racking design, catalog nominal loads are merely baselines. Real-world structural reliability hinges on the interaction between Euler buckling limits, connection rigidity (portal action), and the degree of baseplate anchorage. In high-density settings, horizontal seismic forces and operational impact loads from material handling equipment (MHE) dictate that column thickness, diagonal bracing patterns, and floor slab PSI ratings must be calibrated as a singular integrated mechanical assembly.
Under EN 15512 and RMI criteria, beam safety factors must remain at a minimum of 1.5, with maximum permissible deflection under full distributed load restricted to L/200 (where L is clear beam span). For high-bay installations exceeding 10 meters, upright twist and out-of-plumb margins cannot exceed 1/500th of vertical height without compromising automatic carriage tolerances.
| System Architecture | Pallet Accessibility | Space Utilization | Rotational Logic | Primary Mechanical Failure Mode | Optimal Industry Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 100% Direct Immediate | 40% – 50% | FIFO / LIFO Flexible | Front column collision during MHE turning | 3PL hubs, multi-SKU retail, FMCG hubs |
| Double Deep Racking | 50% Immediate (Deep Reach) | 60% – 65% | LIFO Operational | Secondary bay beam deflection overload | Cold storage, wholesale buffer, medium SKU count |
| Radio Shuttle System | Channel Selective | 80% – 85% | FIFO / LIFO Automated | Shuttle rail misalignment & sensor block | Freezer logistics, bulk food processing, chemical drums |
| Cantilever Racks | 100% Linear Frontal | 50% – 60% | Universal | Arm root bending stress concentration | PVC tubing, structural steel beams, timber panels |
| High Bay VNA System | 100% Guided Direct | 70% – 80% | FIFO / LIFO Strict | Floor flatness deviation & mast resonance | High-cube fulfillment, pharma DCs, industrial spare parts |
Procurement directors and supply chain engineers must future-proof storage investments against labor constraints, automated mechanical interfaces, and stringent structural safety regulations.
Procurement is pivoting from static manual racks toward semi-automated radio shuttle lanes and ASRS-integrated high-cube frames. Systems must be engineered with tighter deflection thresholds (≤L/300) to allow autonomous guided vehicle (AGV) laser positioning without mechanical binding.
Global warehouse operators increasingly weigh lifecycle durability over initial steel purchase cost. Thicker gauge column bases, heavy-duty post protectors, and high-impact zinc-powder dual coating lower recurring repair overhead and prevent disastrous rack collapses during standard handling.
Global multi-national warehouse rollouts demand racks meeting both European EN (15512, 15620, 15635) and North American RMI / ANSI MH16.1 codes. Unified certification allows enterprise buyers to replicate uniform distribution center designs across varied regional jurisdictions with full regulatory safety clearance.
With industrial square-meter rental costs accelerating in major logistics hubs, new warehouse construction targets heights of 14 to 30 meters. Procurement focuses heavily on high-bay narrow-aisle (VNA) and rack-clad structural platform systems that transform vertical cubic space into live pallet storage positions.
Comprehensive engineering clarifications to guide supply chain planners, procurement teams, and logistics directors through technical specification and international order fulfillment.
Whether configuring a Greenfield logistics fulfillment center or retrofitting existing warehouse bays to maximize cubic density, our design team is available to review your architectural DWG drawings and provide an optimized, certified layout proposal.
Get Catalog